For efficient grain storage and handling operations, pneumatic material handling systems have become a cornerstone in modern agricultural and food processing facilities. These systems are designed to transport bulk materials like grains, seeds, and other agricultural products within grain silos and related infrastructure. The core of such systems lies in the pneumatic conveying technology, which utilizes air pressure to move materials through a network of pipes and equipment. This approach offers significant advantages over traditional mechanical conveying methods, particularly in terms of flexibility, hygiene, and operational efficiency.
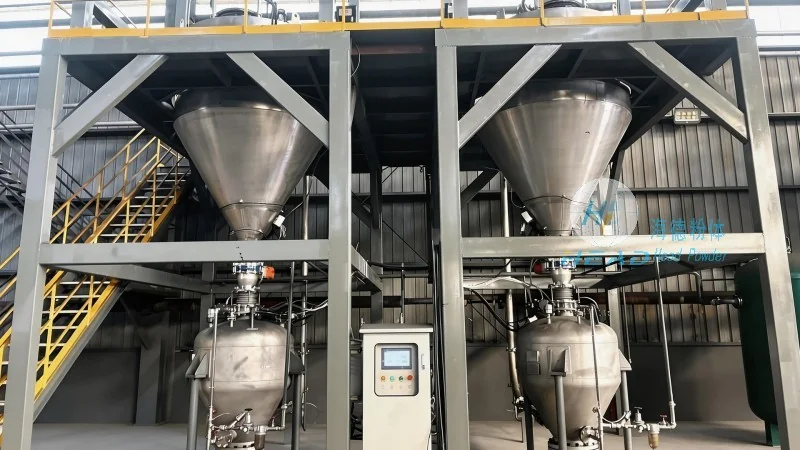
The Working Principle of Pneumatic Material Handling Systems
The fundamental working principle of pneumatic material handling in grain silos involves the use of air to create a flow of material. The process typically starts with the material being loaded into a hopper or feeder. From there, the material is drawn into a pipeline by a vacuum or pressure created by a fan or blower. The air and material mixture travels through the pipeline, often with the help of special components like bends, elbows, and filters to ensure smooth and efficient transport. At the destination point, the material is separated from the air, usually through a cyclone separator or a filter, and collected in a storage bin or processing unit. The air, now clean, is either recirculated or discharged, completing the cycle. This continuous process allows for the seamless transfer of large volumes of grain with minimal human intervention.
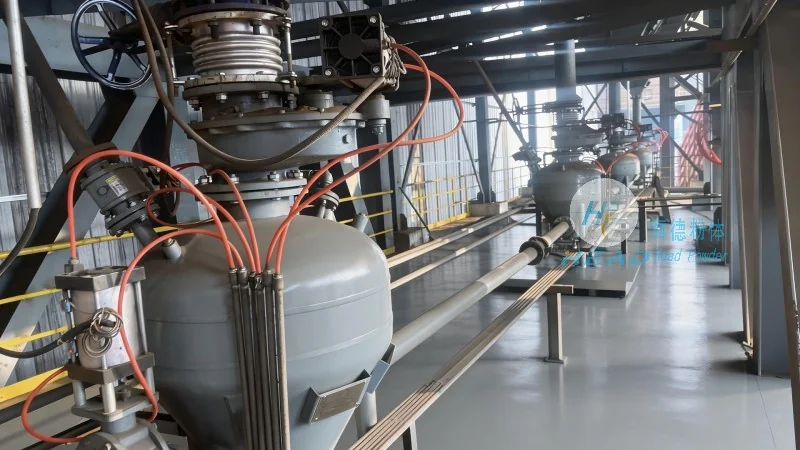
Key Characteristics and Advantages of Pneumatic Material Handling in Grain Silos
Several distinct characteristics define the effectiveness of pneumatic material handling systems in grain storage applications. Firstly, they offer high flexibility in terms of layout and routing. Unlike fixed mechanical conveyors, pneumatic systems can be easily reconfigured to adapt to changes in storage or processing needs, making them ideal for dynamic operations. Secondly, these systems excel in maintaining hygiene standards, as they operate in enclosed pipelines, preventing contamination from external sources and ensuring the purity of the grain. This is particularly critical in food processing industries where product quality and safety are paramount. Thirdly, pneumatic conveying is known for its ability to handle a wide range of material types and sizes, from fine powders to larger grain particles, with minimal degradation or loss. Additionally, the systems are generally low-maintenance, with fewer moving parts compared to mechanical conveyors, leading to reduced operational costs and downtime. The energy efficiency of modern pneumatic systems also contributes to their appeal, as they can optimize air usage and minimize waste.
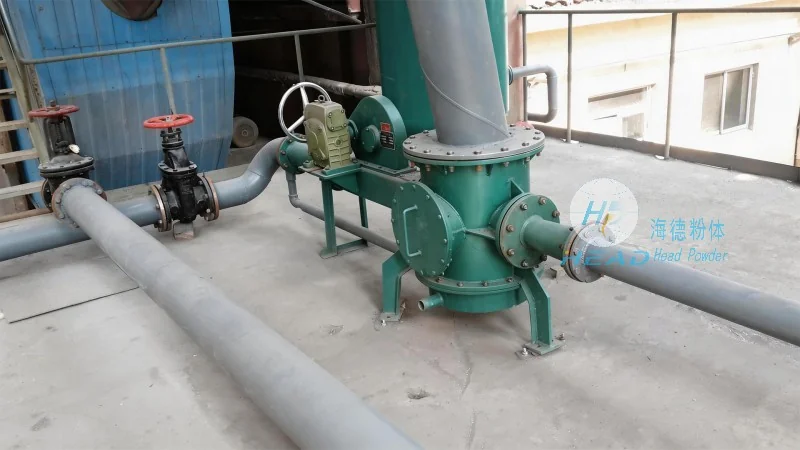
Applications and Integration in Modern Grain Storage Facilities
Pneumatic material handling systems are widely integrated into various aspects of grain storage and processing. They are commonly used for loading and unloading grain from trucks and railcars, transferring grain between silos or storage bins, and feeding processing equipment like mills and cleaners. The ability to transport materials vertically and horizontally with equal efficiency makes these systems versatile for complex storage layouts. Moreover, in combination with automation and control systems, pneumatic conveyors can be integrated into fully automated grain handling lines, enhancing overall operational efficiency and reducing labor requirements. The adaptability of these systems also allows them to be used in different stages of the grain handling process, from initial reception to final packaging, ensuring a smooth and continuous workflow.
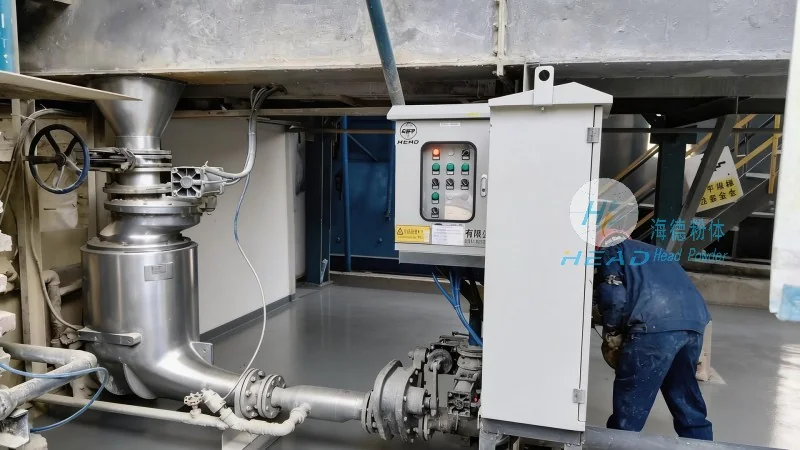
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
As a leading provider of engineering solutions for material handling in the agricultural sector, Shandong HeadPowder Engineering Co., Ltd. specializes in designing, manufacturing, and implementing advanced pneumatic conveying systems tailored to the needs of grain storage facilities. With a focus on innovation and quality, the company has established itself as a trusted partner in the industry, delivering solutions that enhance operational efficiency and product quality. HeadPowder's expertise lies in customizing systems to meet specific client requirements, ensuring that each installation is optimized for the unique characteristics of the grain being handled and the operational environment. The company's commitment to using high-quality materials and advanced technology in its products ensures durability and reliability, which are crucial for long-term performance in demanding agricultural applications. Based in Shandong, China, HeadPowder leverages its local presence and industry knowledge to provide comprehensive support to clients, from initial consultation to after-sales service.




