Working Principle and Features of Powder Pneumatic Conveying Equipment for Dust Collection Stations
Release time:2026-09-18 03:01:24
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Zhang manager
Efficient and reliable material handling is a critical aspect of industrial operations, especially within dust collection systems where the transport of powders and particulate matter is essential. The powder pneumatic conveying equipment specifically designed for dust collection stations serves as a vital component in maintaining air quality and ensuring smooth operational processes. This equipment is engineered to move powders and fine particles from one location to another within a dust collection system, offering a solution that minimizes contamination and optimizes overall system efficiency.
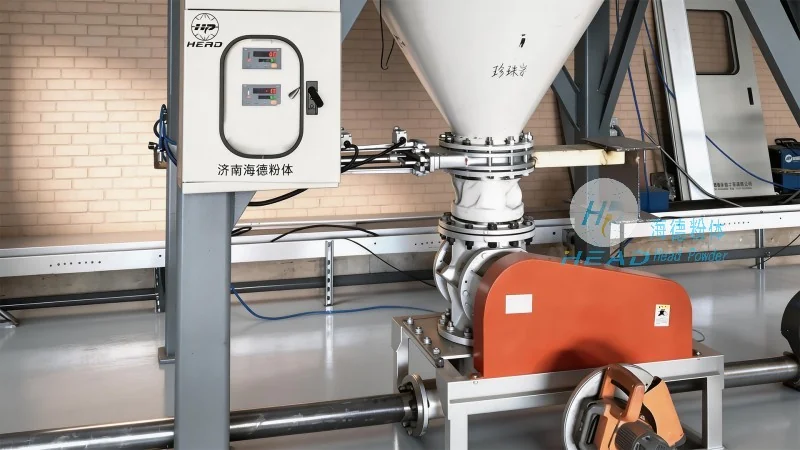
Working Principle of Powder Pneumatic Conveying Equipment
The fundamental operation of powder pneumatic conveying equipment revolves around the use of air or gas to transport bulk materials. The process typically begins with a hopper or feeder that feeds the powder into a pipeline. A blower or compressor then generates the necessary airflow, which propels the powder particles through the pipeline. The equipment may employ either positive pressure (where air is forced into the system) or negative pressure (where air is drawn out), depending on the specific application and system design. The air-powder mixture travels through the pipeline, and the powder is subsequently separated from the air at the discharge point, often utilizing a cyclone separator or a filter. This separation process ensures that the powder is delivered to its intended destination while the air is either recirculated or released as clean air, maintaining the integrity of the material and the cleanliness of the system.
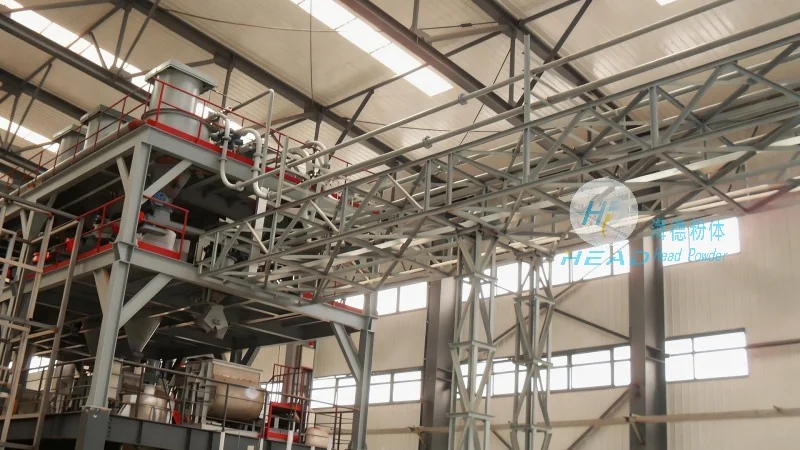
Key Features of the Equipment
HeadPowder Engineering Co., Ltd. offers powder pneumatic conveying equipment for dust collection stations that is distinguished by several key features. One primary feature is its ability to handle a wide variety of powder types, including fine powders, granules, and even sticky or cohesive materials. The equipment is constructed with robust materials to withstand the abrasive nature of powders and the corrosive effects of certain chemicals, ensuring long-term durability and reliability. Another significant feature is the adjustable airflow control, which allows operators to optimize the conveying rate based on the material's properties and system requirements. The system also incorporates essential safety features such as pressure relief valves and overheat protection to prevent accidents and equipment damage. Additionally, the equipment is equipped with easy-to-clean components, facilitating maintenance and reducing downtime. The compact design of the system makes it suitable for installation in confined spaces, a common requirement in dust collection stations, ensuring efficient use of available space.
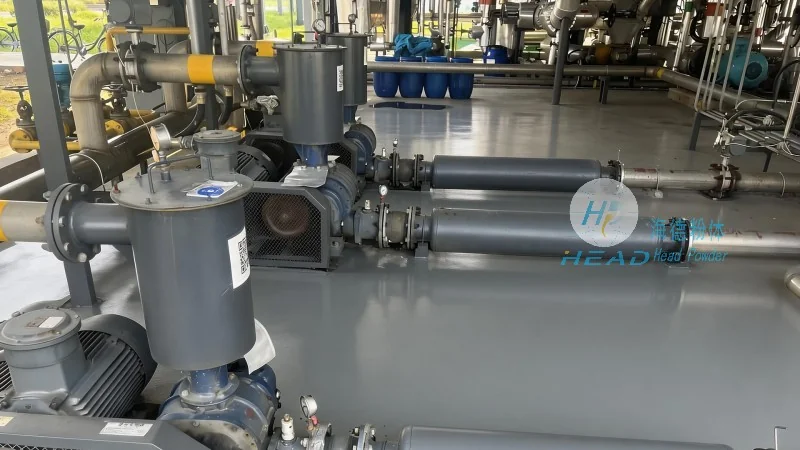
Benefits and Applications
The integration of powder pneumatic conveying equipment in dust collection stations provides numerous benefits. Firstly, it eliminates the need for manual handling of powders, thereby reducing the risk of dust exposure and enhancing workplace safety. Secondly, the closed system design minimizes material loss and contamination, which is particularly crucial in industries like pharmaceuticals, food processing, and chemical manufacturing where product purity is paramount. The equipment also enhances process efficiency by providing a continuous and consistent flow of material, leading to increased production rates and reduced operational costs. In dust collection systems, the equipment ensures that powders are efficiently transported from the collection point to storage or processing areas, maintaining the integrity of the material and the cleanliness of the air system. This contributes to overall operational excellence and compliance with environmental regulations.




