Bean material handling equipment plays a crucial role in the agricultural and food processing industries, particularly when dealing with legumes like beans. These specialized machines are engineered to efficiently transport, sort, and process bean materials from one stage of production to another. Understanding the functionality and design principles behind such equipment is essential for optimizing operational efficiency and maintaining product quality.
What Are Bean Material Handling Equipment?
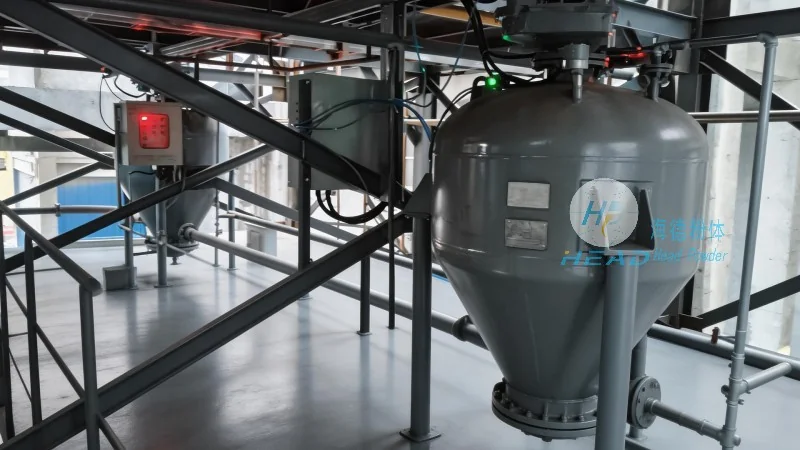
Bean material handling equipment encompasses a range of machinery designed to manage the movement of bean crops or processed bean products. This includes devices like conveyors, elevators, and sorting systems that are tailored to handle the unique characteristics of beans—such as their size, shape, and texture. The primary goal of these systems is to streamline the workflow in bean processing facilities, from harvesting and cleaning to packaging and distribution.
The Design Principles of Bean Material Handling Equipment
The design of bean material handling equipment is guided by several key principles aimed at maximizing efficiency, durability, and adaptability. First, the equipment must be constructed to withstand the physical demands of handling bean materials, which may include moisture, dust, and varying particle sizes. Materials like stainless steel and corrosion-resistant alloys are commonly used to ensure longevity and hygiene, especially in food processing applications. Second, the design emphasizes gentle handling to preserve the integrity of the beans, minimizing damage during transport. This is achieved through features like adjustable speed controls, soft-start mechanisms, and specialized belt or chute materials that reduce friction and abrasion. Third, the equipment is engineered for easy maintenance and cleaning, which is critical in food processing environments to meet sanitary standards. Modular components and easy-to-access parts allow for quick repairs and sanitation, reducing downtime and operational costs.
Key Components and Their Functions
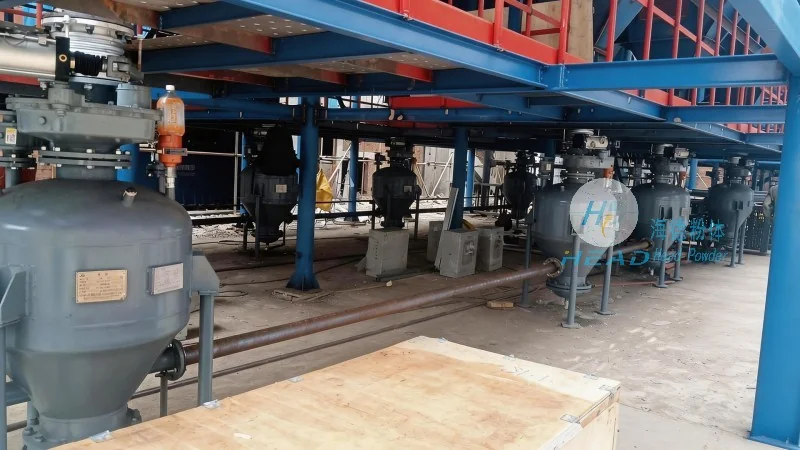
Bean material handling equipment typically consists of several interconnected components, each serving a specific function in the material flow. The main components include: conveyors (such as belt conveyors or screw conveyors) for horizontal or vertical transport, elevators for lifting beans to higher levels, and sorting mechanisms for separating beans based on size, weight, or quality. Additionally, cleaning and conditioning systems may be integrated to remove impurities like stones, dust, or foreign objects before further processing. These components work in tandem to create a seamless material handling process, ensuring that beans are moved safely and efficiently from one stage to the next.
Applications in Bean Processing
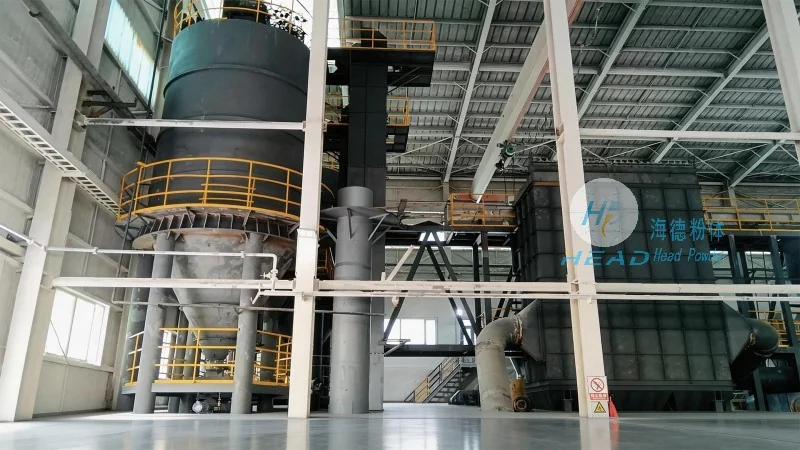
Bean material handling equipment is widely used in various stages of bean processing, from raw bean reception to final product packaging. In the initial stages, equipment like vibrating screens and air classifiers are used to clean and sort raw beans, removing debris and unwanted materials. During the processing phase, conveyors transport beans to processing lines, where they may undergo peeling, shelling, or roasting. After processing, sorting machines separate beans by grade or quality, allowing for proper packaging and distribution. The equipment also supports quality control by enabling the inspection of beans for defects or contamination, ensuring that only high-quality products reach the market.
Advantages of Using Bean Material Handling Equipment
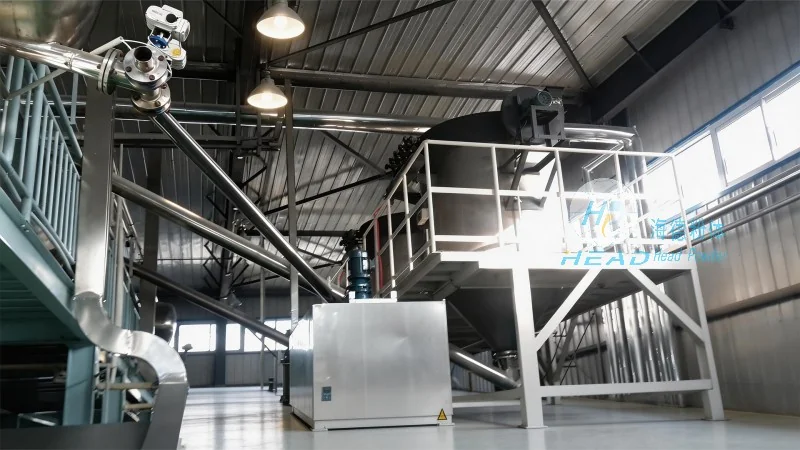
Implementing bean material handling equipment offers several advantages for businesses in the bean processing industry. Firstly, it significantly improves operational efficiency by automating the material transport process, reducing the need for manual labor and minimizing human error. This leads to faster processing times and increased throughput, which is crucial for meeting market demands. Secondly, the equipment enhances product quality by ensuring gentle handling and consistent processing, reducing the risk of damage or contamination. This results in higher-quality beans that are more appealing to consumers and command better prices. Thirdly, the design of modern bean material handling equipment focuses on energy efficiency, with features like variable speed drives that reduce power consumption. This not only lowers operational costs but also aligns with sustainability goals. Finally, the equipment is designed for scalability, allowing businesses to expand their operations without significant changes to the material handling system.
Conclusion
Bean material handling equipment is a vital component of modern bean processing operations, combining functionality, durability, and efficiency to meet the demands of the industry. By understanding the design principles and applications of these systems, businesses can optimize their production processes, improve product quality, and enhance overall operational performance. As a leader in engineering solutions for material handling, Shandong HeadPowder Engineering Co., Ltd. specializes in providing customized equipment tailored to the specific needs of bean processing facilities, ensuring that businesses can achieve their operational goals with reliable and efficient equipment.




