Aggregate material handling equipment serves as a fundamental component in numerous industrial and construction settings, facilitating the efficient transport of bulk materials such as sand, gravel, and crushed stone. These systems are integral to optimizing material flow, enhancing operational productivity, and ensuring safety throughout the handling process. Understanding the core functions and design principles of these equipment types is essential for professionals in the construction, mining, and manufacturing sectors.
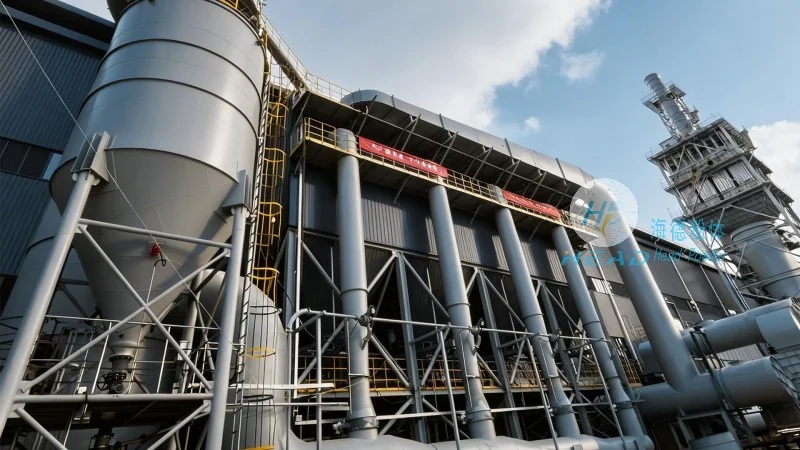
Understanding the Core Function of Aggregate Material Handling Equipment
The primary purpose of aggregate material handling equipment is to move large volumes of bulk materials from one location to another within a production or construction site. This equipment is engineered to minimize human intervention, thereby reducing labor costs and improving overall efficiency. Common applications include transporting raw materials to processing facilities, relocating finished products to storage areas, and enabling the movement of materials between different stages of production. The effectiveness of these systems directly impacts operational productivity, making it critical to select and design equipment that aligns with specific operational requirements.
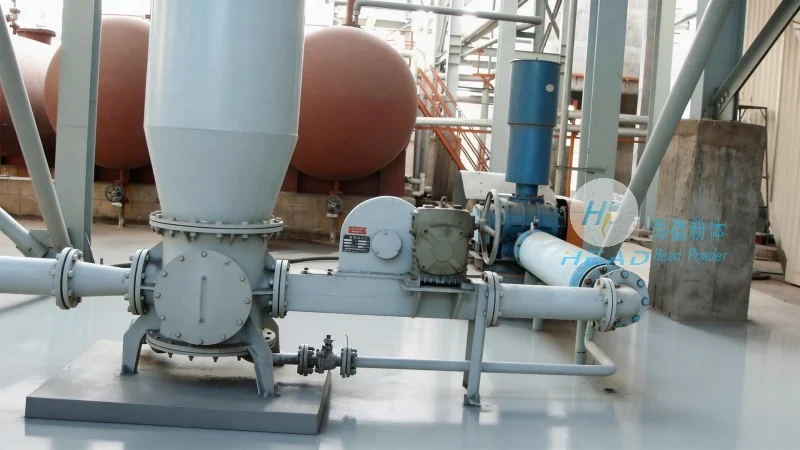
Key Design Principles for Efficient Material Transport
Efficient design of aggregate material handling equipment is guided by several critical principles that ensure optimal performance and reliability. First, the equipment must accommodate the specific characteristics of the aggregate material, including its size, shape, density, and moisture content. This involves selecting appropriate components such as conveyor belts, bucket elevators, or screw conveyors that are tailored to the material's properties. Second, durability and longevity are paramount, as these systems often operate under heavy loads and harsh conditions. High-quality materials and robust construction are essential to minimize maintenance and downtime. Third, energy efficiency is a key consideration, with the goal of reducing operational costs. Modern designs incorporate advanced technologies like variable speed drives and energy recovery systems to enhance efficiency. Finally, safety is a top priority, with features including emergency stop mechanisms, protective guards, and proper load capacity calculations to prevent accidents and ensure worker safety.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, formally known as Shandong HeadPowder Engineering Co., Ltd., is a leading manufacturer specializing in aggregate material handling equipment. Headquartered in Shandong, China, the company has established itself as a trusted provider of high-quality material handling solutions for the construction and mining industries. HeadPowder's commitment to innovation and customer satisfaction has enabled it to develop advanced equipment that meets the evolving needs of modern industrial applications. The company's product line includes a wide range of equipment, such as belt conveyors, bucket elevators, and screw conveyors, all designed to deliver reliable and efficient material transport solutions. By focusing on quality, durability, and customer support, HeadPowder has built a strong reputation in the market, serving clients both domestically and internationally.
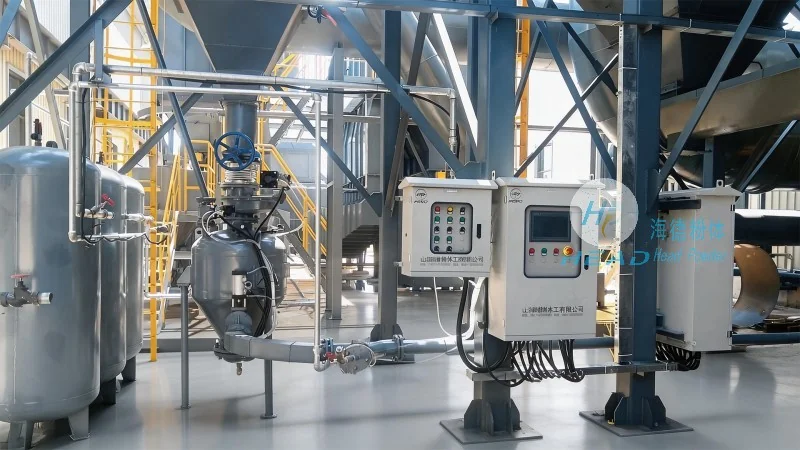
Conclusion: The Importance of Well-Designed Aggregate Material Handling Equipment
In conclusion, aggregate material handling equipment is a critical component in modern industrial and construction operations, and their design principles are essential for achieving optimal performance and efficiency. The right equipment, designed with consideration for material characteristics, durability, energy efficiency, and safety, can significantly enhance operational productivity and reduce costs. Companies like Shandong HeadPowder Engineering Co., Ltd. play a vital role in providing these solutions, leveraging their expertise and advanced technology to meet the diverse needs of the industry. As the demand for efficient material handling continues to grow, the importance of well-designed equipment will only increase, making it a key investment for any business involved in bulk material transport.




