For businesses in the food processing industry, particularly those involved in the production of fermented grain products like rice wine, the efficient and hygienic handling of raw materials is critical to maintaining product quality and operational efficiency. The air-pneumatic conveying system represents a sophisticated solution designed to address these challenges, offering a reliable method for transporting bulk materials such as fermented grain from storage to processing areas.
Introduction to the Air-Pneumatic Conveying System
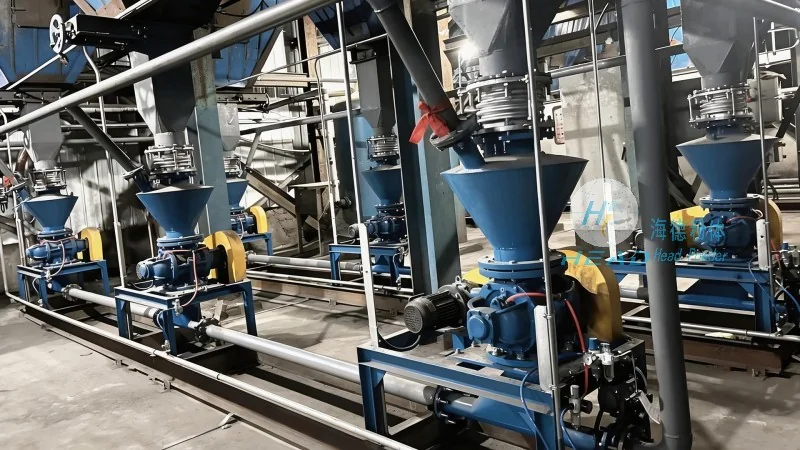
The air-pneumatic conveying system, also known as pneumatic conveying, is a technology that uses compressed air to move dry or semi-dry bulk materials through a pipeline. This method is particularly advantageous for handling materials like fermented grain, which require careful handling to preserve their texture and microbial integrity. Unlike traditional mechanical conveying systems, pneumatic conveying minimizes material degradation, reduces contamination risks, and enhances overall process control.
Key Features and Advantages of the System
One of the primary advantages of the air-pneumatic conveying system is its ability to maintain a closed environment, which is essential for food safety compliance. By eliminating direct contact with external contaminants, the system ensures that the fermented grain remains in pristine condition throughout the conveying process. Additionally, the system offers flexibility in terms of layout and integration with existing production lines, allowing for seamless adaptation to various facility configurations.
Another significant benefit is the energy efficiency of pneumatic conveying. Compared to traditional methods like bucket elevators or belt conveyors, the air-pneumatic system typically consumes less power while achieving higher material throughput. This not only reduces operational costs but also contributes to a more sustainable manufacturing process. The system also provides consistent material flow rates, which helps in maintaining uniform product quality and reducing waste.
Technical Specifications and Components
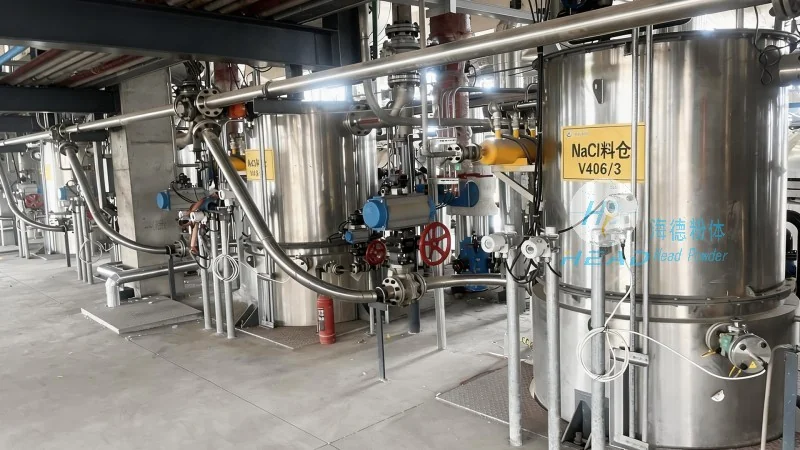
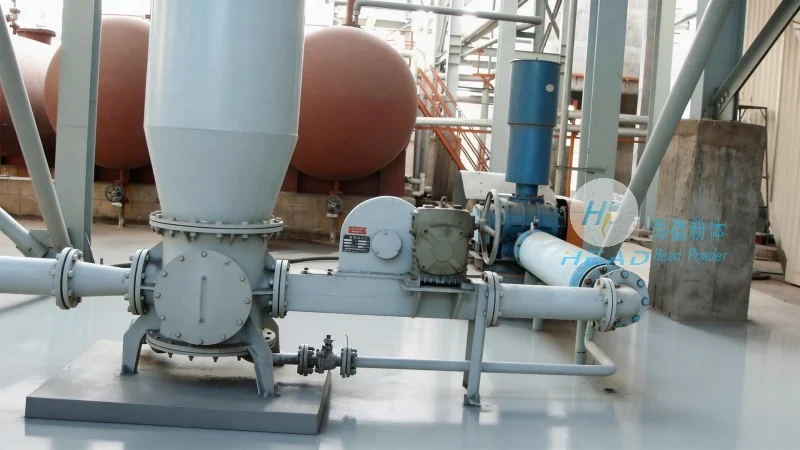
The air-pneumatic conveying system for fermented grain typically consists of several key components, including a hopper for material storage, a feeder to control the flow of material into the pipeline, a conveying line with appropriate fittings and valves, and a receiver to deposit the material at the destination. The system may also include a dust collection system to manage any airborne particles and ensure a clean working environment. The choice of components, such as the type of air compressor and the material of construction for the pipeline, is tailored to the specific characteristics of the fermented grain, ensuring optimal performance and durability.
Application in Fermented Grain Production
In the context of rice wine production, the air-pneumatic conveying system is widely used to transport fermented grain from the fermentation tanks to the distillation or drying stages. This process is crucial as it ensures that the grain is moved without breaking down the delicate microbial cultures that contribute to the flavor and aroma of the final product. The system's gentle handling capabilities prevent the agglomeration of particles and maintain the granular structure of the fermented grain, which is vital for subsequent processing steps.
The system also supports the integration of multiple production lines, allowing for the simultaneous transfer of different batches of fermented grain. This capability enhances production flexibility and reduces downtime during material changes. Furthermore, the system's ability to handle varying material densities and moisture levels makes it suitable for a range of fermented grain products, from traditional rice wine to other fermented grain-based beverages.
Benefits for Food Processing Facilities
Implementing an air-pneumatic conveying system for fermented grain offers numerous benefits for food processing facilities. Firstly, it improves operational efficiency by reducing the time and labor required for material handling. The automated nature of the system minimizes human intervention, leading to consistent and reliable material transfer. Secondly, it enhances product quality by maintaining the integrity of the fermented grain, which directly impacts the final taste and nutritional value of the end product.
Thirdly, the system contributes to cost savings through reduced energy consumption and lower maintenance requirements. The closed system design also reduces the risk of cross-contamination, which is a critical factor in food safety regulations. This helps facilities maintain compliance with industry standards and avoid potential penalties or product recalls.
Customization and Integration Services
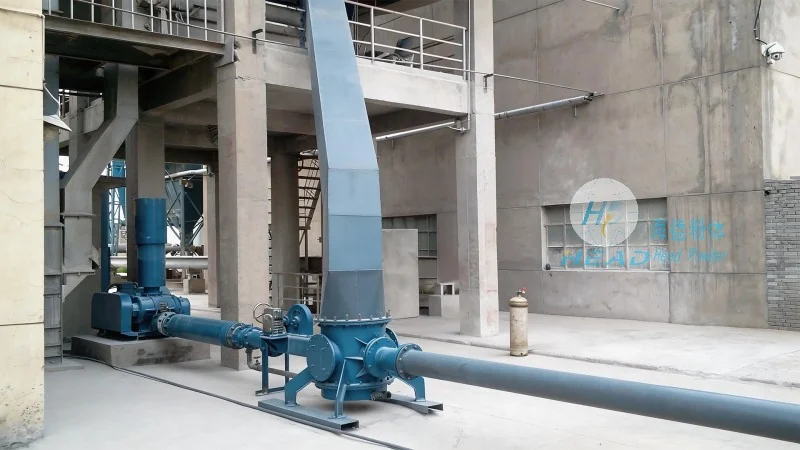
Shandong HeadPowder Engineering Co., Ltd., a leading provider of engineering solutions for the food processing industry, offers customized air-pneumatic conveying systems tailored to the specific needs of each client. With a team of experienced engineers and technicians, the company ensures that the system is designed to meet the unique requirements of fermented grain production, including material characteristics, production capacity, and facility layout.
HeadPowder provides comprehensive integration services, from initial system design and installation to ongoing maintenance and support. The company's expertise in pneumatic conveying technology allows for the development of solutions that are both efficient and cost-effective, ensuring that clients achieve optimal performance and return on investment. By partnering with HeadPowder, food processing facilities can enhance their operational capabilities and maintain a competitive edge in the market.
Conclusion
The air-pneumatic conveying system for fermented grain is a sophisticated and effective solution for the efficient handling of bulk materials in food processing. By leveraging compressed air to transport materials through a closed pipeline, the system offers numerous advantages, including improved product quality, enhanced operational efficiency, and reduced costs. With its ability to maintain a hygienic environment and adapt to various production needs, the system is an essential component for modern fermented grain production facilities. As a trusted provider of engineering solutions, Shandong HeadPowder Engineering Co., Ltd. continues to lead the way in delivering high-quality, customized conveying systems that meet the evolving demands of the food industry.




