For farmers and agricultural processing enterprises, the efficient handling of millet materials is crucial to the smooth operation of production processes. The millet material handling system equipment, developed by Shandong HeadPowder Engineering Co., Ltd. (hereinafter referred to as HeadPowder), is designed to meet the diverse needs of millet material transportation, storage, and processing. This article will delve into the principles of the equipment and its working scene characteristics, providing a comprehensive understanding of its application and advantages.
Principle of Millet Material Handling System Equipment
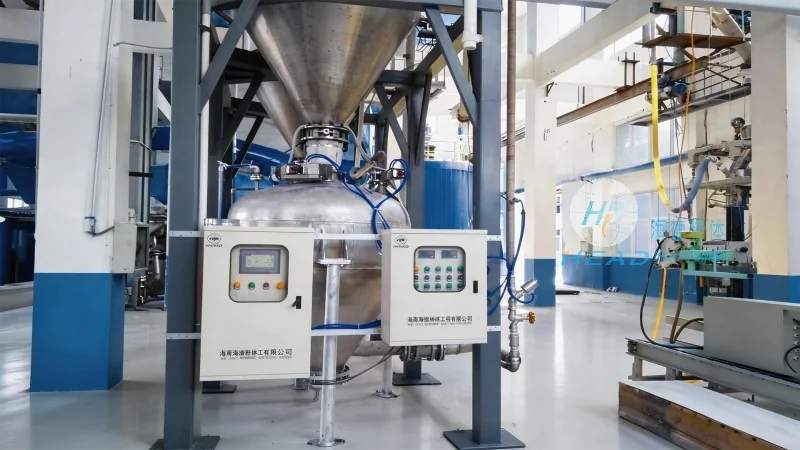
The millet material handling system equipment typically consists of components such as feeders, conveyors, storage bins, and control systems. The working principle is based on mechanical force to achieve the movement of millet from the collection point to the processing or storage point. Feeders are used to uniformly feed millet into the conveyor system, which can be belt conveyors, screw conveyors, or pneumatic conveyors, depending on the material characteristics and application requirements. Belt conveyors are suitable for horizontal or gentle incline transportation, offering high load capacity and stable operation. Screw conveyors are ideal for vertical or inclined transportation, with the ability to mix and lift materials. Pneumatic conveyors, or air slides, are used for long-distance or enclosed transportation, providing dust-free and low-noise operation. The conveyor system transfers the millet through a series of mechanisms, ensuring stable and continuous material flow. Storage bins are used for temporary storage, allowing for buffer management during peak production periods. The control system integrates sensors and automation technology to monitor the material flow, adjust the conveyor speed, and ensure safe and efficient operation. This integrated design enables the equipment to handle millet with high efficiency and low energy consumption, while minimizing material damage and loss.
Working Scene Characteristics of Millet Material Handling System Equipment
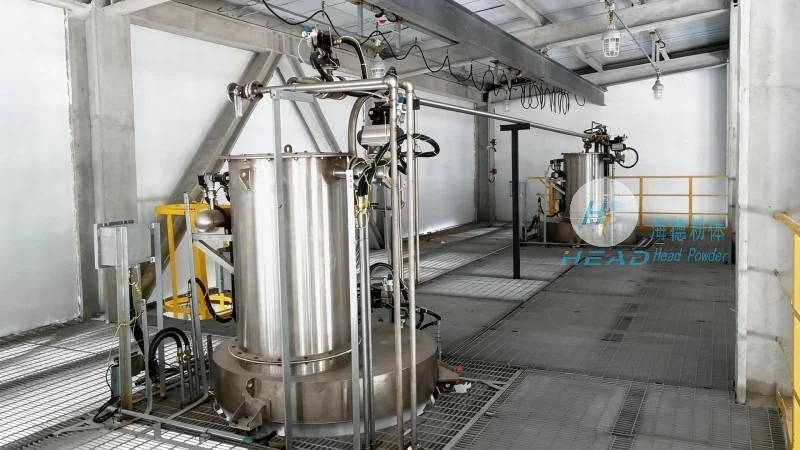
The millet material handling system equipment is widely used in various working scenes, each with its unique characteristics and requirements. In the millet harvesting and collection stage, the equipment is used to transport harvested millet from the field to the storage area, ensuring timely and safe material transfer. For example, in a large-scale farm, the equipment can be connected to the combine harvester to directly receive the millet, reducing the need for manual handling and minimizing material loss. During the processing stage, such as cleaning, grading, and drying, the equipment is used to move millet between different processing units, maintaining the continuity of the production line. The conveyor system can be adjusted to match the processing speed, ensuring that each unit receives a consistent flow of material. In the storage stage, the equipment is used to transfer millet from the processing line to the storage bins, optimizing storage space and reducing material loss due to spoilage. The working scene characteristics also include the need for adaptability to different millet varieties, such as different sizes and moisture contents, and the ability to handle large volumes of material with minimal labor. The equipment is designed to be flexible and scalable, allowing it to be integrated into existing production lines or used as a standalone system, catering to the diverse needs of agricultural enterprises.
Application Advantages of Millet Material Handling System Equipment by HeadPowder
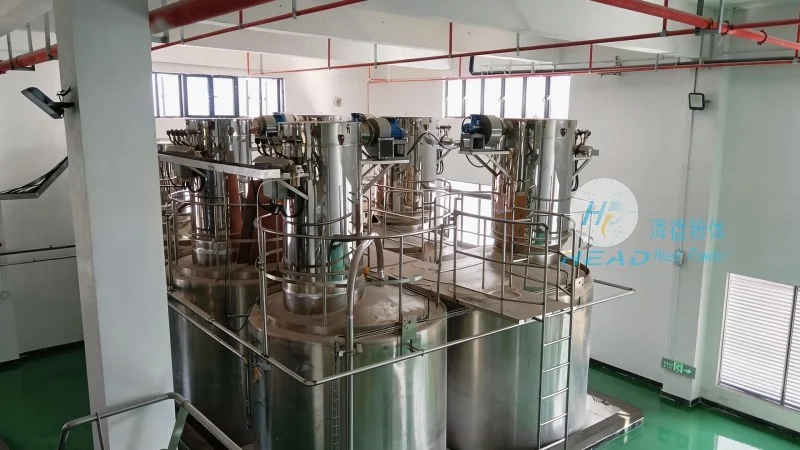
HeadPowder, as a professional manufacturer of millet material handling system equipment, has accumulated rich experience in the design and production of such systems. The company's products are characterized by high efficiency, low maintenance costs, and strong adaptability. The equipment is manufactured with high-quality materials, such as stainless steel and corrosion-resistant alloys, ensuring durability and resistance to the corrosive environment of millet processing. The advanced manufacturing processes, including precision machining and automated assembly, guarantee the equipment's high performance and reliability. The control system is equipped with user-friendly interfaces and remote monitoring capabilities, allowing operators to easily manage the equipment and monitor its status in real-time. The company also provides customized solutions based on the specific needs of customers, including different conveyor types, storage bin capacities, and control system configurations. By using HeadPowder's millet material handling system equipment, agricultural enterprises can improve production efficiency by up to 30%, reduce labor costs by minimizing manual handling, and enhance product quality by reducing material damage and loss. These advantages make HeadPowder's equipment a preferred choice for millet processing enterprises, helping them to increase their competitiveness in the market.




