For industries dealing with bulk powders, efficient and reliable material handling is crucial. The intelligent bulk bag unloading and powder conveying system, developed by Shandong HeadPowder Engineering Co., Ltd., represents a significant advancement in this field. This system integrates advanced technology to streamline the process of handling bulk bagged materials, ensuring high efficiency, safety, and precision in various industrial applications. By automating the traditionally labor-intensive and time-consuming tasks of bulk bag handling, the system enhances productivity while reducing operational costs and minimizing the risk of material loss or contamination.
Principle of the Intelligent Bulk Bag Unloading Powder Conveying System
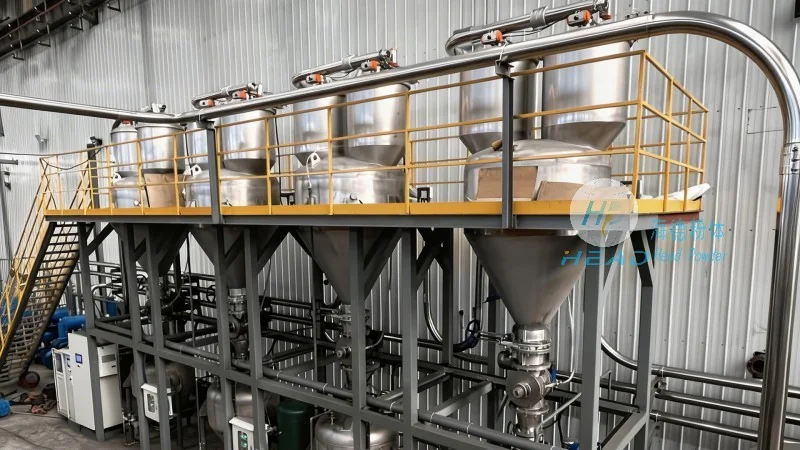
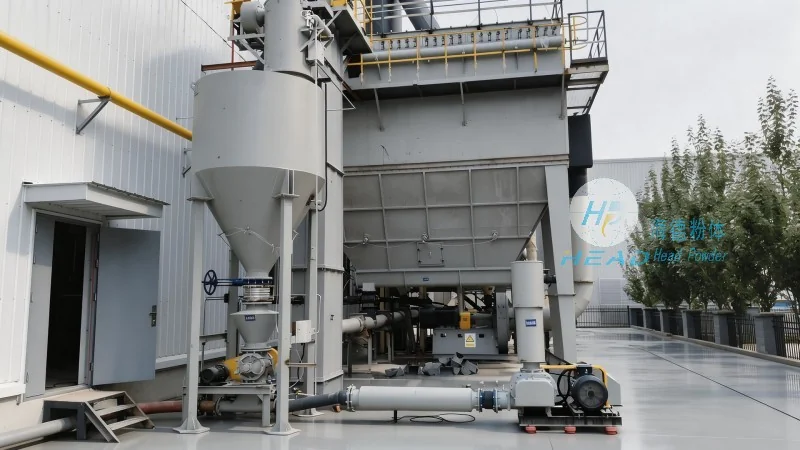
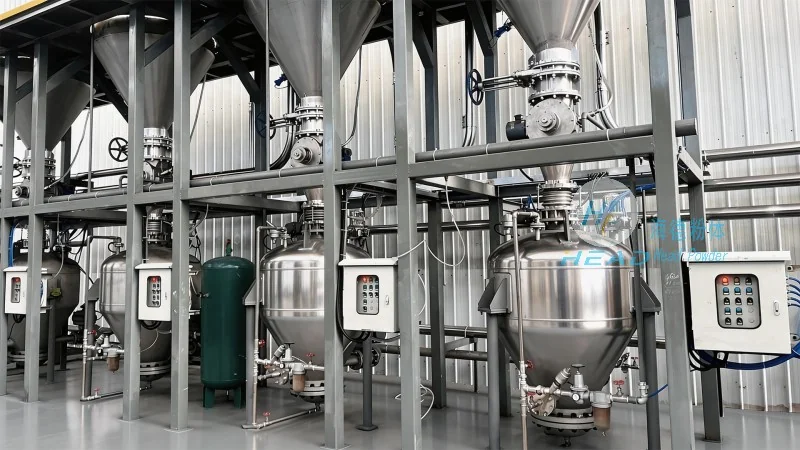
The core of the system lies in its intelligent control and automation. It typically comprises several key components, including bulk bag lifting mechanisms, automatic opening devices, and powder conveying units. The process begins with the placement of a bulk bag onto a designated platform. The system then uses mechanical or pneumatic actuators to lift the bag, followed by automated opening to release the powder. The powder is then transferred through a conveyor system, often with dust collection and filtration to maintain air quality. Sensors and control systems monitor the entire process, ensuring that the flow rate, pressure, and other parameters remain within optimal ranges. This integration of mechanical, electrical, and pneumatic components allows for a seamless and continuous operation, minimizing manual intervention and reducing the risk of material loss or contamination. The system's design emphasizes energy efficiency and low maintenance, making it a cost-effective solution for long-term use.
Working Scene Characteristics and Application Advantages
The intelligent bulk bag unloading and powder conveying system is designed to meet the diverse needs of different industrial sectors. Its adaptability makes it suitable for applications in pharmaceuticals, food processing, chemical manufacturing, and other industries where handling bulk powders is essential. The system's key characteristics include high efficiency, as it can process multiple bulk bags per hour, significantly reducing downtime compared to traditional manual methods. Additionally, it offers enhanced safety features, such as enclosed conveying systems and dust suppression mechanisms, which protect both operators and the environment. The system's modular design allows for customization based on the specific requirements of the user, including different bag sizes, powder types, and conveying distances. This flexibility ensures that the system can be integrated into existing production lines without major modifications, providing a cost-effective solution for material handling needs. In pharmaceutical applications, for example, the system's compliance with GMP (Good Manufacturing Practice) standards ensures that the handling process meets regulatory requirements, maintaining product quality and safety. Similarly, in food processing industries, the system's hygienic design and easy cleaning features help maintain high standards of sanitation, which is critical for product quality and consumer safety.




