HeadPowder, a leading provider in the field of industrial material handling solutions, specializes in the design, manufacturing, and implementation of advanced dust-free and airtight material conveying systems. These systems are engineered to ensure the safe, efficient, and contamination-free transport of various materials across diverse industrial applications. The following article delves into the core principles behind such systems and highlights the key working scene characteristics that define their operational effectiveness.
Understanding the Core Principles of Dust-Free and Airtight Conveying Systems
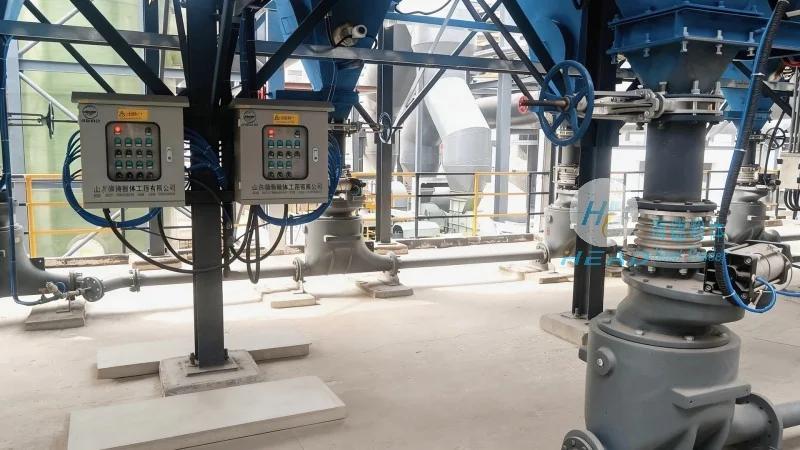
The fundamental principle of dust-free and airtight material conveying systems is to create a sealed environment that prevents the release of particulate matter or contaminants into the surrounding air. This is achieved through a combination of robust mechanical components, advanced sealing technologies, and intelligent control mechanisms. The system typically operates by enclosing the material within a sealed tube or channel, ensuring that all material movement is contained and that no dust or particles escape into the ambient environment. Key components include high-quality conveyor belts or chains, precision-driven drive systems, and specialized sealing elements that maintain the integrity of the system's enclosure. The design emphasizes durability, low maintenance, and high efficiency, making it suitable for demanding industrial settings.
Key Working Scene Characteristics and Applications
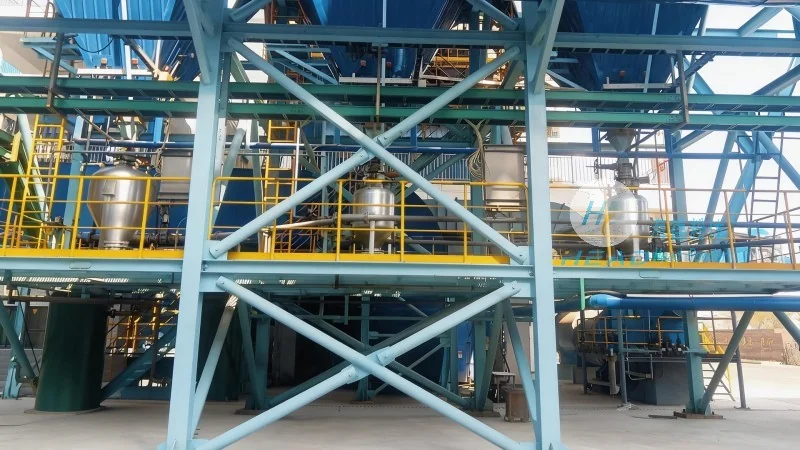
Dust-free and airtight material conveying systems are widely employed in industries where material purity and environmental safety are paramount. Common working scene characteristics include high-precision manufacturing environments, pharmaceutical production facilities, food processing plants, and research laboratories. In these settings, the system's ability to maintain a sterile and contamination-free environment is critical. For instance, in pharmaceutical manufacturing, the system ensures that raw materials are transported without introducing any foreign particles that could compromise product quality or safety. Similarly, in food processing, the sealed design prevents cross-contamination and maintains hygiene standards. The systems are also utilized in industries dealing with hazardous materials, where the risk of dust explosions or inhalation of harmful particles is a major concern. The working scenes often involve continuous operation, high material throughput, and strict adherence to regulatory standards, all of which the system's design addresses effectively.
Operational Advantages and Technical Specifications
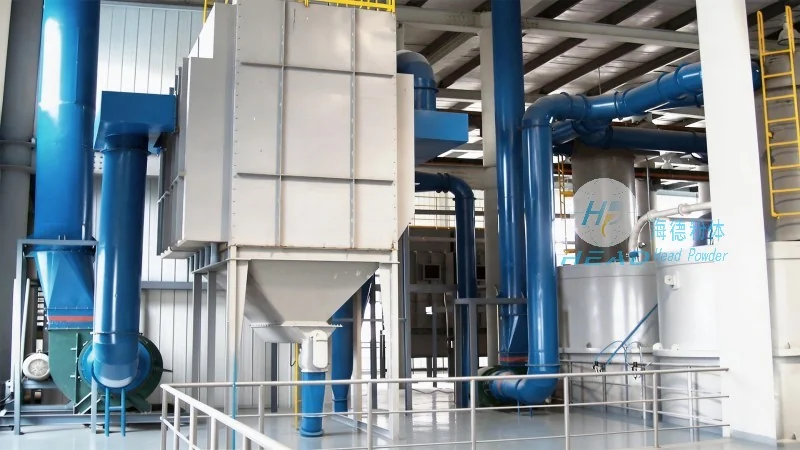
HeadPowder's dust-free and airtight material conveying systems offer several operational advantages that enhance productivity and safety. These include reduced downtime due to minimal maintenance requirements, improved material handling efficiency through optimized conveyor speeds and capacities, and enhanced worker safety by eliminating exposure to dust and airborne contaminants. The systems are typically equipped with advanced control panels that allow for real-time monitoring and adjustment of operational parameters. Technical specifications vary based on the specific application, but common features include adjustable conveyor speeds, variable load capacities, and compatibility with a wide range of material types. The systems are designed to be scalable, allowing for integration into existing production lines or expansion as operational needs grow. Additionally, the use of high-quality materials and precision engineering ensures long-term reliability and consistent performance, even under harsh operating conditions.
Conclusion and Company Overview
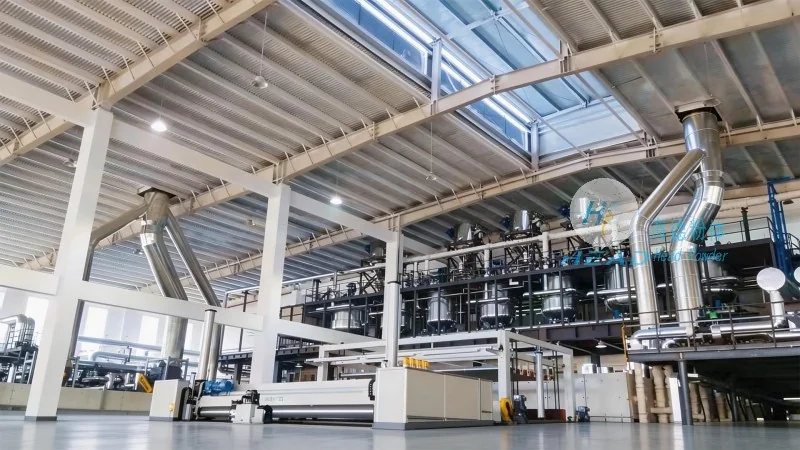
HeadPowder Engineering Co., Ltd., based in Shandong, China, is a trusted partner in providing cutting-edge dust-free and airtight material conveying solutions. With a strong commitment to innovation and customer satisfaction, the company has established itself as a leader in the industrial material handling sector. The principles and working scene characteristics of these systems underscore their importance in modern industrial operations, where maintaining product quality, ensuring worker safety, and adhering to regulatory standards are non-negotiable. By leveraging advanced technology and expert engineering, HeadPowder continues to deliver reliable and efficient solutions that meet the evolving needs of its clients across various industries.




