HeadPowder, a leading provider of industrial powder handling solutions, specializes in the design and implementation of efficient quartz sand powder conveying systems. Based in Shandong, China, the company has established itself as a trusted partner for businesses requiring reliable and high-performance material transport solutions. This article explores the fundamental principles behind quartz sand powder conveying systems and highlights the key characteristics of their operational environments.
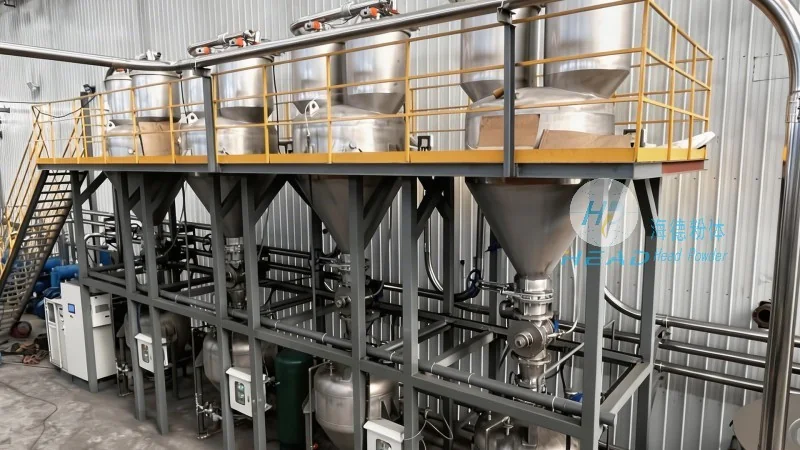
Overview of Quartz Sand Powder Conveying Systems
Quartz sand, a widely used industrial material, often requires specialized handling due to its granular nature and potential for dust generation. Powder conveying systems are engineered to transport quartz sand from one location to another while maintaining product integrity, minimizing material loss, and ensuring operational safety. These systems typically consist of components such as hoppers, feeders, conveying lines, and discharge equipment, each playing a critical role in the overall process.
The Core Principles of Powder Conveying
The operation of quartz sand powder conveying systems is based on several key principles, including the control of particle flow, pressure differentials, and material properties. For instance, in pneumatic conveying systems, air is used to create a flow that transports the sand particles through a pipeline. This method can be either positive pressure (where air is blown into the system) or negative pressure (where air is drawn out). The choice of system depends on factors like the distance to be covered, the volume of material, and the need to minimize dust exposure.
Another principle involves the use of mechanical conveyors, such as screw or belt conveyors, which rely on physical movement to transport the sand. These systems are often preferred for shorter distances or when the material is prone to clogging. The selection of the appropriate conveying method is crucial to ensure efficient and safe operation, as improper design can lead to blockages, increased energy consumption, or product degradation.
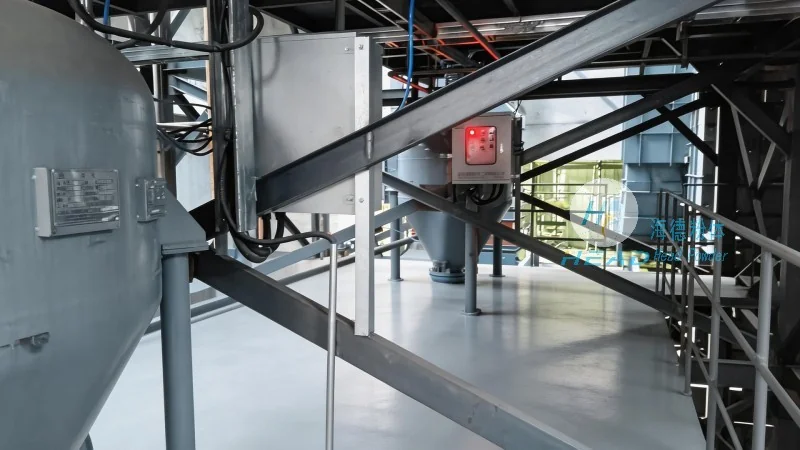
Working Scene Characteristics
The operational environments for quartz sand powder conveying systems vary significantly based on the application and industry. In mining operations, for example, these systems are used to transport sand from extraction sites to processing facilities, often under conditions of high dust and varying particle sizes. The systems must be robust enough to handle abrasive materials and withstand harsh environmental factors.
In the chemical and pharmaceutical industries, the focus shifts to maintaining product purity and preventing contamination. Here, conveying systems are designed with enclosed pipelines and filtration systems to ensure that the quartz sand remains free from impurities and does not come into contact with external contaminants. The working environment may also involve strict temperature and humidity controls, which the system must accommodate.
In construction and building materials applications, the systems are used to transport sand for concrete production or other construction processes. The operational scenes in this sector often involve large volumes of material and require systems that can handle high throughput while maintaining efficiency and cost-effectiveness. The systems must also be adaptable to different site conditions, such as varying ground levels or limited space.
Key Features and Advantages
Quartz sand powder conveying systems from HeadPowder Engineering Co., Ltd. are designed with several features that enhance their performance and reliability. These include advanced control systems that allow for precise regulation of material flow, reducing waste and improving process efficiency. The systems also incorporate safety features, such as dust suppression and explosion-proof designs, to protect personnel and equipment in high-risk environments.
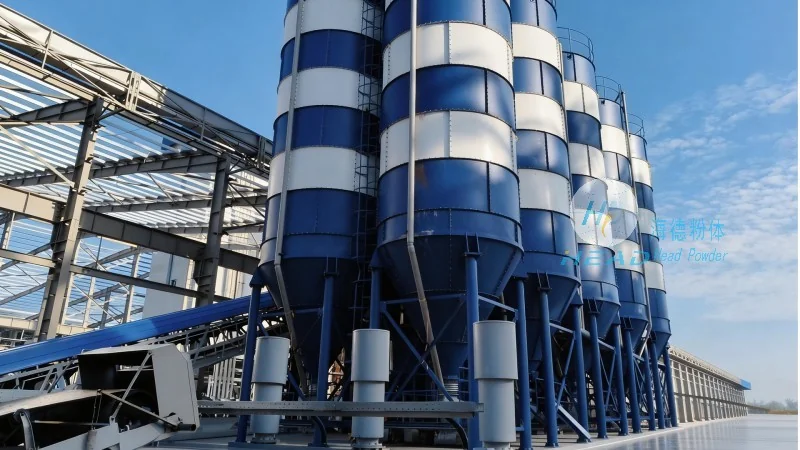
Another advantage is the flexibility of these systems, which can be customized to meet the specific needs of different applications. Whether it's a small-scale operation or a large industrial plant, the conveying systems can be scaled to handle varying volumes and particle sizes. This adaptability makes them suitable for a wide range of industries, from mining and construction to chemical processing.
The use of high-quality materials in the construction of the conveying components ensures durability and longevity, reducing maintenance costs over the system's lifespan. Additionally, the systems are engineered for low energy consumption, contributing to cost savings and environmental sustainability.
Conclusion
Quartz sand powder conveying systems are essential for the efficient and safe transport of this critical industrial material. By understanding the core principles and working scene characteristics, businesses can select the most appropriate system for their needs. HeadPowder Engineering Co., Ltd., with its expertise and commitment to quality, provides reliable solutions that meet the demands of various industries, ensuring optimal performance and operational success.




