Understanding the fundamental principles and operational characteristics of potassium carbonate powder conveying systems is crucial for industries that rely on efficient material handling. This article provides an in-depth exploration of the core mechanisms behind these systems, alongside an analysis of their typical working environments and applications.
Principle of Operation for Potassium Carbonate Powder Conveying Systems
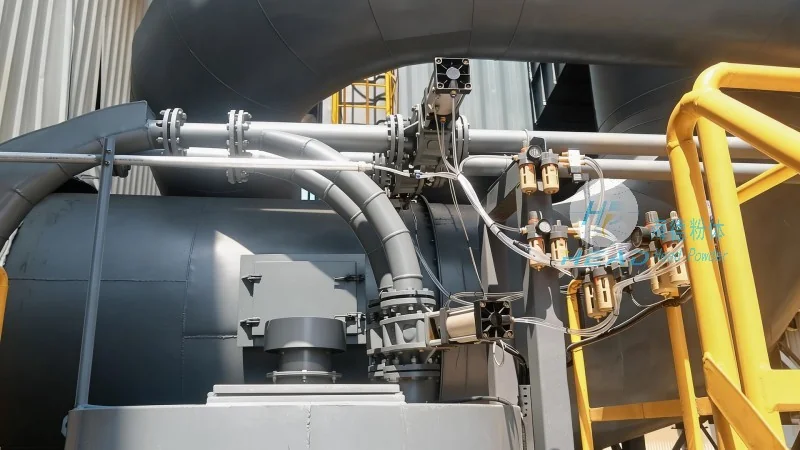
The operation of a potassium carbonate powder conveying system is based on several key principles that ensure reliable and efficient material transport. At its core, the system utilizes a combination of mechanical and pneumatic components to move the powder from its source to the destination. The process typically begins with the loading of the potassium carbonate powder into a hopper or storage container. From there, the powder is fed into a conveyor system, which may include screw conveyors, pneumatic ducts, or other specialized equipment designed to handle fine powders like potassium carbonate.
One of the primary mechanisms is the use of air pressure or vacuum to create a flow of the powder through the conveying lines. This method, known as pneumatic conveying, is particularly effective for potassium carbonate due to its fine particle size and potential for dust generation. The system often incorporates features such as rotary valves, airlocks, and filters to control the flow rate and prevent material buildup or leakage. Additionally, the design may include temperature control and moisture management components to maintain the quality of the potassium carbonate during transport, as these factors can significantly impact its chemical properties and usability.
Working Scene Characteristics of Potassium Carbonate Powder Conveying Systems
The working environments where potassium carbonate powder conveying systems are applied vary widely, reflecting the diverse industrial uses of potassium carbonate. These systems are commonly found in chemical manufacturing facilities, where potassium carbonate is used as a raw material in the production of various chemicals, pharmaceuticals, and food additives. In such settings, the system must handle large volumes of powder and operate under strict quality control measures to ensure that the material remains pure and free from contaminants.
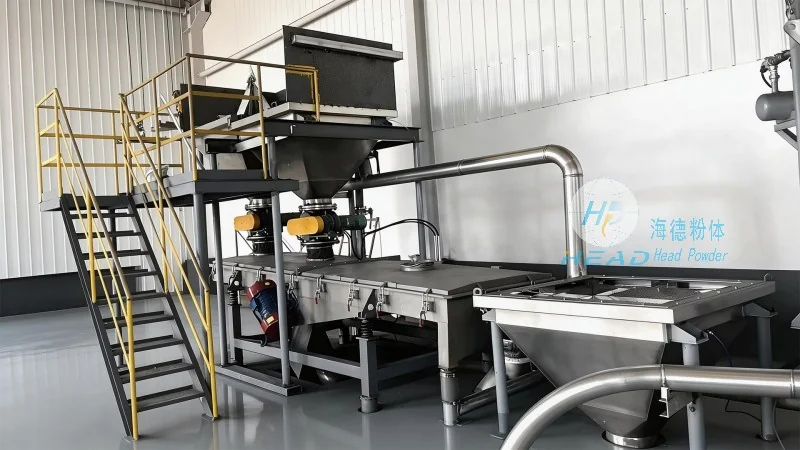
Another common application is in the food and beverage industry, where potassium carbonate is used as a leavening agent or pH regulator. The conveying systems in these facilities must meet stringent hygiene standards, often incorporating stainless steel components and closed-loop systems to prevent cross-contamination and maintain food safety regulations. Additionally, the systems may be integrated with packaging lines, where the powder is transferred directly into packaging containers, requiring precise control over flow rates and particle distribution.
In the pharmaceutical sector, the requirements for powder conveying systems are even more stringent, focusing on sterility, purity, and traceability. These systems may include additional filtration and decontamination steps to ensure that the potassium carbonate is suitable for use in drug formulations. The working environment in pharmaceutical plants is typically clean and controlled, with the conveying system operating under aseptic conditions to prevent microbial contamination.
About Shandong HeadPowder Engineering Co., Ltd.
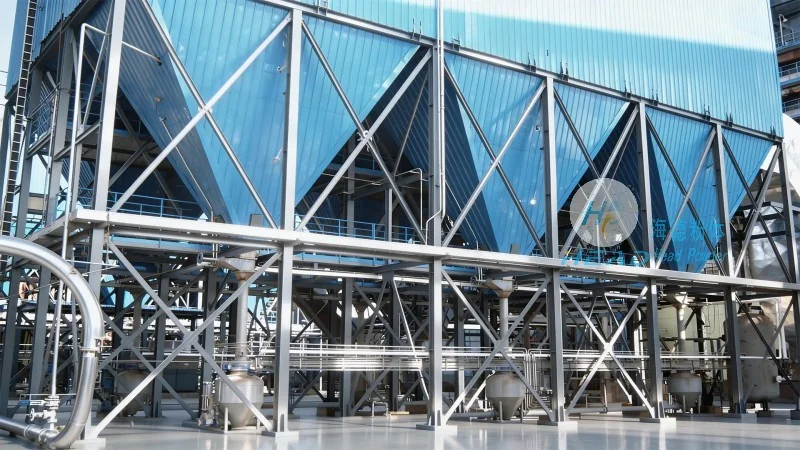
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading provider of specialized powder handling solutions. With a focus on innovation and customer-centric design, the company has developed advanced conveying systems tailored to the unique needs of industries handling potassium carbonate and other fine powders. HeadPowder's expertise lies in designing systems that balance efficiency, reliability, and safety, ensuring that clients can meet their production targets while maintaining the highest standards of material quality.
HeadPowder's facilities are located in Shandong, China, where the company leverages local manufacturing capabilities and a strong supply chain to deliver high-quality products and services. The company's commitment to research and development ensures that its systems incorporate the latest technologies in powder handling, such as advanced control systems, energy-efficient designs, and materials that resist corrosion and wear from potassium carbonate particles.
By combining technical expertise with practical application knowledge, HeadPowder has established itself as a trusted partner for businesses seeking reliable and effective potassium carbonate powder conveying solutions. The company's systems are designed to adapt to various operational conditions and industry requirements, providing customized solutions that enhance productivity and reduce operational costs for its clients.




