HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced pneumatic conveying systems tailored for the handling of anhydrous sodium sulfate. This article delves into the fundamental principles behind such systems and highlights the key operational characteristics that define their effectiveness in industrial applications.
Understanding the Core Principle of Pneumatic Conveying for Anhydrous Sodium Sulfate
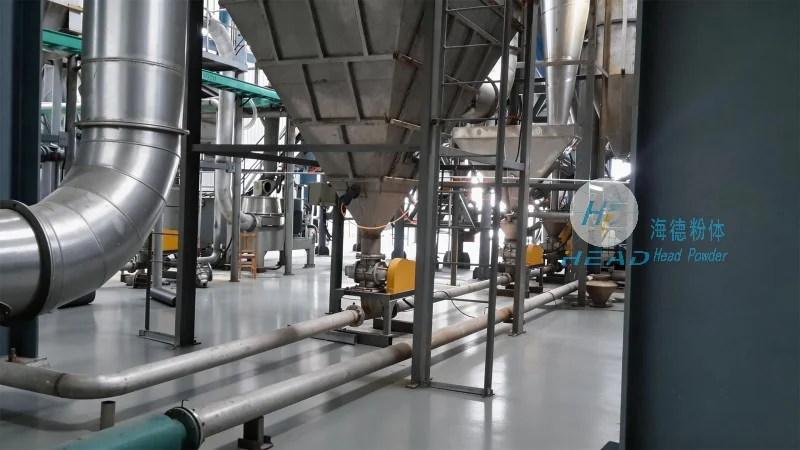
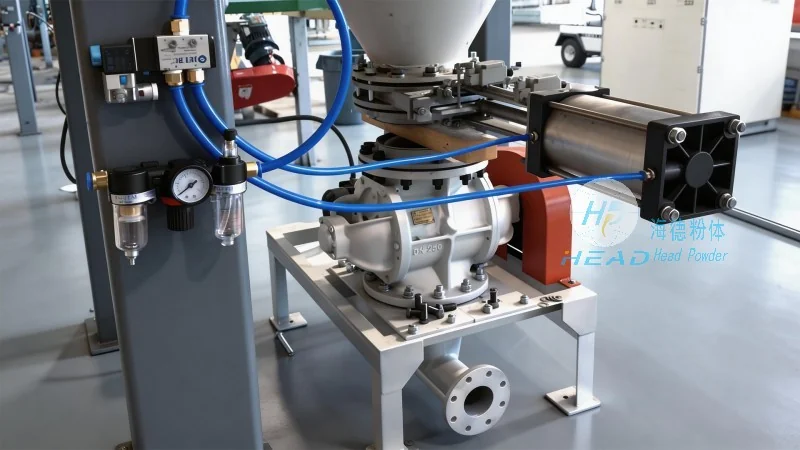
The pneumatic conveying system for anhydrous sodium sulfate operates on the principle of using compressed air to transport bulk materials through a pipeline. Unlike traditional mechanical conveyors, this method eliminates the need for moving parts in the conveying path, reducing maintenance requirements and enhancing safety. The system typically consists of a hopper, a rotary valve, a conveyor pipe, and a dust collector. The anhydrous sodium sulfate is fed into the hopper, and as compressed air is introduced, it creates a flow that propels the material through the pipeline to the discharge point. This process is highly efficient for handling fine powders and granular materials, ensuring minimal product degradation and consistent flow rates.
Key Operational Characteristics and Advantages
One of the primary advantages of the anhydrous sodium sulfate pneumatic conveying system is its ability to handle materials with high moisture content or those prone to caking, as the air flow prevents agglomeration. The system also offers flexibility in terms of layout, allowing for vertical, horizontal, or combined vertical-horizontal transport, which is crucial for optimizing space in industrial facilities. Additionally, the enclosed pipeline design minimizes dust emissions, contributing to a cleaner working environment and compliance with environmental regulations. The system's efficiency in material transfer is further enhanced by the use of variable speed drives and pressure control mechanisms, which allow for precise adjustment of flow rates based on operational needs.
Typical Work Scenarios and Applications
The anhydrous sodium sulfate pneumatic conveying system is widely used in various industrial sectors, including chemical manufacturing, food processing, and mining. In chemical plants, it facilitates the transfer of raw materials between processing units, ensuring a continuous and controlled supply of anhydrous sodium sulfate for production processes. In food processing facilities, the system is employed to transport ingredients with strict hygiene requirements, maintaining product purity and preventing contamination. The mining industry also benefits from this technology, as it enables the efficient transport of anhydrous sodium sulfate from storage areas to processing equipment, reducing labor costs and improving overall operational efficiency. Each application leverages the system's ability to handle large volumes of material with minimal downtime, making it a reliable solution for demanding industrial environments.
Conclusion and Company Overview
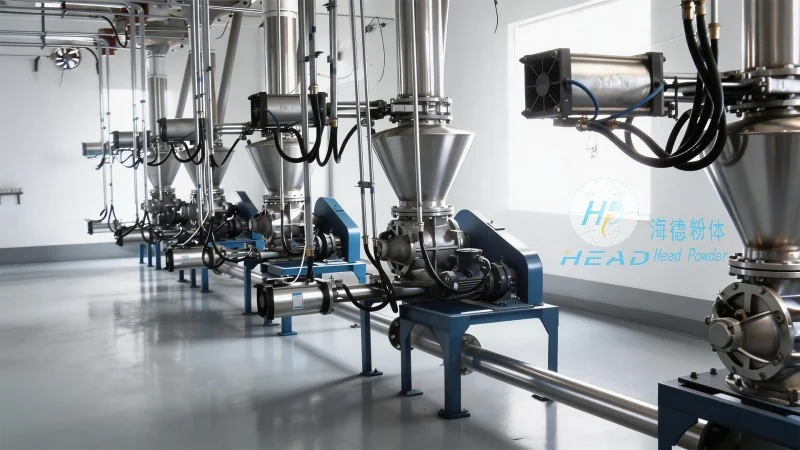
HeadPowder Engineering Co., Ltd., based in Shandong, China, is dedicated to providing high-quality pneumatic conveying solutions for anhydrous sodium sulfate and other bulk materials. By integrating advanced engineering principles and robust manufacturing processes, the company ensures that its systems meet the highest standards of performance, reliability, and safety. The operational characteristics discussed, such as efficient material transfer, flexible layout options, and environmental compliance, make the anhydrous sodium sulfate pneumatic conveying system an ideal choice for industries seeking to optimize their material handling processes. With a commitment to innovation and customer satisfaction, HeadPowder continues to lead in the development of cutting-edge conveying technologies for the global market.




