HeadPowder, a leading provider in the field of material handling solutions, specializes in the design, manufacturing, and implementation of dilute phase pneumatic conveying systems. These systems are engineered to efficiently transport bulk materials over long distances with minimal operational complexity. This article delves into the fundamental principles behind these systems and highlights the key working scenarios where they excel, providing a comprehensive overview for potential users and industry professionals.
Company Overview and Expertise
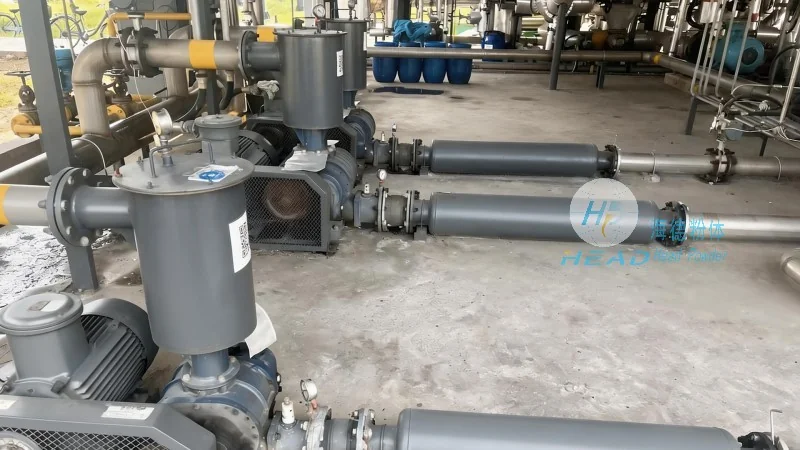
HeadPowder Engineering Co., Ltd., headquartered in Shandong, China, has established itself as a trusted name in the engineering and manufacturing of pneumatic conveying equipment. With years of experience and a commitment to innovation, the company focuses on delivering high-performance solutions tailored to diverse industrial needs. The expertise of HeadPowder lies in understanding the unique requirements of material handling processes, enabling the development of customized dilute phase systems that optimize efficiency and reliability.
The Principle of Dilute Phase Pneumatic Conveying
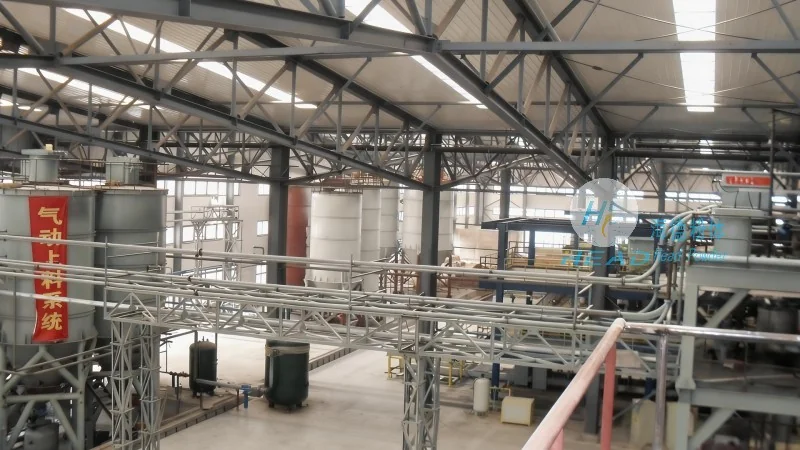
Dilute phase pneumatic conveying systems operate on the principle of transporting particulate materials in a dilute suspension within a high-velocity air stream. Unlike dense phase systems, where materials are conveyed in a more compacted form, dilute phase systems rely on the kinetic energy of the air to move particles through the pipeline. The process involves generating a high-velocity air flow, typically using positive displacement blowers or centrifugal fans, which draws the material into the conveying line. As the material is suspended in the air, it travels through the pipeline, often with multiple bends and changes in elevation, before being discharged at the destination. The key to efficient operation lies in maintaining an optimal air-to-material ratio, ensuring that the particles remain in suspension throughout the conveying process.
Key Working Scenario Characteristics
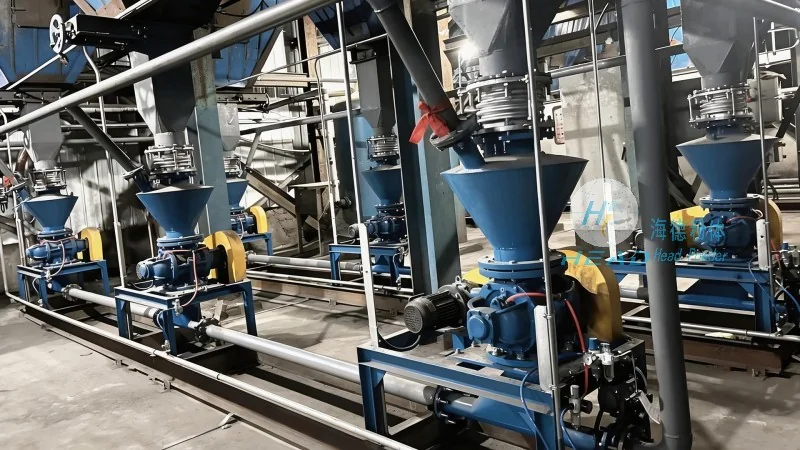
Dilute phase pneumatic conveying systems are particularly well-suited for applications requiring long-distance material transport, where traditional methods such as belt conveyors or bucket elevators may be impractical or inefficient. The systems excel in scenarios involving the transfer of fine powders, granules, and other dry bulk materials. For instance, in the chemical industry, these systems are commonly used to transport raw materials like powders and granules from storage silos to processing units, ensuring a continuous and dust-free operation. In the food processing sector, dilute phase systems are employed to handle ingredients such as flour, sugar, and spices, maintaining hygiene standards and preventing contamination. Additionally, in the pharmaceutical industry, where material purity is paramount, these systems provide a clean and controlled method of material transfer, minimizing the risk of cross-contamination.
Advantages and Operational Benefits
One of the primary advantages of dilute phase pneumatic conveying systems is their ability to transport materials over significant distances with minimal infrastructure requirements. Unlike mechanical conveyors, which may require extensive civil works and structural supports, pneumatic systems can be installed in existing facilities or in new constructions with relative ease. The systems also offer flexibility in terms of layout, allowing for changes in the conveying path without major modifications to the infrastructure. Furthermore, dilute phase systems provide a dust-free and enclosed environment, which is crucial in industries where material containment and environmental compliance are critical. The operation of these systems is generally low-maintenance, with components such as blowers and filters requiring regular maintenance to ensure optimal performance. The energy efficiency of dilute phase systems, particularly when using high-efficiency blowers, contributes to lower operational costs over time.
Conclusion
HeadPowder Engineering Co., Ltd. offers comprehensive solutions for dilute phase pneumatic conveying systems, leveraging advanced engineering and manufacturing capabilities to meet the diverse needs of various industries. By understanding the fundamental principles and working scenarios of these systems, users can make informed decisions about their material handling requirements. The company's commitment to quality, innovation, and customer satisfaction ensures that clients receive reliable and efficient systems that enhance operational productivity and reduce costs. With a strong presence in Shandong, China, HeadPowder continues to be a leader in providing cutting-edge material handling solutions that drive industrial efficiency and sustainability.




