Intelligent centralized pneumatic conveying systems represent a sophisticated solution for material handling in various industrial applications. These systems are designed to efficiently transport bulk materials over long distances with minimal human intervention, leveraging advanced technology to optimize performance and reliability. The following content explores the fundamental principles behind such systems and highlights key working scene characteristics that define their operational effectiveness.
Company Overview and Background
HeadPowder, a leading manufacturer in the field, specializes in the design, development, and implementation of advanced pneumatic conveying solutions. With headquarters in Shandong, China, the company has established itself as a trusted partner for industries seeking reliable material handling technologies. The expertise and innovation at HeadPowder are integral to the creation of intelligent centralized systems that meet diverse operational needs.
Core Principles of Intelligent Centralized Pneumatic Conveying Systems
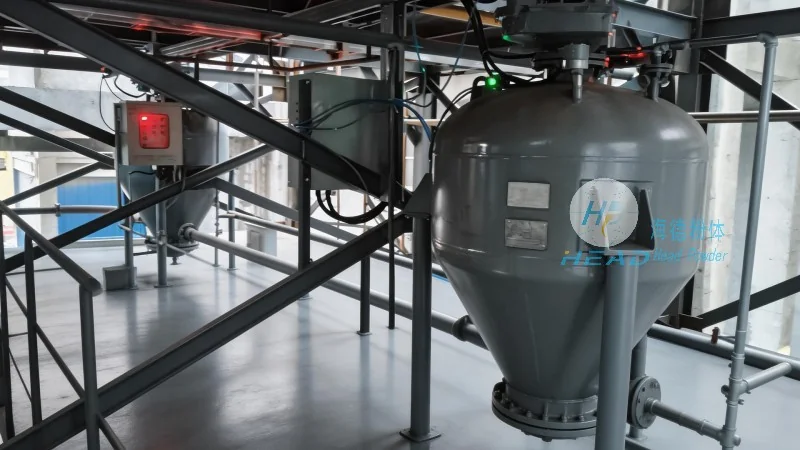
The operation of intelligent centralized pneumatic conveying systems is grounded in the principles of pneumatic transport, where materials are conveyed through a network of pipes using air or gas as the medium. These systems typically consist of several key components, including a material feeding unit, a conveying line, a control system, and a discharge point. The intelligent aspect of these systems is realized through advanced control algorithms and sensors that monitor and adjust operational parameters in real-time, ensuring optimal performance and energy efficiency.
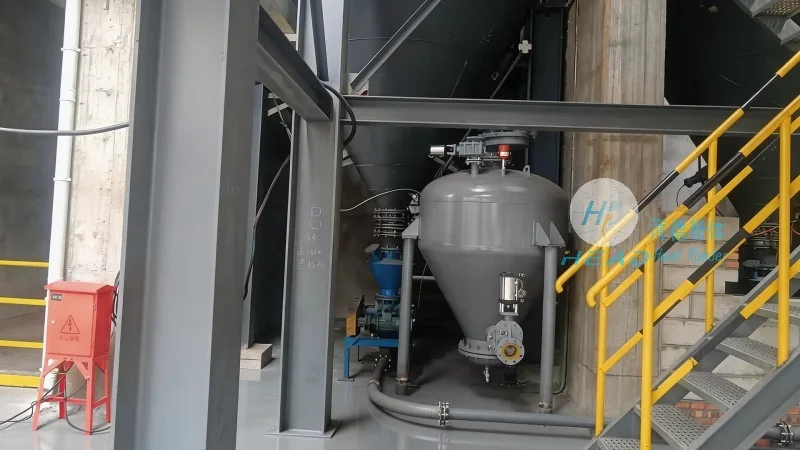
One of the primary principles is the use of differential pressure to move materials. By creating a pressure differential between the intake and discharge points, the system propels the material through the pipeline. The intelligent control system continuously adjusts the pressure and flow rates to maintain consistent material transport, preventing issues such as blockages or uneven flow. Additionally, the system incorporates feedback mechanisms that allow for adaptive adjustments based on real-time data, enhancing overall reliability and reducing downtime.
Working Scene Characteristics and Applications
Intelligent centralized pneumatic conveying systems are widely utilized across various industrial sectors, including pharmaceuticals, food processing, chemical manufacturing, and mining. The working scene characteristics of these systems are tailored to meet the specific demands of each application, ensuring efficient material handling while maintaining product integrity and safety standards.
In pharmaceutical and food processing industries, where hygiene and contamination control are paramount, these systems are designed with stainless steel components and sealed piping to prevent cross-contamination. The intelligent control features allow for precise dosing and cleaning cycles, ensuring compliance with regulatory requirements. For example, in a pharmaceutical plant, the system may be used to transport active pharmaceutical ingredients (APIs) or finished dosage forms, with real-time monitoring to detect any deviations in flow or pressure.
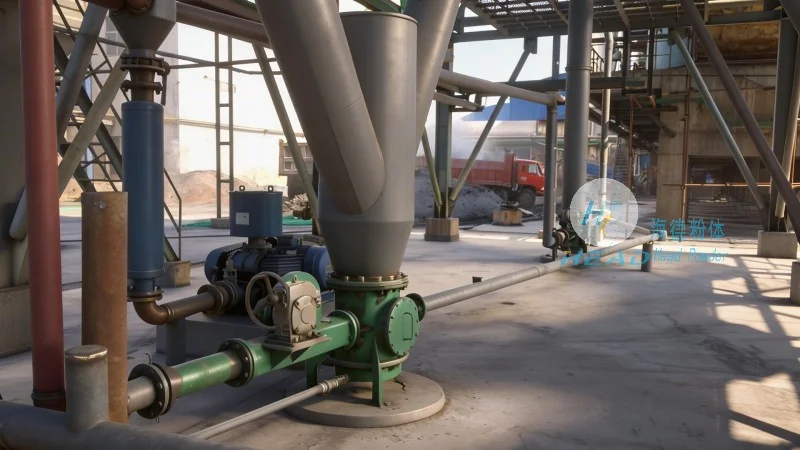
In chemical manufacturing, the systems handle a variety of powders and granules, often requiring temperature control and explosion-proof designs. The intelligent features enable safe operation in hazardous environments by monitoring gas levels and automatically adjusting system parameters to prevent ignition risks. This ensures that the material is conveyed safely and efficiently, minimizing the risk of accidents and product damage.
In the mining and minerals processing sector, large volumes of bulk materials are transported over long distances. The centralized design allows for the integration of multiple feeding points and discharge locations, optimizing the flow of raw materials to processing plants. The intelligent control system optimizes energy consumption by adjusting the air pressure based on the material load and distance, reducing operational costs while maintaining high throughput.
Advantages and Operational Benefits
The intelligent centralized pneumatic conveying systems offer several advantages over traditional material handling methods. These include reduced labor costs due to minimal manual intervention, lower maintenance requirements through predictive diagnostics, and improved product quality by minimizing material degradation during transport. The centralized design also allows for better space utilization in industrial facilities, as the system can be integrated into existing layouts without significant modifications.
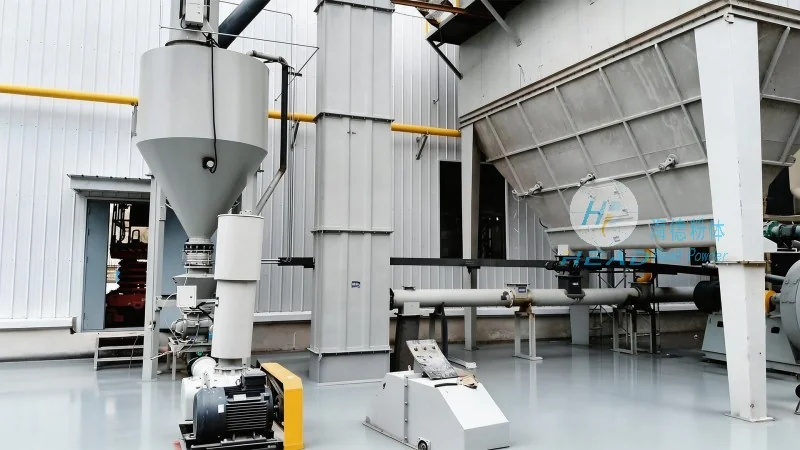
Furthermore, the real-time monitoring and control features provide operators with comprehensive insights into system performance, enabling proactive maintenance and quick resolution of issues. This leads to increased system uptime and overall operational efficiency. The adaptability of these systems to different materials and operational conditions makes them a versatile solution for a wide range of industrial applications.
Conclusion
Intelligent centralized pneumatic conveying systems, as exemplified by solutions from Shandong HeadPowder Engineering Co., Ltd., represent a cutting-edge approach to material handling. By integrating advanced control technologies and intelligent monitoring, these systems provide efficient, reliable, and safe transport of bulk materials across diverse industrial applications. The working scene characteristics and operational benefits highlight the effectiveness of such systems in optimizing industrial processes and reducing operational costs.




