Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in China, specializes in providing advanced solutions for the handling and transportation of bulk materials. Among their product offerings is the Ammonium Bicarbonate Powder Pneumatic Conveying Line, a sophisticated system designed to efficiently manage the movement of this specific chemical compound. This article delves into the working principle and key features of this system, highlighting its practical applications and technical advantages.
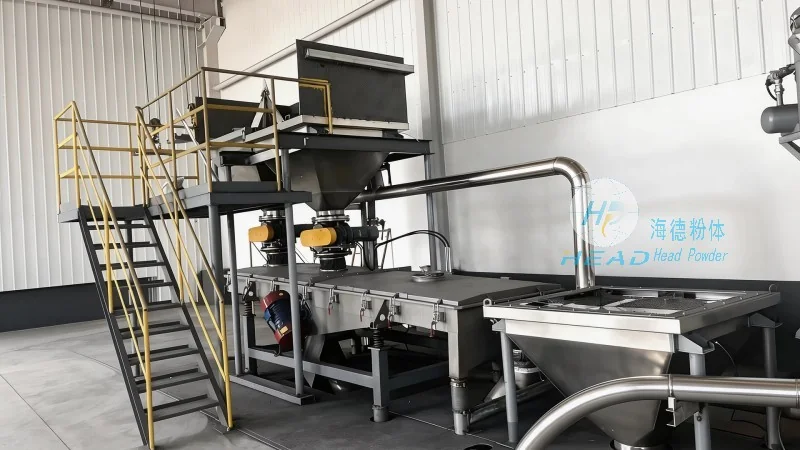
Overview of the Ammonium Bicarbonate Powder Pneumatic Conveying Line
The Ammonium Bicarbonate Powder Pneumatic Conveying Line is a specialized system engineered to transport ammonium bicarbonate, a white crystalline powder commonly used in agricultural fertilizers and industrial processes, through a pneumatic conveying mechanism. This technology eliminates the need for traditional mechanical conveying methods, such as belt conveyors or screw conveyors, which can be prone to material degradation or blockages. By utilizing compressed air or other gas streams, the system ensures a clean, efficient, and low-maintenance approach to bulk material handling.
The Working Principle of the Pneumatic Conveying System
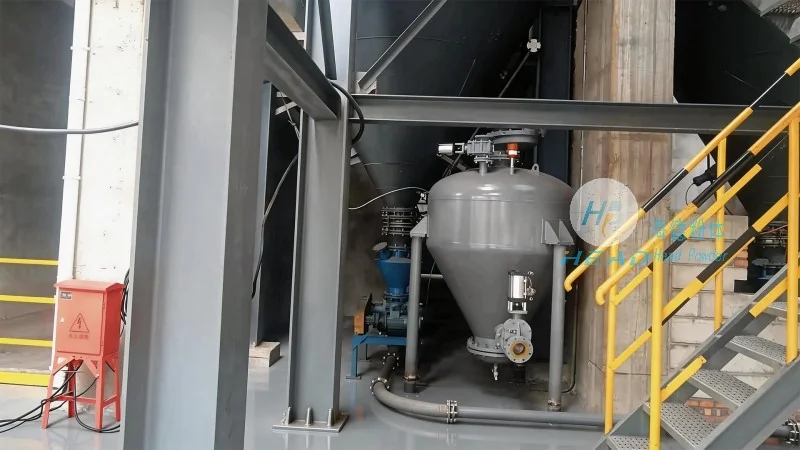
The core of the Ammonium Bicarbonate Powder Pneumatic Conveying Line operates on the principle of pneumatic transport, where the powder is suspended and propelled by a moving gas stream. The process typically involves several key components: a hopper for material storage, a rotary valve or feeder to control the flow rate, a pipeline system for material transport, and a receiver or discharge unit for the final delivery. Compressed air is introduced into the pipeline, creating a pressure differential that lifts and carries the ammonium bicarbonate particles through the system. The velocity of the gas is carefully controlled to maintain a stable flow, preventing particle agglomeration and ensuring consistent delivery.
Key Features and Technical Advantages
Several notable features distinguish the Ammonium Bicarbonate Powder Pneumatic Conveying Line from conventional conveying systems. Firstly, it offers a high degree of flexibility in terms of layout and installation, as the pipeline can be configured to follow complex routes without the need for extensive structural modifications. Secondly, the system minimizes material contamination and degradation, as it operates in a closed environment, protecting the ammonium bicarbonate from moisture, dust, or other external factors that could affect its quality. Additionally, the pneumatic conveying mechanism reduces the risk of product spillage and dust emissions, contributing to a safer and more environmentally friendly operation.
Application Scenarios and Performance Metrics
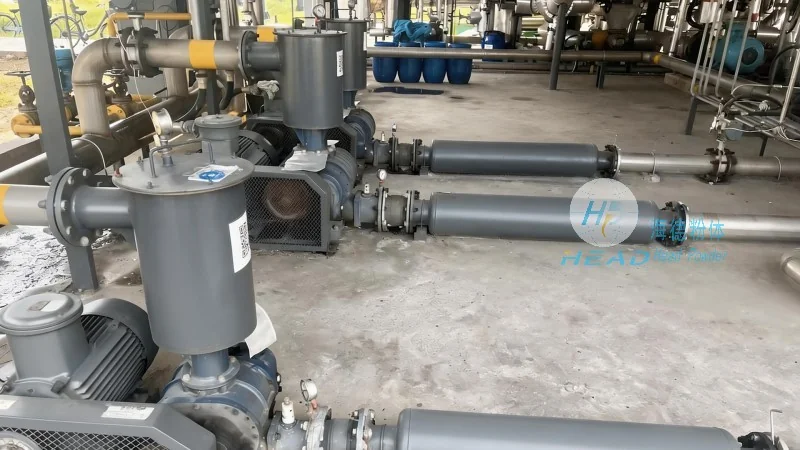
The Ammonium Bicarbonate Powder Pneumatic Conveying Line is particularly well-suited for applications in the agricultural and chemical industries, where the efficient handling of bulk powders is critical. It is commonly used in fertilizer production facilities, where large quantities of ammonium bicarbonate need to be transported from storage silos to processing units or packaging lines. The system’s ability to handle high flow rates and maintain consistent material quality makes it an ideal solution for these demanding environments. Performance metrics such as conveying capacity, pressure drop, and energy efficiency are optimized through precise design and engineering, ensuring reliable operation over extended periods.
Conclusion and Company Expertise
Shandong HeadPowder Engineering Co., Ltd. has established itself as a trusted provider of specialized material handling solutions, including the Ammonium Bicarbonate Powder Pneumatic Conveying Line. With a strong commitment to innovation and quality, the company continues to enhance its products to meet the evolving needs of the industry. By leveraging advanced pneumatic conveying technology, this system offers a reliable and efficient means of transporting ammonium bicarbonate, supporting the productivity and sustainability of operations in various sectors. For businesses seeking to optimize their bulk material handling processes, the Ammonium Bicarbonate Powder Pneumatic Conveying Line represents a robust and effective solution.




