Crystalline material conveying equipment is a specialized type of machinery designed to handle and transport crystalline substances efficiently. These materials, often found in industries such as pharmaceuticals, chemicals, and food processing, require precise handling due to their unique physical properties. The equipment from Shandong HeadPowder Engineering Co., Ltd. is engineered to meet these demands, ensuring safe and reliable operation in various industrial applications.
Working Principle of Crystalline Material Conveying Equipment
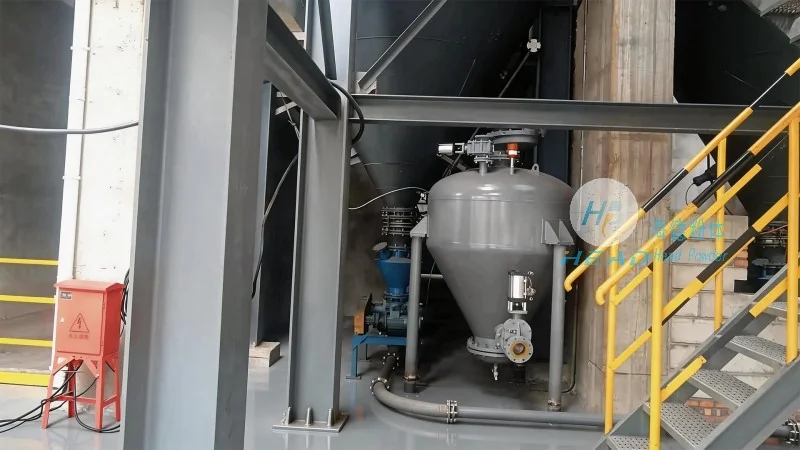
The core working principle of crystalline material conveying equipment involves the use of mechanical components to move solid crystalline materials from one location to another. Typically, these systems employ a combination of mechanisms such as screw conveyors, belt conveyors, or pneumatic transport systems, depending on the specific characteristics of the material being handled. The equipment is designed to maintain the integrity of the crystalline particles, preventing breakage or agglomeration during transport. For instance, in screw conveyors, a rotating screw (or auger) pushes the material forward through a closed tube, ensuring a controlled and consistent flow. This method is particularly effective for materials that are free-flowing but may require gentle handling to avoid damage. Belt conveyors, on the other hand, use a continuous belt to transport materials, which is ideal for larger or bulkier crystalline products. Pneumatic systems utilize air pressure to move materials through a pipeline, offering a dust-free and enclosed transport solution, especially beneficial for materials that are sensitive to contamination or environmental factors.
Key Features of Crystalline Material Conveying Equipment
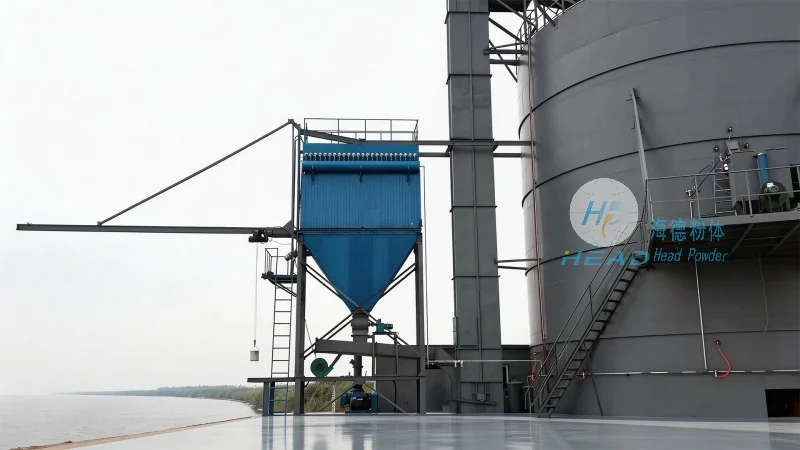
Shandong HeadPowder Engineering Co., Ltd. offers crystalline material conveying equipment with several key features that enhance performance and reliability. One of the primary features is the ability to handle a wide range of crystalline materials, from fine powders to larger granules, without compromising the quality of the product. The equipment is designed with adjustable speed controls, allowing operators to modify the conveying rate based on the specific requirements of the material and the production process. This flexibility ensures optimal efficiency and prevents overloading or underloading of the system. Another notable feature is the robust construction, which includes materials resistant to corrosion and wear, ensuring long-term durability and minimal maintenance. The equipment also incorporates safety features such as overload protection and emergency stop mechanisms, safeguarding both the machinery and the personnel operating it. Additionally, the design often includes cleaning mechanisms to maintain hygiene, which is crucial in industries like pharmaceuticals and food processing where product purity is paramount. The equipment is also equipped with monitoring systems that provide real-time data on the conveying process, enabling operators to detect and address any issues promptly, thereby improving overall operational efficiency.
Application-Specific Advantages
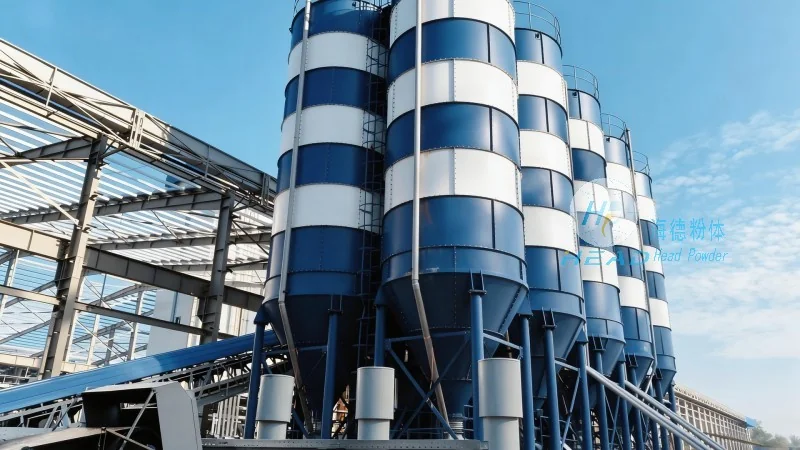
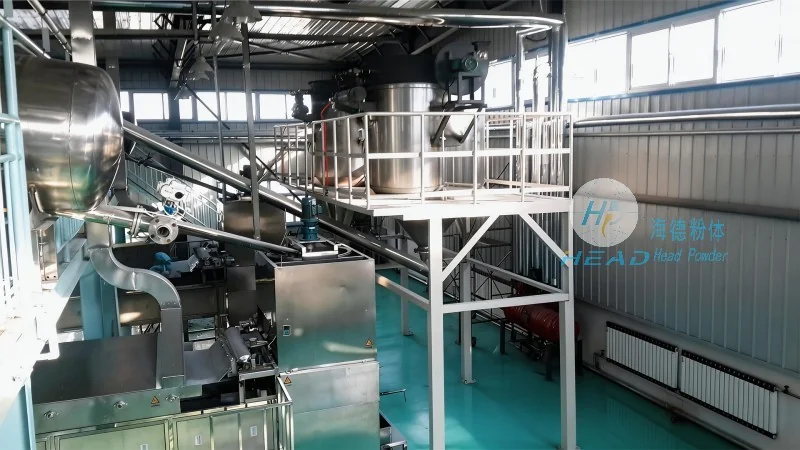
The advantages of crystalline material conveying equipment extend to various industrial applications. In the pharmaceutical industry, for example, the equipment is used to transport active pharmaceutical ingredients (APIs) and excipients, ensuring that the materials remain pure and free from contamination. The gentle handling and enclosed design prevent cross-contamination, which is critical in maintaining product quality and regulatory compliance. In the chemical industry, the equipment is utilized to transport chemical crystals, such as those used in the production of fertilizers or specialty chemicals. The ability to handle abrasive materials without causing wear to the equipment components is a significant advantage, as it reduces maintenance costs and extends the lifespan of the machinery. Similarly, in the food processing industry, the equipment is employed to transport food-grade crystalline products, such as sugar or salt, ensuring that the products are handled hygienically and without any additives. The equipment's design, which often includes stainless steel components and easy-to-clean surfaces, meets the stringent hygiene standards required in food processing facilities. Overall, the equipment from Shandong HeadPowder Engineering Co., Ltd. offers a reliable and efficient solution for transporting crystalline materials, tailored to meet the specific needs of different industries.
Conclusion
Crystalline material conveying equipment from Shandong HeadPowder Engineering Co., Ltd. combines advanced engineering with practical design to provide an effective solution for transporting crystalline materials. The working principle, which may vary based on the specific application, ensures that the materials are handled with care, maintaining their integrity and quality. The key features, including adjustable speed controls, robust construction, and safety mechanisms, enhance the equipment's performance and reliability. With applications spanning pharmaceuticals, chemicals, and food processing, the equipment offers significant advantages in terms of efficiency, safety, and compliance. As a leading manufacturer based in China, Shandong HeadPowder Engineering Co., Ltd. continues to innovate and provide high-quality conveying solutions that meet the evolving needs of the industrial sector.




