

What is a Calcined Ash Material Pneumatic Conveying Equipment? And What Are Its Design Principles?
Calcined ash material pneumatic conveying equipment is a specialized system designed to transport calcined ash, a byproduct of industrial processes such as coal combustion or metal smelting, from one location to another. This equipment plays a crucial role in modern industrial operations by providing an efficient, reliable, and often dust-free method of material handling. The system typically consists of a hopper, a conveyor line, and a control unit, all working in tandem to ensure smooth material transport. Understanding the components and design principles of this equipment is essential for optimizing industrial processes and maintaining operational efficiency.
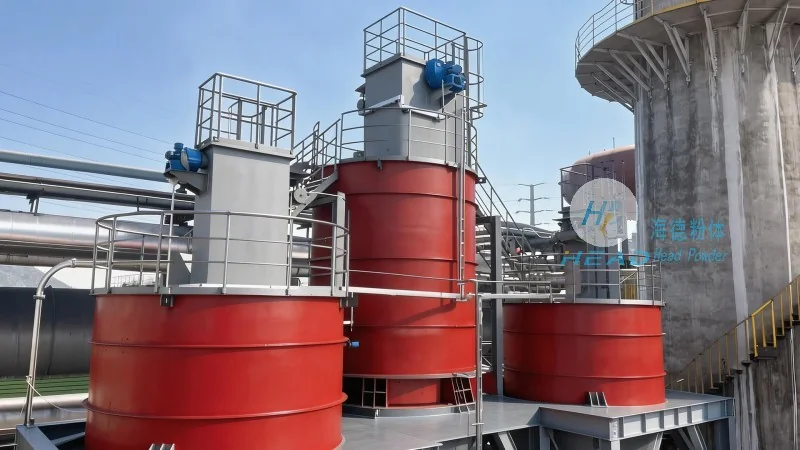
Key Components of the Pneumatic Conveying System
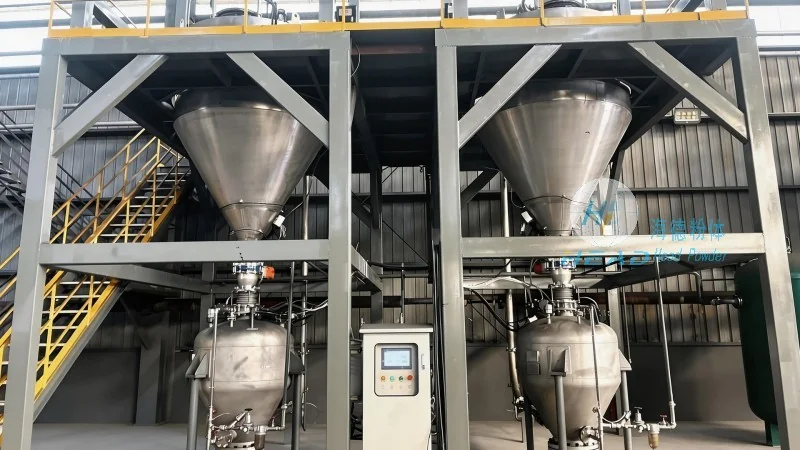
The calcined ash material pneumatic conveying equipment is composed of several key components that work together to facilitate material transport. The primary components include a material hopper, which stores the calcined ash and feeds it into the system; a conveying line, which can be either a positive or negative pressure system depending on the application; and a control unit that regulates the flow and pressure within the system. Additionally, the system may include a filter or dust collector to capture any airborne particles and prevent environmental contamination. Each component is carefully designed to handle the specific characteristics of calcined ash, such as its density, moisture content, and particle size, ensuring optimal performance.
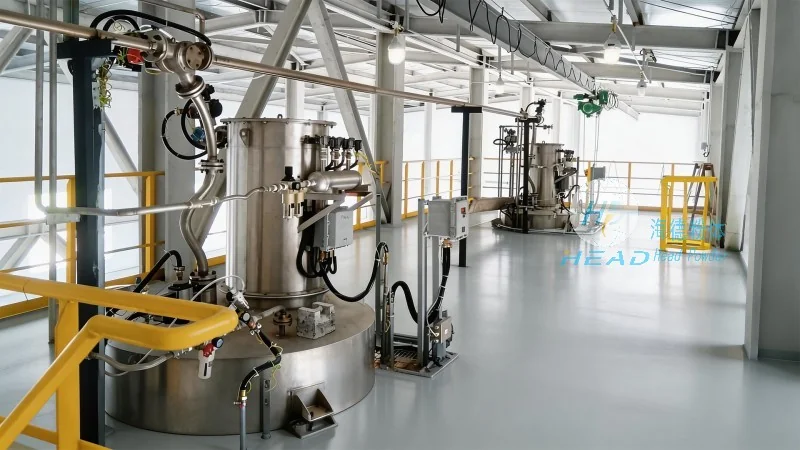
Design Principles for Efficient Material Handling
The design principles of calcined ash material pneumatic conveying equipment are centered on maximizing efficiency, reliability, and safety. One of the core principles is the selection of the appropriate conveying method, which can be either pressure or vacuum-based. Pressure systems use compressed air to push the material through the line, while vacuum systems use suction to draw the material. The choice between these methods depends on factors such as the distance to be covered, the material's properties, and the desired flow rate. Another critical design principle is the sizing of the conveying line and components, which must be matched to the material's flow characteristics to prevent blockages or excessive pressure drops. The system also incorporates features like flow meters and pressure sensors to monitor performance in real-time, allowing for adjustments to maintain optimal operation. Furthermore, the design emphasizes durability and corrosion resistance, as calcined ash can be abrasive and may contain corrosive elements, ensuring the equipment can withstand long-term use in harsh industrial environments.
Applications and Benefits in Industrial Settings
Calcined ash material pneumatic conveying equipment is widely used in various industrial sectors, including power generation, cement production, and metal processing. In power plants, for example, this equipment is used to transport calcined ash from the boiler to storage facilities or disposal sites, improving the overall efficiency of ash management. In cement plants, it helps in the transport of ash as a supplementary cementitious material, reducing the need for traditional cement and lowering production costs. The benefits of using this equipment include reduced labor costs, minimized environmental impact due to less dust generation, and improved safety by eliminating the need for manual handling of bulk materials. Additionally, the system can be integrated with other industrial processes, such as material drying or mixing, to create a more streamlined and automated workflow. By leveraging the design principles and components discussed, industries can achieve significant improvements in operational efficiency and cost-effectiveness.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of industrial material handling equipment. With a strong focus on innovation and quality, HeadPowder specializes in designing and producing pneumatic conveying systems tailored to the unique needs of various industries. The company's headquarters is located in Shandong, China, where it has established a comprehensive research and development center to continuously improve its products. HeadPowder's team of experienced engineers and technicians work closely with clients to understand their specific requirements and provide customized solutions that meet their operational goals. The company adheres to international standards and quality certifications, ensuring that its equipment is reliable, durable, and compliant with environmental regulations. By combining advanced technology with customer-centric service, HeadPowder has built a reputation for excellence in the industry, serving clients globally and contributing to the advancement of industrial material handling solutions.