

Chocolate Powder Pneumatic Conveying: What It Is and Its Design Principles
Chocolate powder pneumatic conveying is a specialized method used in the food industry to transport chocolate powders and other fine particulate materials. This technology is crucial for maintaining the quality and integrity of chocolate powders, which are sensitive to moisture, temperature, and physical handling. The process involves using compressed air or other gases to move the powder through a pipeline system, ensuring a clean, efficient, and hygienic transfer from the source to the destination. Such systems are often designed and manufactured by companies like Shandong HeadPowder Engineering Co., Ltd., a leading provider of engineering solutions for the food processing industry.
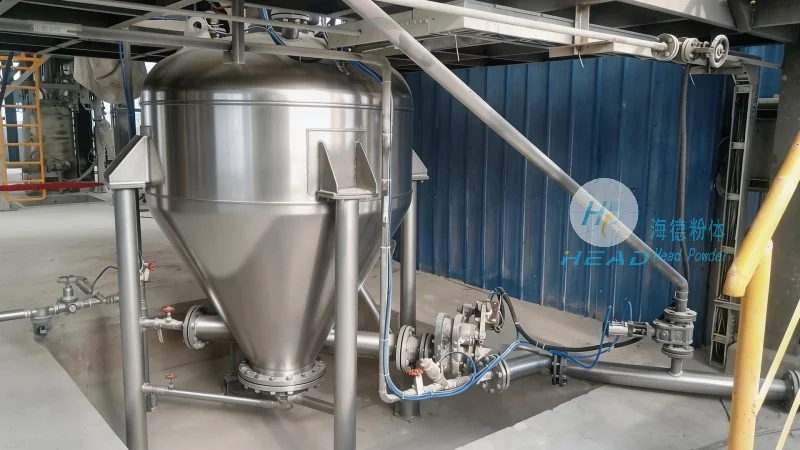
Understanding Chocolate Powder Pneumatic Conveying
At its core, chocolate powder pneumatic conveying is a system that utilizes air pressure to transport dry powders like chocolate powder. Unlike traditional mechanical conveyors, this method avoids direct contact with moving parts, reducing the risk of contamination and product degradation. The system typically consists of a hopper, a venturi or other air delivery device, and a receiver, all connected by a network of pipes. Compressed air is introduced into the system, creating a low-pressure zone that draws the powder into the air stream and propels it through the pipeline.
The Design Principles of Chocolate Powder Pneumatic Conveying
The design of a chocolate powder pneumatic conveying system is tailored to the specific characteristics of the powder, such as its particle size, density, and flowability. Key design principles include: ensuring adequate air velocity to prevent powder settling or blockages, maintaining proper pressure differentials to achieve efficient transport, and incorporating features like cyclone separators or filters to separate the powder from the air stream. The system must also adhere to strict hygiene standards, as chocolate powders are often used in food applications where contamination is unacceptable. This includes using stainless steel components, smooth surfaces, and easy-to-clean designs.
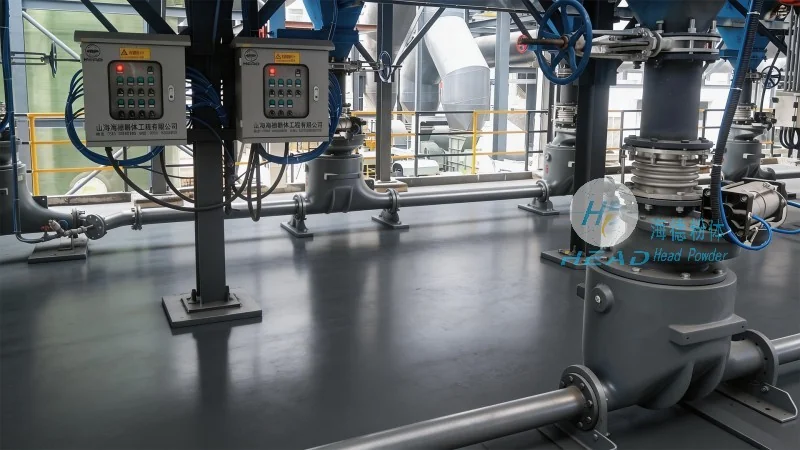
Components and Functionality
The main components of a chocolate powder pneumatic conveying system include the material hopper, the air supply unit, the conveying line, and the product receiver. The hopper is designed to hold the chocolate powder and provide a consistent feed to the system. The air supply unit, usually a compressor, generates the necessary pressure to move the powder. The conveying line, made of materials like stainless steel or food-grade plastic, transports the powder and air mixture. The receiver, often a storage tank or processing vessel, collects the powder after it has been separated from the air.
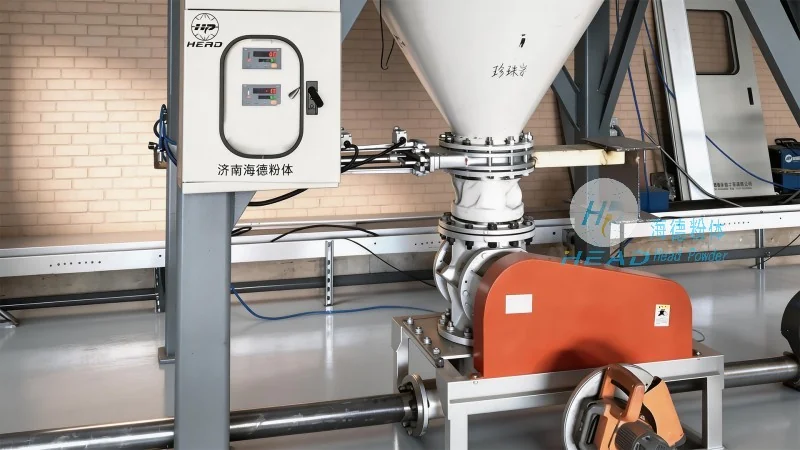
Advantages of Chocolate Powder Pneumatic Conveying
Compared to traditional conveyor systems, chocolate powder pneumatic conveying offers several advantages. It provides a hygienic and dust-free transfer, which is essential for food-grade products. The system is also flexible, allowing for changes in flow rate and direction without significant modifications. Additionally, it can handle a wide range of powder characteristics, from fine to coarse particles, and can transport materials over long distances with minimal energy consumption. The lack of moving parts also reduces maintenance requirements and downtime.
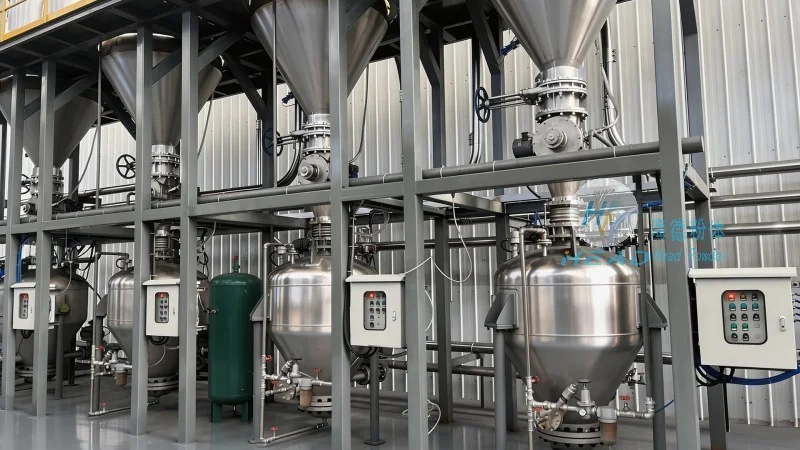
Applications in the Chocolate Industry
Chocolate powder pneumatic conveying is widely used in various stages of chocolate production and processing. It is commonly employed in the transfer of cocoa powder, chocolate chips, and other fine ingredients from storage silos to production lines. The system is also used in the packaging process, where it helps move finished chocolate powders into bags or containers. In addition, it can be integrated into automated production lines, improving efficiency and reducing labor costs.
Key Considerations for Design and Implementation
When designing a chocolate powder pneumatic conveying system, several factors must be considered to ensure optimal performance and product quality. These include the powder's properties, such as its moisture content and flowability, the required conveying distance and capacity, and the available space for the system. It is also important to consider the environmental impact, as the system must be designed to minimize air emissions and noise. Additionally, the system should be easy to clean and maintain, as regular cleaning is essential to prevent cross-contamination and product spoilage.