When considering the components of a corn pneumatic conveying system, it's essential to understand the key elements that enable efficient and reliable material transport. This system, widely used in agricultural and industrial applications, relies on a combination of specialized equipment and engineering principles to move corn from one location to another. The following sections outline the primary components that constitute a typical corn pneumatic conveying setup, providing insights into how each part contributes to the overall functionality.
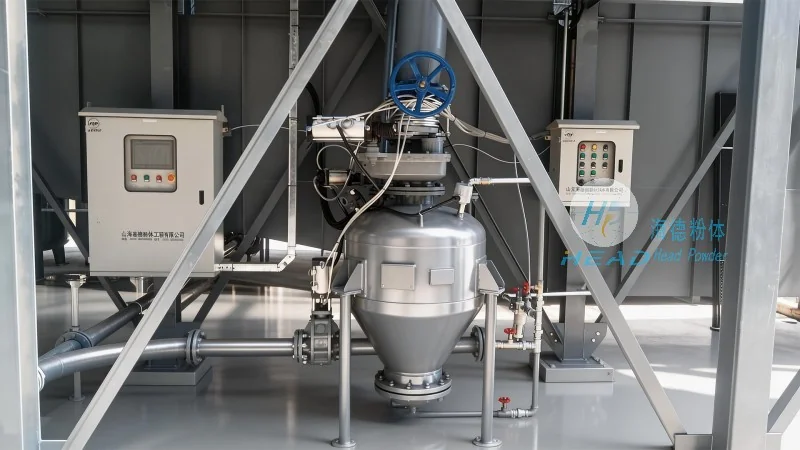
Core Components of Corn Pneumatic Conveying Systems
The foundation of any corn pneumatic conveying system lies in its core components, which work in tandem to ensure smooth material handling. These components include the hopper, conveyor line, and receiving vessel, each playing a critical role in the process. The hopper serves as the initial storage and feeding unit, where corn is loaded and prepared for transport. It is typically designed with a sloped bottom to facilitate the flow of material into the conveyor line. The conveyor line itself is the heart of the system, responsible for transporting the corn through the pipeline using air pressure. This line can be made of various materials, such as stainless steel or plastic, depending on the specific requirements of the application. The receiving vessel, located at the end of the conveyor line, collects the corn once it has been transported to its destination. This component is often equipped with a discharge mechanism to allow for easy unloading.
Compressors and Air Handling Equipment
A crucial part of corn pneumatic conveying is the compressor and associated air handling equipment. These components generate the necessary air pressure to move the corn through the system. The compressor can be either positive displacement or centrifugal, with positive displacement types being more common for low to medium pressure applications. The air handling equipment includes filters, regulators, and moisture separators, which ensure that the air used for conveying is clean and free from contaminants. This is vital to prevent clogging and maintain the efficiency of the system. The compressor's capacity and pressure rating must be matched to the system's requirements, as an underpowered or incorrectly sized unit can lead to reduced conveying efficiency or system failure.
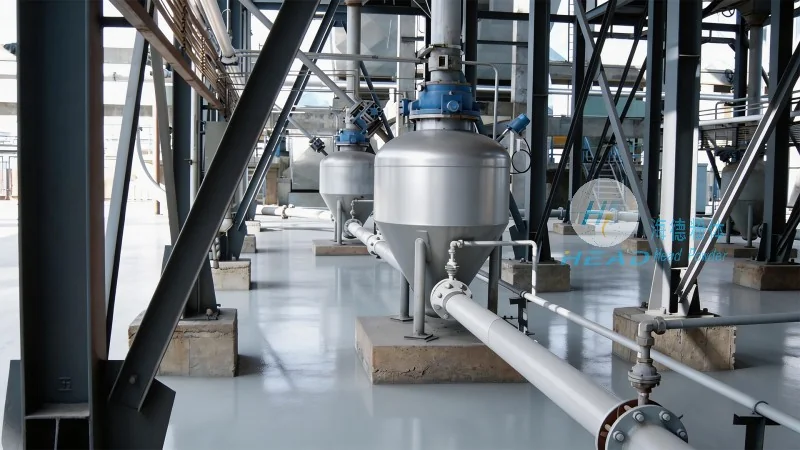
Control Systems and Sensors
Modern corn pneumatic conveying systems incorporate advanced control systems and sensors to monitor and regulate the operation. These systems help maintain consistent performance and prevent issues such as blockages or overpressure. The control panel typically includes switches, valves, and indicators that allow operators to manage the system's functions. Sensors are used to detect the level of material in the hopper and receiving vessel, as well as to monitor air pressure and flow rates. This data is then used to adjust the system's operation in real-time, ensuring optimal performance. For example, if the hopper level is low, the system can automatically adjust the feed rate to prevent overloading the conveyor line. Similarly, if the air pressure drops, the system can increase the compressor output to maintain the required flow.
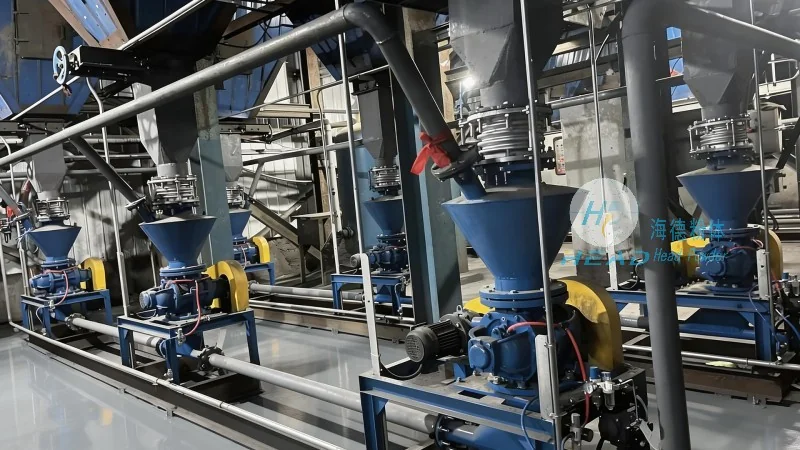
Accessories and Ancillary Equipment
Additional components such as rotary valves, and dust collectors are integral to the corn pneumatic conveying system. Rotary valves are used to control the flow of corn from the hopper into the conveyor line, ensuring a consistent feed rate. They are typically equipped with a sealing mechanism to prevent air leakage and maintain the system's pressure. Dust collectors are essential for maintaining a clean and safe working environment, as they capture any dust or particles generated during the conveying process. These collectors are often equipped with filters that can be cleaned or replaced to maintain their efficiency. Other accessories may include check valves, which prevent backflow of material or air, and pressure relief valves, which protect the system from overpressure conditions.
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., a leading provider of pneumatic conveying solutions, specializes in designing and manufacturing systems tailored to the needs of corn processing industries. With a focus on quality and innovation, the company has developed a range of components and systems that enhance the efficiency and reliability of corn handling operations. HeadPowder's expertise in material handling technology ensures that their products meet the highest standards of performance and durability. The company's commitment to customer satisfaction is reflected in their comprehensive support services, including installation, maintenance, and technical assistance. Based in China, Shandong HeadPowder Engineering Co., Ltd. serves clients globally, providing customized solutions that address the unique challenges of corn pneumatic conveying in various applications.




