HeadPowder, a leading engineering firm based in Shandong, China, specializes in the design and implementation of pneumatic conveying systems for various industrial applications, including the efficient handling of sulfammonium materials. This article delves into the fundamental principles behind sulfammonium pneumatic conveying and highlights the key characteristics of its operational scenarios.
Understanding the Pneumatic Conveying Principle for Sulfammonium
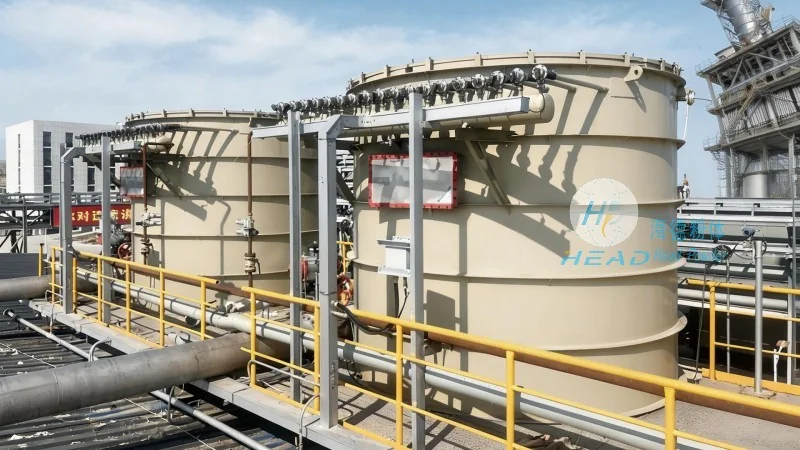
The core of sulfammonium pneumatic conveying lies in the use of air or gas to transport solid particles through a pipeline. This method, known as pneumatic conveying, operates by creating a pressure differential that propels the material along the system. For sulfammonium, a common fertilizer, the process involves several critical components and mechanisms. The system typically includes a hopper to store the material, a blower or compressor to generate the necessary airflow, and a pipeline network that guides the material from the source to the destination. The air velocity within the pipeline is a crucial factor; it must be sufficient to lift and transport the particles without causing excessive wear or degradation of the material. HeadPowder engineers meticulously calculate the air velocity and pressure requirements based on the specific properties of sulfammonium, such as its particle size, density, and flow characteristics. By optimizing these parameters, the system ensures reliable and efficient material transport, minimizing downtime and operational costs.
Key Characteristics of Sulfammonium Pneumatic Conveying Work Scenarios
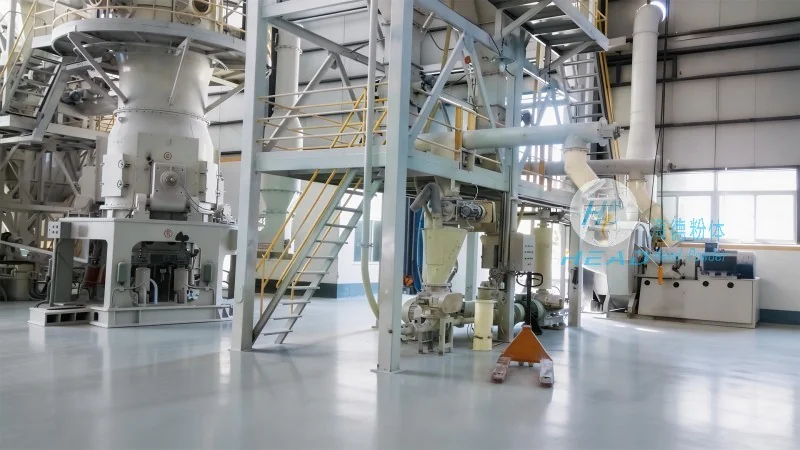
The operational scenarios for sulfammonium pneumatic conveying vary across different industrial settings, each presenting unique challenges and requirements. In fertilizer production facilities, for instance, the system is often integrated into large-scale manufacturing processes where sulfammonium is produced and then transported to storage silos or packaging lines. The key characteristics of such scenarios include high throughput rates, continuous operation, and the need for precise control over material flow. HeadPowder's expertise in customizing systems to meet these demands ensures that the conveying process is seamless and meets production targets. Another common scenario is in chemical processing plants, where sulfammonium may be used as an intermediate or raw material in various chemical reactions. Here, the system must handle potentially abrasive or corrosive materials, requiring specialized equipment like wear-resistant pipelines and valves. The work scenarios also vary in terms of the distance and layout of the conveying system. Some applications involve short-distance transport within a single facility, while others require long-distance conveying over several kilometers. HeadPowder's engineers design flexible and scalable systems that can adapt to these varying distances and layouts, ensuring optimal performance regardless of the operational scale.
Benefits and Advantages of Sulfammonium Pneumatic Conveying
Implementing pneumatic conveying systems for sulfammonium offers several significant benefits that enhance operational efficiency and safety. One of the primary advantages is the ability to handle materials in a closed system, which minimizes dust emissions and protects the environment. This is particularly important for sulfammonium, a fine powder that can be hazardous if released into the air. The closed system also prevents contamination from external sources, maintaining the purity of the material. Another key benefit is the reduction in labor costs and manual handling. By automating the material transport process, HeadPowder's systems reduce the need for manual loading and unloading, which not only improves safety but also increases productivity. Additionally, pneumatic conveying systems are highly flexible and can be easily integrated with existing production lines. This adaptability allows facilities to upgrade or expand their operations without major disruptions. The energy efficiency of these systems is also a notable advantage. Compared to traditional methods like belt conveyors or bucket elevators, pneumatic conveying can be more energy-efficient, especially for short-distance or high-volume transport. HeadPowder's optimization of air flow and system design ensures that energy consumption is minimized while maintaining optimal performance.
HeadPowder's Role in Sulfammonium Pneumatic Conveying Solutions
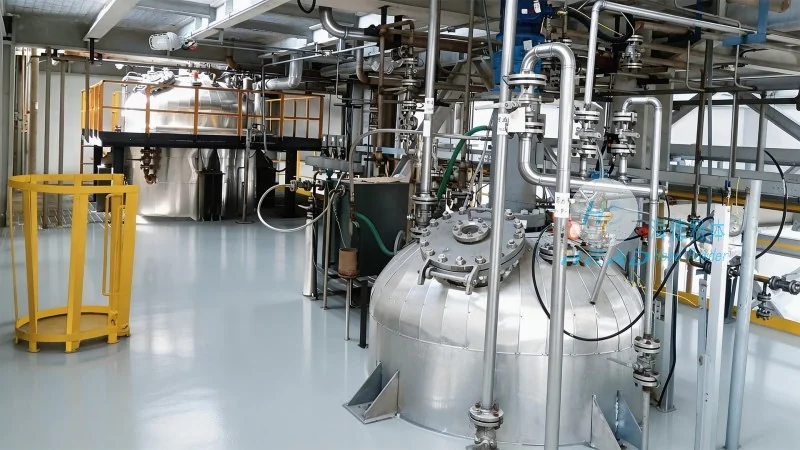
As a trusted partner in the engineering and manufacturing sector, HeadPowder provides comprehensive solutions for sulfammonium pneumatic conveying. The company's team of experienced engineers and technicians works closely with clients to understand their specific needs and design customized systems that meet their operational requirements. From initial consultation and system design to installation and commissioning, HeadPowder offers end-to-end support to ensure successful implementation. The company's expertise in material handling and process engineering allows it to address the unique challenges associated with sulfammonium, such as its hygroscopic nature and potential for caking. By incorporating advanced technologies and materials, HeadPowder's systems are designed to handle these challenges effectively, ensuring reliable and consistent performance. The company also provides ongoing maintenance and support services to keep the systems operating at peak efficiency. This commitment to quality and customer satisfaction has made HeadPowder a preferred choice for many industrial facilities seeking reliable sulfammonium conveying solutions.




