HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced powder explosive conveying equipment. This article explores the fundamental principles behind these systems and highlights their key applications across various industrial settings.
The Core Principles of Powder Explosive Conveying
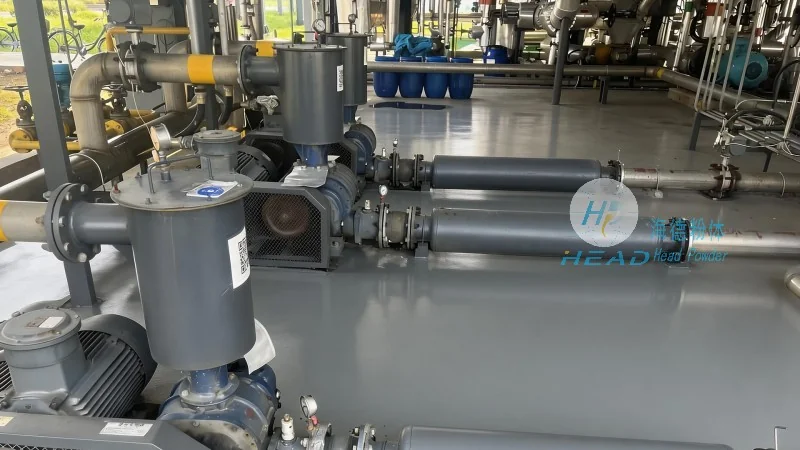
Powder explosive conveying systems are engineered to safely and efficiently transport granular or powdery materials, particularly those with explosive potential. The primary goal is to ensure stable, controlled movement while minimizing the risk of ignition or explosion. These systems typically operate on the principle of creating a sealed, inert environment that prevents the introduction of oxygen or other ignition sources. Key components include a hopper for material storage, a conveyor mechanism (such as pneumatic or mechanical), and a control system that regulates pressure and flow. The design emphasizes safety protocols, such as explosion-proof seals and pressure relief valves, to comply with industry standards like ATEX or NFPA. By maintaining a consistent flow and preventing material buildup, the system ensures reliable performance in high-risk environments. The engineering approach also considers the physical properties of the material, including particle size distribution, moisture content, and density, to optimize the conveying process and prevent issues like clogging or segregation.
Working Scene Characteristics and Applications
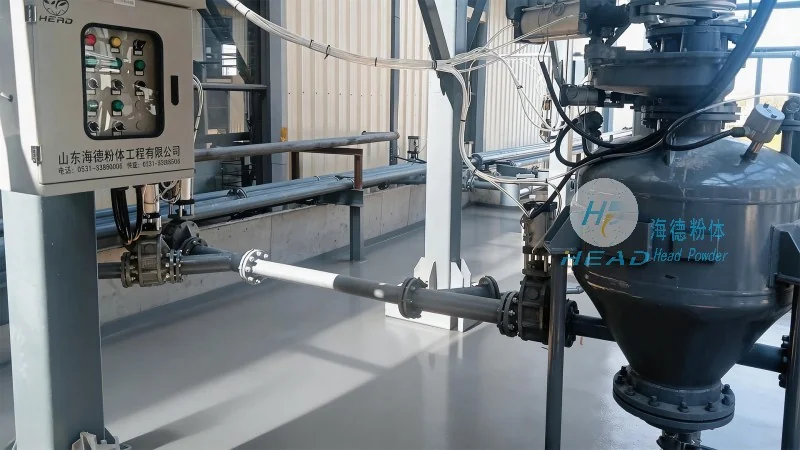
The working scene characteristics of powder explosive conveyors are tailored to meet the demands of industries where explosive powders are handled. These systems are commonly used in the production of fireworks, pyrotechnics, and other explosive materials. The key characteristics include high-precision control over material flow, low maintenance requirements, and the ability to handle a wide range of particle sizes and densities. In fireworks manufacturing, for example, the system ensures that powders are delivered to mixing and pressing stages without contamination or degradation. In pyrotechnic production, the conveyor maintains a consistent supply of oxidizers and fuels, which is critical for the stability of the final product. Additionally, the systems are designed for easy integration into existing production lines, with modular components that allow for scalability and customization. The working environment is typically controlled, with temperature and humidity monitoring to prevent material caking or moisture absorption, which could affect the explosive properties. The systems also feature real-time monitoring capabilities, allowing operators to track flow rates and detect any anomalies that may indicate a potential issue, ensuring continuous and safe operation.
About HeadPowder Engineering Co., Ltd.
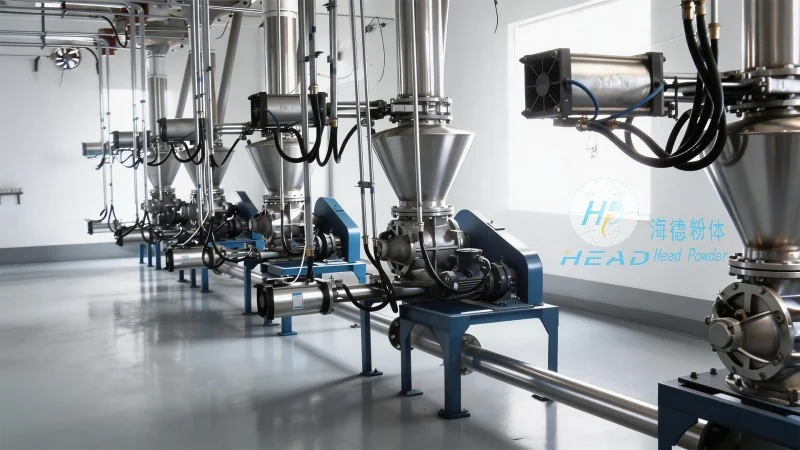
HeadPowder Engineering Co., Ltd. is a professional enterprise dedicated to the research, development, and manufacturing of specialized conveying equipment for hazardous materials. With a strong focus on safety and innovation, the company has established itself as a trusted partner in the industry. Based in Shandong, China, HeadPowder leverages advanced engineering techniques and rigorous quality control processes to deliver reliable solutions for clients worldwide. The company's commitment to excellence is reflected in its adherence to international safety standards and continuous improvement of product performance. By combining technical expertise with customer-centric service, HeadPowder ensures that its powder explosive conveying systems meet the unique needs of each application, providing long-term value and operational efficiency. The company's team of experienced engineers and technicians work closely with clients to understand their specific requirements, offering tailored solutions that enhance productivity while maintaining the highest safety standards. HeadPowder's products are designed to withstand the harsh conditions of explosive material handling, with durable materials and robust construction that ensure longevity and minimal downtime.




