Foam powder conveyors represent a sophisticated solution in material handling, particularly for industries dealing with fine powders. The technology behind these systems is centered on the principle of using foam as a carrier medium to transport particulate materials. By generating a stable foam structure, the conveyor can effectively move powders through pipelines or open channels while minimizing dust generation and improving overall material integrity. This approach is especially valuable in environments where air quality and product purity are critical concerns.
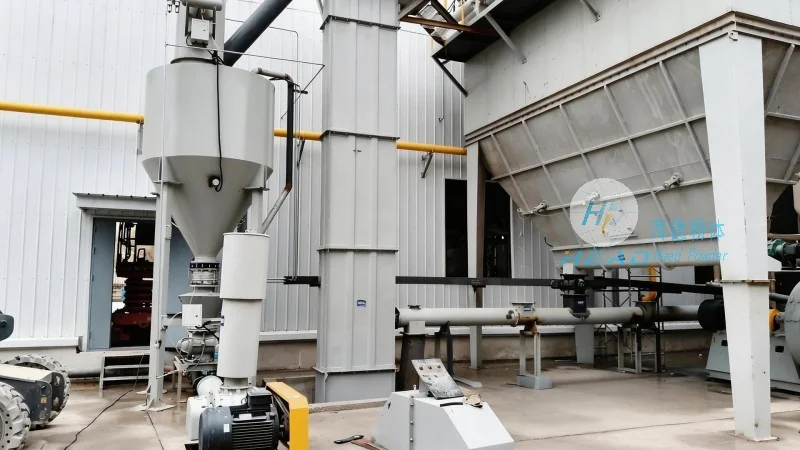
Core Working Principle of Foam Powder Conveyors
At the heart of foam powder conveyors is the interaction between the foam and the powder particles. The system typically operates by mixing a liquid (such as water or a specialized solution) with a foaming agent under controlled conditions. This mixture is then introduced into a pump or conveyor system, where it is aerated to create a stable foam. The foam, with its low density and high surface area, envelops the powder particles, forming a cohesive slurry. As the foam flows through the conveyor, it transports the powder while maintaining the particles in a suspended state. The key to efficient operation lies in the balance of foam stability, particle size, and flow rate. Properly adjusted, the foam can handle a wide range of powder types, from fine pharmaceutical powders to bulk industrial materials, without causing clogging or degradation of the product.
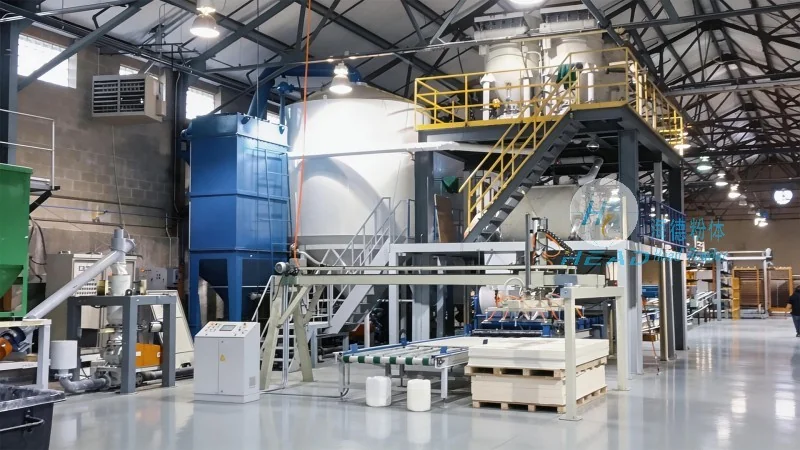
Key Working Characteristics and Application Scenarios
One of the most notable characteristics of foam powder conveyors is their ability to deliver dust-free material transport. Unlike traditional pneumatic or mechanical conveyors, which often generate significant airborne dust, foam conveyors keep the powder contained within the foam matrix. This makes them ideal for applications in pharmaceutical manufacturing, food processing, and chemical processing where product contamination and air quality regulations are paramount. Additionally, the system offers flexibility in handling different powder densities and moisture levels. For instance, in the pharmaceutical industry, foam conveyors can transport sensitive drugs without compromising their sterility or quality. In the food sector, they can handle powders like flour or cocoa without introducing foreign particles or moisture. The technology also excels in scenarios requiring long-distance or vertical transport, as the foam's viscosity and stability allow for consistent flow even over extended or elevated routes.
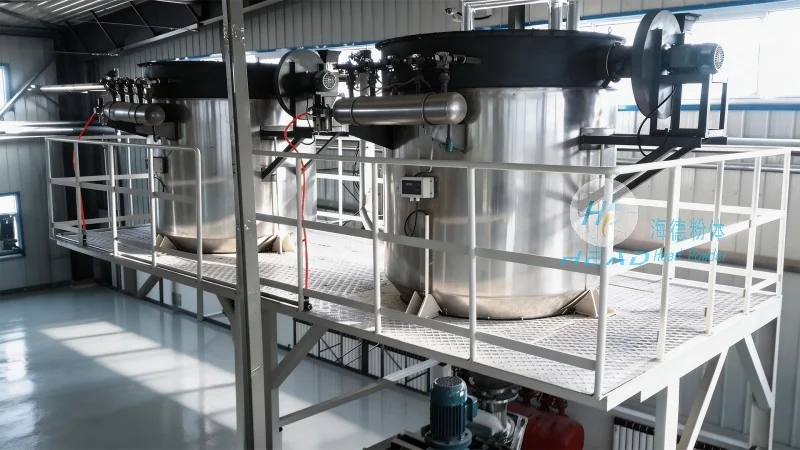
HeadPowder: Leading Manufacturer of Foam Powder Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a prominent manufacturer specializing in advanced material handling equipment, including foam powder conveyors. Based in Shandong, China, HeadPowder leverages decades of engineering expertise to design and produce conveyors that meet the rigorous demands of modern industrial applications. The company's products are engineered with precision to ensure optimal foam stability, efficient power consumption, and minimal maintenance requirements. HeadPowder's commitment to innovation is evident in their ability to customize systems for specific industry needs, whether it's for high-purity pharmaceuticals, food-grade powders, or bulk chemical materials. By integrating cutting-edge technology with practical design, HeadPowder delivers reliable and efficient foam powder conveying solutions that enhance productivity while adhering to safety and environmental standards.




