Corn pneumatic conveying is a critical technology in agricultural processing and material handling, designed to transport corn kernels efficiently from one location to another using air pressure. This method offers several advantages over traditional mechanical conveyors, including reduced equipment wear, lower maintenance costs, and the ability to handle a wide range of corn types and conditions. The core principle involves creating a pressure differential that propels corn through a pipeline using air, making it a versatile solution for both small-scale and large-scale operations.
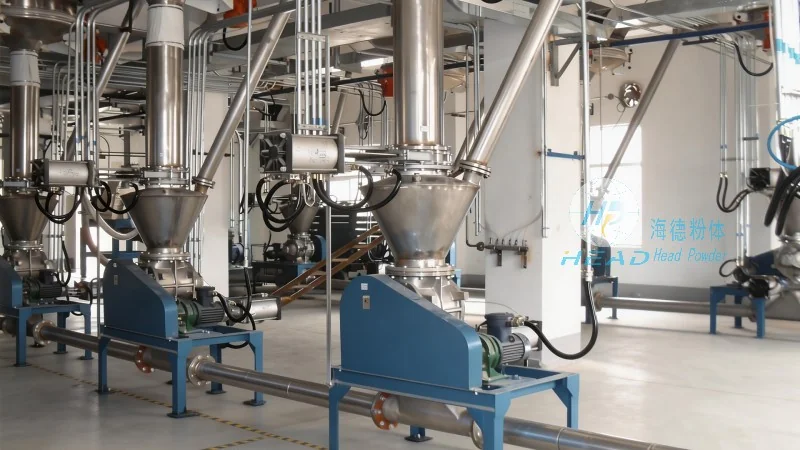
The Fundamental Principles of Pneumatic Conveying for Corn
The operation of corn pneumatic conveying systems relies on the principles of fluid dynamics and air movement. At its essence, the system uses a fan or blower to generate airflow, which then carries corn particles through a sealed pipeline. The key components include a hopper for storing corn, a conveyor line (often made of metal or flexible tubing), and a discharge point where the corn is released. The pressure created by the fan can be either positive (pressure) or negative (vacuum), with positive pressure being more common for corn applications due to its ability to handle larger volumes and prevent dust accumulation. The velocity of the air and the size of the corn kernels are carefully balanced to ensure efficient transport without causing damage to the kernels or excessive wear on the system components. This balance is crucial for maintaining the quality of the corn and the longevity of the equipment.
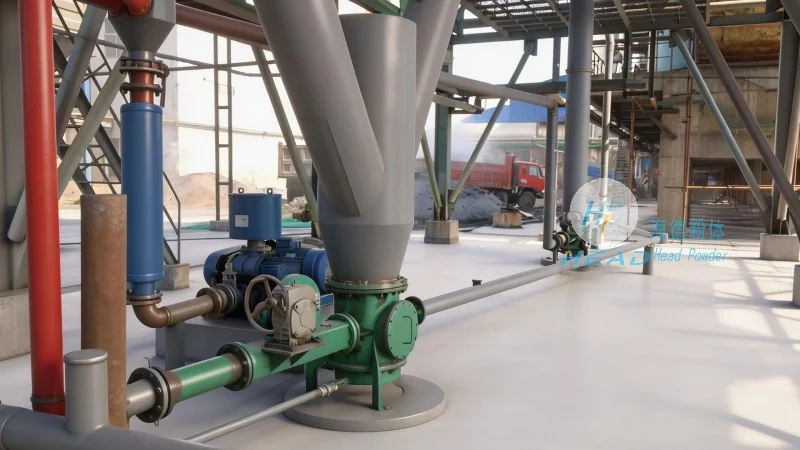
Key Working Scene Characteristics of Corn Pneumatic Conveying
When applied in real-world scenarios, corn pneumatic conveying systems exhibit distinct characteristics that make them suitable for various agricultural and industrial settings. One primary characteristic is their ability to handle both dry and moist corn, adapting to different moisture levels without compromising performance. This flexibility is particularly valuable in regions with varying climatic conditions or during different stages of the corn harvest season. Another important characteristic is the system's compact design, which allows for installation in confined spaces, such as on farms or in processing facilities with limited floor space. The sealed pipeline design also helps in maintaining the quality of the corn by preventing contamination from external elements, such as dust or pests. Additionally, the system's low noise operation makes it suitable for use in areas where noise restrictions are a concern, such as near residential zones or during nighttime operations. These characteristics collectively contribute to the widespread adoption of corn pneumatic conveying in modern agricultural operations.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of pneumatic conveying systems tailored for agricultural applications. With a strong focus on innovation and quality, HeadPowder has established itself as a trusted partner in the corn processing industry. The company's products are designed to meet the specific needs of corn handling, ensuring efficient and reliable transport while maintaining the integrity of the corn kernels. HeadPowder's expertise lies in customizing systems to suit different operational requirements, from small-scale farm operations to large-scale industrial processing plants. The company's commitment to customer satisfaction and technical support has earned it a reputation for delivering durable and efficient solutions that enhance productivity and reduce operational costs for its clients.
Real-World Applications and Operational Scenarios
Corn pneumatic conveying systems are widely used in various operational scenarios within the corn industry. For instance, in grain storage facilities, these systems are employed to transfer corn from storage silos to processing lines, ensuring a continuous flow of raw material. In corn milling operations, the system can transport corn from the cleaning and drying stages to the grinding and milling equipment, maintaining a consistent supply of material. Additionally, in feed manufacturing plants, corn pneumatic conveyors are used to move corn from storage bins to mixing and packaging units, supporting the production of animal feed. The adaptability of these systems allows them to integrate seamlessly with existing infrastructure, minimizing the need for extensive modifications to existing facilities. This integration capability is a significant advantage for businesses looking to upgrade their corn handling processes without disrupting their current operations.
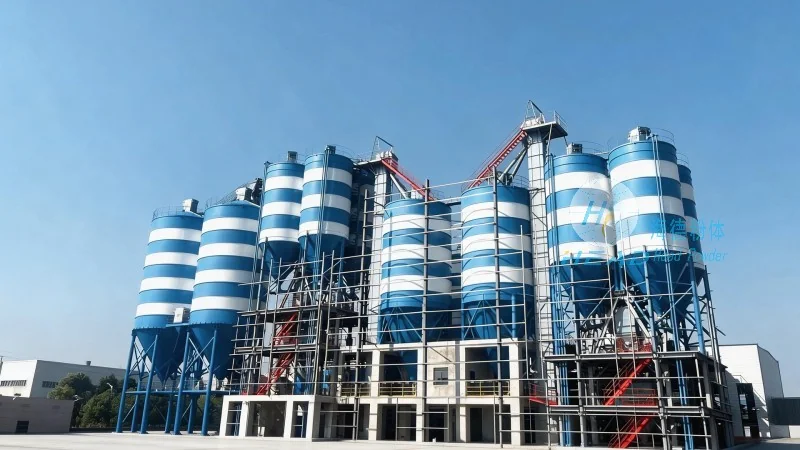
Conclusion: The Advantages of Corn Pneumatic Conveying
Overall, corn pneumatic conveying represents a highly effective and efficient method for transporting corn in agricultural and industrial settings. By leveraging the principles of air pressure and fluid dynamics, these systems offer numerous benefits, including reduced wear and tear, lower maintenance costs, and the ability to handle a wide range of corn conditions. The working scene characteristics, such as adaptability to different moisture levels and compact design, make them suitable for diverse applications. With the expertise of companies like Shandong HeadPowder Engineering Co., Ltd., businesses can access reliable and customized solutions that enhance their operational efficiency and product quality. As the demand for efficient corn handling continues to grow, pneumatic conveying systems remain a vital technology in modern agricultural operations.




