Working Principle and Features of Dust-Free Bag Opening Pneumatic Conveying System Equipment
Release time:2026-09-17 07:17:19
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Zhang manager
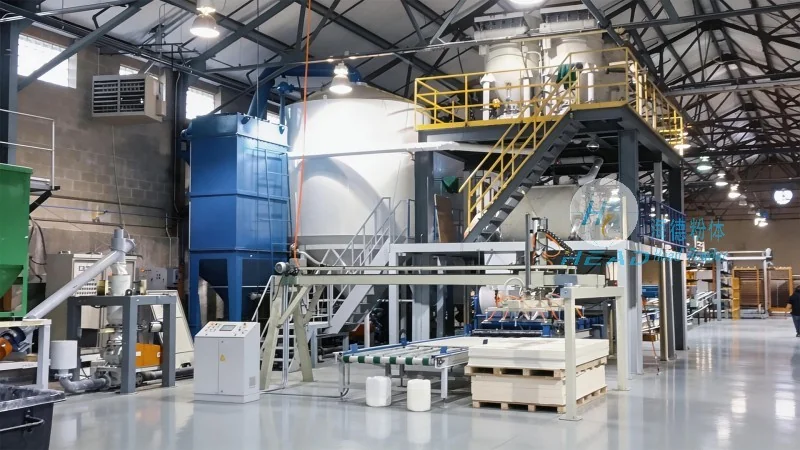
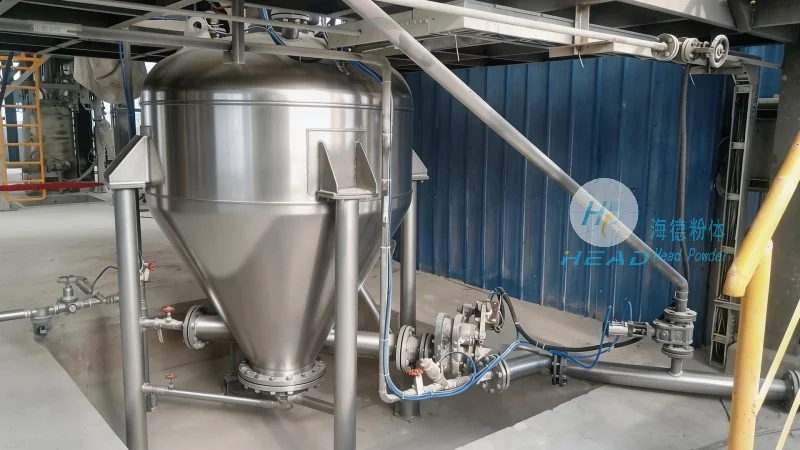
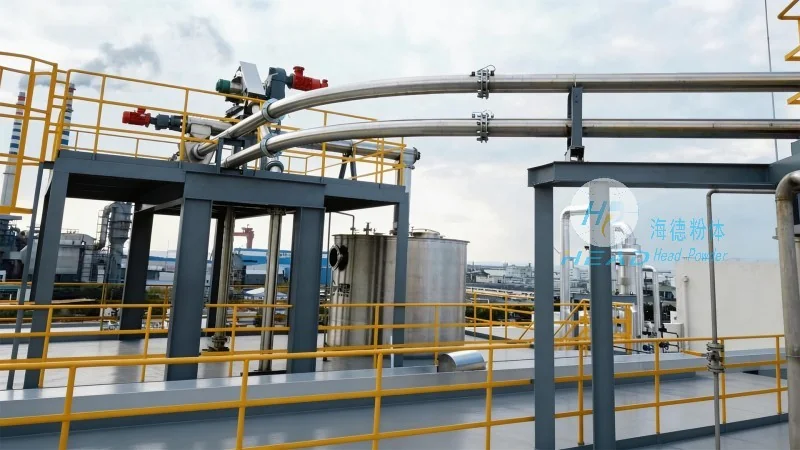
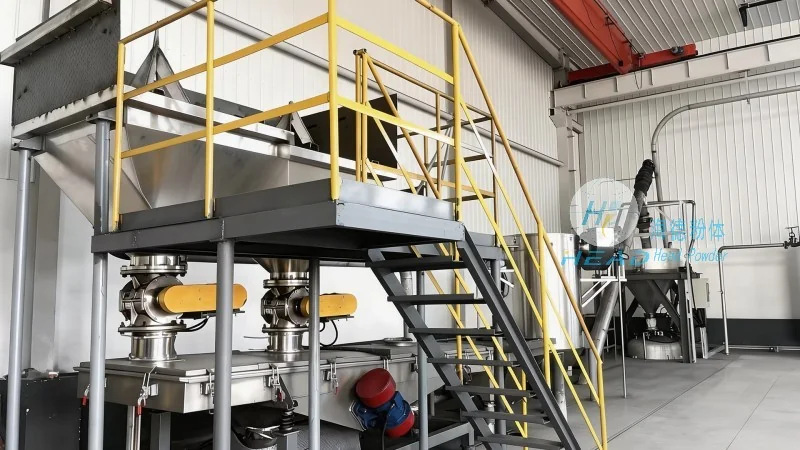
The dust-free bag opening pneumatic conveying system is a specialized equipment designed to handle bulk materials from sealed bags in a clean environment. Its working principle centers on the use of compressed air to create a negative pressure or positive pressure flow, which draws the material from the bag and transports it to the processing or storage area. The system typically includes components such as a bag opening device, a vacuum or pressure conveyor, a filter system, and a material collection hopper. The bag opening mechanism may involve mechanical cutting or air knives to safely open the bag without generating dust. Once the bag is opened, the material is drawn into the conveyor by the air flow, which is then filtered to remove any fine particles before being directed to the next stage of the process. This method ensures that the material is handled in a controlled manner, minimizing contamination and maintaining product purity.
Key Features of the Dust-Free Bag Opening Pneumatic Conveying System
The system offers several distinct advantages that make it suitable for industries requiring high standards of cleanliness and efficiency. Firstly, its dust-free operation is crucial for maintaining a clean working environment, especially in pharmaceutical, food, and chemical processing sectors where contamination control is paramount. The enclosed system design prevents dust from escaping into the air, reducing the risk of product degradation and health hazards. Secondly, the system is highly efficient in material handling, capable of transporting large volumes of bulk materials quickly and with minimal labor. The pneumatic conveying process allows for continuous operation, which can improve production throughput and reduce downtime. Additionally, the system is versatile, capable of handling a wide range of materials, including powders, granules, and fine particles, with adjustable conveying speeds and pressures to suit different material characteristics. Another key feature is the ease of integration with existing production lines, as the system can be customized to fit specific space constraints and operational requirements. The filter system is designed to capture and retain any fine particles, ensuring that the exhaust air is clean and compliant with environmental regulations.
Company Information and Background
HeadPowder, the manufacturer of this advanced system, is a leading company in the field of bulk material handling solutions. With its headquarters in Shandong, China, HeadPowder has established itself as a trusted provider of high-quality engineering equipment tailored to the needs of various industries. The company specializes in the design, manufacturing, and installation of pneumatic conveying systems, focusing on innovation and customer satisfaction. By leveraging years of experience and expertise, HeadPowder has developed systems that meet international standards for safety, efficiency, and environmental compliance. The company's commitment to quality is reflected in its use of durable materials and rigorous testing procedures, ensuring that each system performs reliably and consistently over its service life. HeadPowder's team of engineers and technicians work closely with clients to understand their specific requirements, providing tailored solutions that enhance operational performance and reduce costs.




