

What is a Carbon Black and Coal Powder Material Pneumatic Conveyor? What is Its Design Principle?
HeadPowder, a leading manufacturer based in Shandong, China, specializes in providing advanced pneumatic conveying systems tailored for handling carbon black and coal powder materials. These systems are engineered to efficiently transport fine powders over long distances with minimal operational issues, making them essential for various industrial applications.
Understanding the Core Function of Pneumatic Conveyors
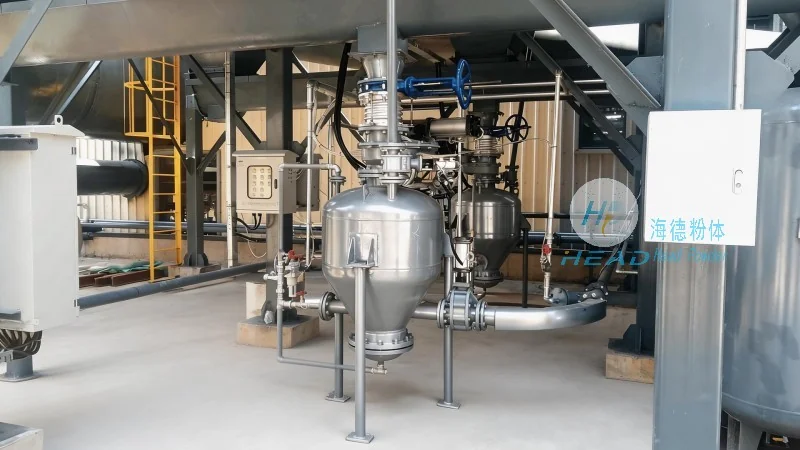
A pneumatic conveyor, as the name suggests, utilizes compressed air or gas to move bulk materials like carbon black and coal powder from one location to another. Unlike traditional mechanical conveyors, this method offers advantages such as reduced equipment wear, lower maintenance costs, and the ability to handle materials in a dust-free environment. The system typically consists of a hopper for material storage, a blower or compressor to generate airflow, and a pipeline network that transports the material to the destination point.
Design Principles Behind the Pneumatic Conveyor System
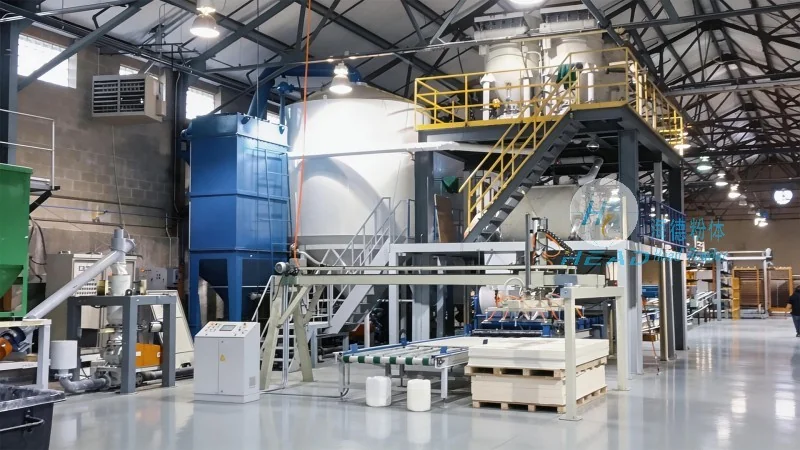
The design of a carbon black and coal powder pneumatic conveyor involves several critical principles to ensure optimal performance. First, the selection of appropriate air velocity is crucial. The velocity must be high enough to prevent material settling or clogging in the pipeline but low enough to avoid excessive pressure drop and energy consumption. Engineers calculate the required air velocity based on the material's density, particle size, and flow characteristics. Second, the system's pressure and flow rate are carefully balanced. The blower or compressor must generate sufficient pressure to overcome the resistance in the pipeline, including friction losses and elevation changes. This balance ensures consistent material flow without causing excessive wear on components. Third, the pipeline design is optimized for material transport. The diameter and length of the pipeline are determined based on the material's flow properties and the desired conveying capacity. Additionally, the use of bends, elbows, and other fittings is minimized to reduce pressure losses and maintain a smooth flow. Finally, the system incorporates safety features, such as pressure relief valves and dust collection systems, to protect against overpressure and dust emissions, ensuring compliance with industrial safety standards.
Key Components and Their Roles
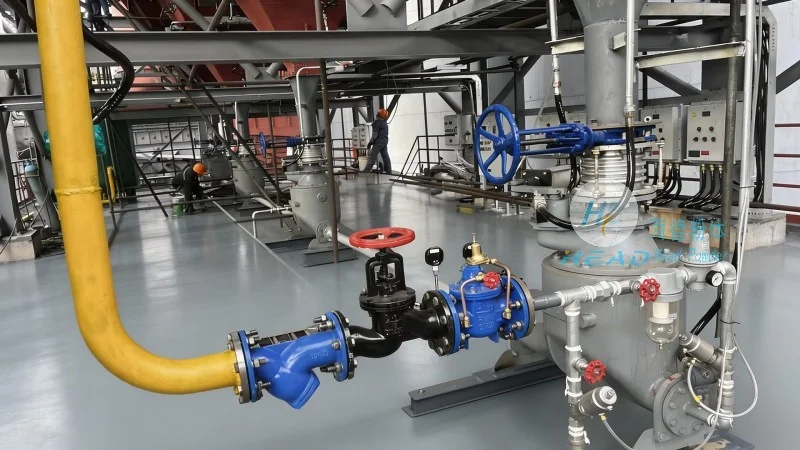
The pneumatic conveyor system for carbon black and coal powder consists of several key components, each playing a vital role in the overall operation. The hopper serves as the material storage unit, allowing for continuous feeding of the powder. It is equipped with a feeder, such as a rotary valve or a screw feeder, to control the flow rate of the material into the pipeline. The blower or compressor is the heart of the system, generating the necessary airflow to transport the material. It can be a positive displacement blower or a centrifugal compressor, depending on the system's requirements. The pipeline network connects the hopper to the destination point, with the main pipeline and branch lines designed to handle the material flow efficiently. The destination point, such as a silo or a processing unit, is equipped with a receiver or a discharge valve to collect the material. Additionally, the system may include a dust collection system to capture any airborne particles and prevent environmental contamination. Each component is carefully selected and sized to ensure the system operates efficiently and reliably.
Applications and Benefits in Industrial Settings
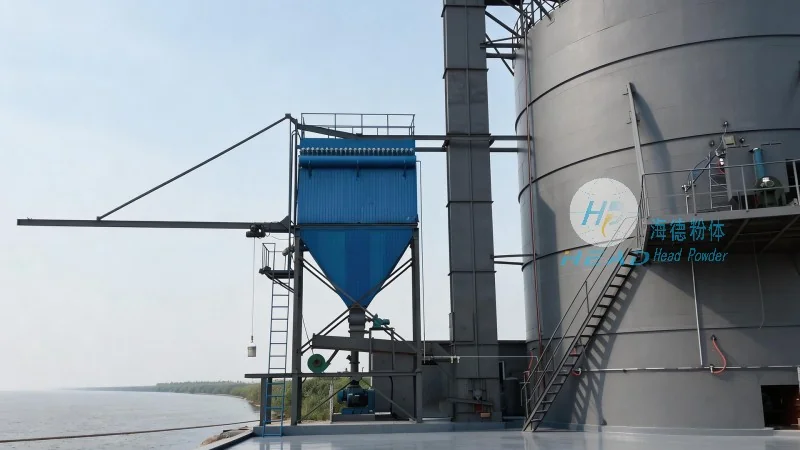
Carbon black and coal powder pneumatic conveyors are widely used in various industrial sectors, including chemical manufacturing, mining, and power generation. In the chemical industry, these systems are used to transport carbon black, a key raw material for rubber and plastic production, from storage silos to processing units. The ability to handle fine powders without generating dust makes the system ideal for maintaining a clean and safe working environment. In the mining industry, coal powder is transported from mines to processing plants or power stations, where it is used as fuel. The pneumatic conveyor system allows for the efficient and safe transport of coal powder over long distances, reducing the need for manual handling and minimizing the risk of accidents. In power generation, coal powder is conveyed from storage to the boiler, where it is burned to generate electricity. The system's ability to handle large volumes of material at high speeds makes it a cost-effective solution for power plants. The benefits of using a pneumatic conveyor for carbon black and coal powder include improved material handling efficiency, reduced labor costs, lower maintenance requirements, and enhanced safety. The system also helps to minimize environmental impact by reducing dust emissions and improving material containment.