For agricultural operations that rely on potassium-based fertilizers, efficient material handling is crucial for maintaining productivity and ensuring the quality of the final product. Potassium fertilizer material handling equipment is specifically designed to manage the storage, transfer, and distribution of these essential nutrients. Understanding the components and design principles behind such equipment is vital for optimizing farm operations and meeting the demands of modern agriculture.
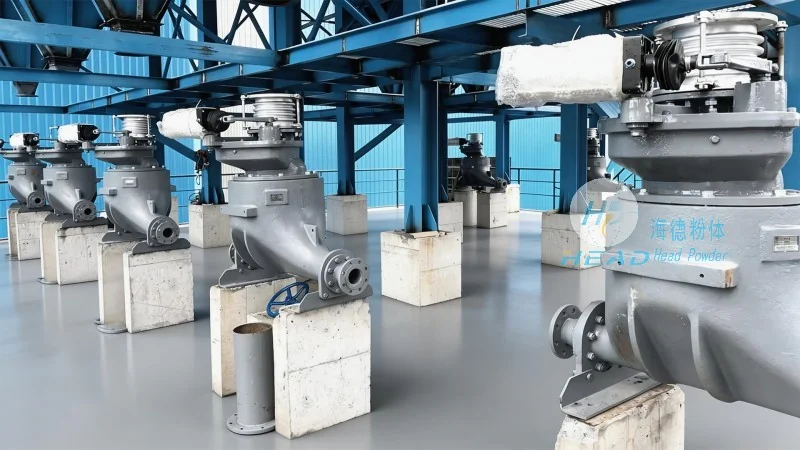
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the development and production of advanced material handling solutions for the fertilizer industry. With a strong commitment to innovation and quality, the company has established itself as a trusted partner for agricultural enterprises seeking reliable equipment for their potassium fertilizer processing needs. The company's headquarters and manufacturing facilities are located in Shandong, providing a strategic base for serving both domestic and international markets.
Design Principles of Potassium Fertilizer Material Handling Equipment
The design of potassium fertilizer material handling equipment is guided by several key principles to ensure safety, efficiency, and durability. First, the equipment must be constructed from materials that are resistant to corrosion and wear, as potassium fertilizers can be chemically aggressive. Stainless steel and specialized alloys are commonly used in the construction of hoppers, conveyors, and storage silos to withstand the harsh conditions of fertilizer handling. Second, the design emphasizes the need for minimal material degradation during transport. This involves using smooth surfaces and gentle conveying mechanisms to prevent clumping or breakdown of the fertilizer particles, which could affect nutrient distribution and application rates.
Third, the equipment is engineered for high throughput and reliability. Conveyor systems, such as belt conveyors or screw conveyors, are often integrated with the design to move large volumes of potassium fertilizer quickly and consistently. The use of variable speed drives allows operators to adjust the flow rate based on operational requirements, optimizing energy consumption and reducing downtime. Additionally, the equipment incorporates safety features, including overload protection and emergency stop mechanisms, to protect both personnel and machinery from potential hazards.
Key Components and Functional Aspects
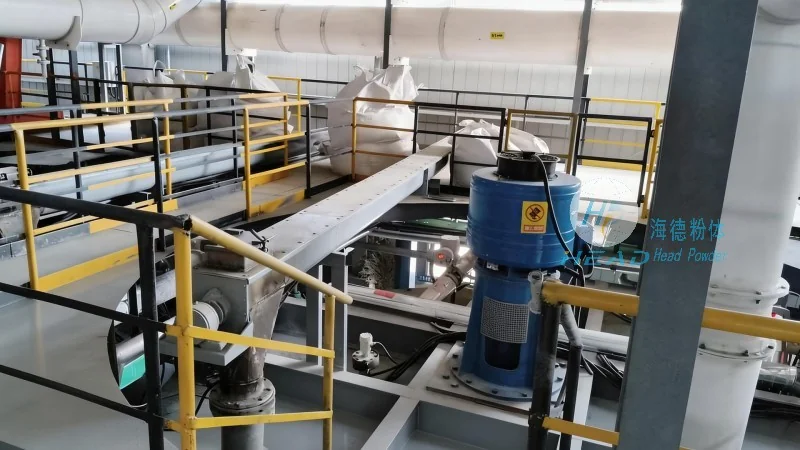
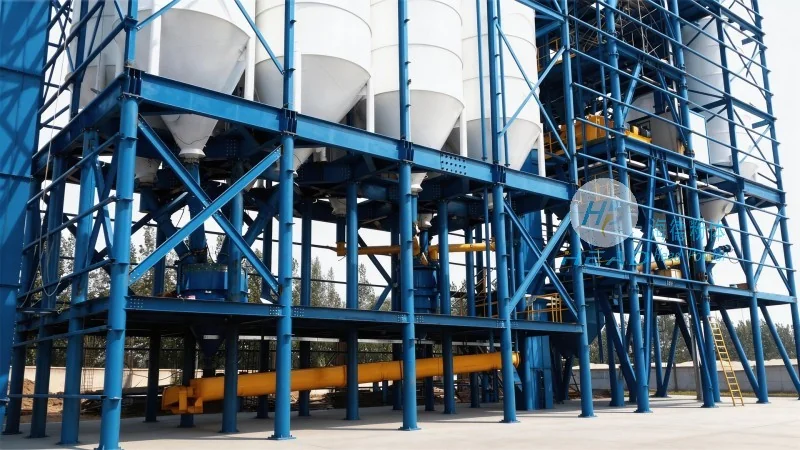
Typical potassium fertilizer material handling equipment includes several critical components that work in tandem to facilitate efficient operation. The storage silo is the primary unit for holding bulk quantities of fertilizer, often equipped with aeration systems to prevent moisture buildup and maintain product quality. From the silo, a feeder or discharge mechanism regulates the flow of fertilizer into the conveyor system. This component ensures a controlled and consistent feed rate, preventing overloading or underloading of the conveying equipment.
The conveyor system itself is a central element, responsible for transporting the fertilizer from the storage area to the application point or packaging facility. Belt conveyors are widely used due to their ability to handle large volumes and their low maintenance requirements. Screw conveyors are also common, particularly for vertical or inclined transport, as they can move material through vertical sections without the need for additional equipment. The design of the conveyor includes features like idler rollers and tensioning mechanisms to ensure smooth operation and prevent belt slippage or breakage.
Advantages and Applications
Investing in specialized potassium fertilizer material handling equipment offers several advantages for agricultural operations. Firstly, it enhances operational efficiency by reducing the time and labor required for manual handling of bulk fertilizer. Automated systems can process large quantities of material in a short period, allowing farmers and agricultural businesses to scale their operations without increasing labor costs. Secondly, the equipment improves product quality by minimizing the risk of contamination or degradation during transport. By maintaining the integrity of the fertilizer, the equipment ensures that the nutrients are delivered in their optimal form, leading to better crop yields and soil health.
Furthermore, the design of the equipment promotes safety in the workplace. By automating the handling process, the risk of accidents associated with manual lifting and moving of heavy fertilizer bags or bulk material is significantly reduced. The integration of safety features, such as emergency stops and overload protection, provides an additional layer of security for operators and equipment. This not only protects personnel but also reduces the likelihood of equipment damage or downtime, which can be costly for agricultural businesses.
Conclusion
Potassium fertilizer material handling equipment is a critical component of modern agricultural operations, designed to efficiently manage the storage, transfer, and distribution of essential nutrients. The design principles behind such equipment prioritize durability, efficiency, and safety, ensuring that the fertilizer is handled with minimal degradation and maximum effectiveness. Companies like Shandong HeadPowder Engineering Co., Ltd. play a vital role in providing these advanced solutions, supporting the agricultural industry in meeting the growing demand for potassium-based fertilizers while maintaining high standards of productivity and quality.




