Exploring the Inert Gas Circulating Pneumatic Conveying System and Its Design Fundamentals
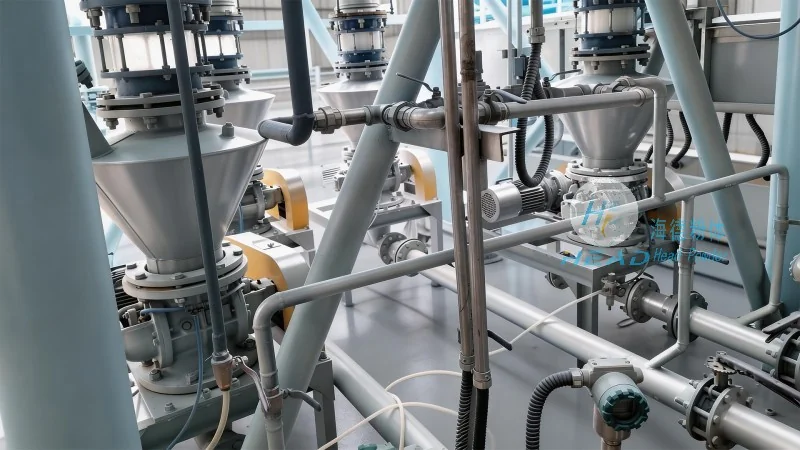
Overview of Inert Gas Circulating Pneumatic Conveying Systems
An inert gas circulating pneumatic conveying system is a sophisticated industrial solution designed to transport bulk materials through a closed-loop system using an inert gas as the primary conveying medium. This technology is particularly valuable in industries where maintaining a controlled, contamination-free environment is non-negotiable, such as pharmaceuticals, food processing, and specialty chemicals. The system operates by creating a stable, gas-filled pipeline that moves material from a source to a destination, all while preserving product quality and safety. By utilizing inert gas, the system eliminates the risk of oxidation, moisture absorption, or chemical reactions that could compromise the material being conveyed.
Core Components and Their Functions
The effectiveness of an inert gas circulating pneumatic conveying system relies on its integrated components, each playing a critical role in the overall operation. The system typically includes a material feed hopper, which holds the bulk material ready for transport. A gas source, often nitrogen or another inert gas, is connected to the system to provide the necessary pressure and flow. The conveying line, constructed from high-quality stainless steel to resist corrosion and maintain hygiene, forms the main pathway for material movement. At the receiving end, a discharge hopper collects the material, while a gas recycling unit captures and recycles the inert gas, minimizing waste and operational costs. This closed-loop design ensures that the system operates efficiently and sustainably, with minimal environmental impact.
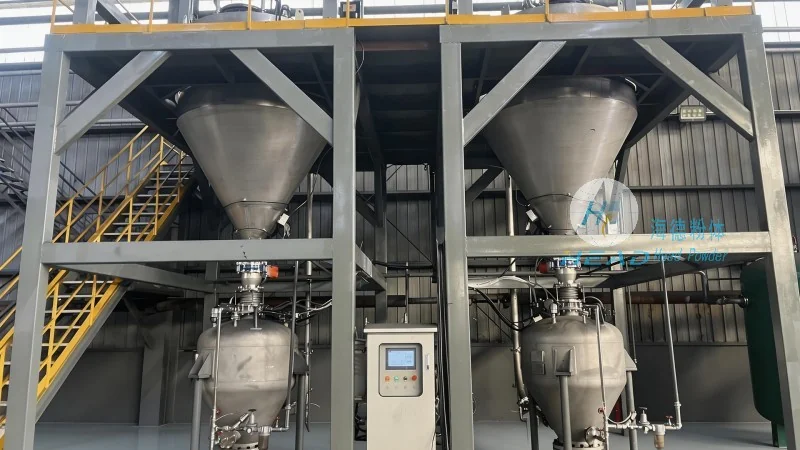
Design Principles and Operational Mechanics
The design principles of an inert gas circulating pneumatic conveying system are centered on fluidization and controlled gas dynamics. The system operates on the principle of creating a fluidized bed of material within the conveying line. By introducing the inert gas at a specific velocity, the material particles become suspended and move as a cohesive stream, rather than falling due to gravity. This fluidization reduces the risk of particle degradation, agglomeration, or segregation, ensuring that the material is transported uniformly and intact. The gas recycling unit is a key design element, as it continuously recirculates the inert gas, maintaining a stable pressure and flow throughout the system. This design minimizes gas consumption, enhances energy efficiency, and ensures consistent performance over extended periods. Additionally, the system is engineered for safety, as the use of inert gas eliminates the presence of oxygen, preventing fire or explosion risks, which is crucial when handling flammable or reactive materials.
Industrial Applications and Advantages
The inert gas circulating pneumatic conveying system offers significant advantages across various industrial sectors. In pharmaceutical manufacturing, it ensures that sensitive powders are handled in a sterile, oxygen-free environment, preventing contamination and maintaining product efficacy. In food processing, the system maintains the quality of ingredients by avoiding moisture absorption or oxidation, which could affect taste, texture, or shelf life. For chemical manufacturers, the system provides a safe and efficient way to transport reactive or hazardous materials without exposure to external air. The system's flexibility also allows for the transportation of diverse materials, including powders, granules, and even liquid suspensions, by adjusting gas flow rates and pressure. This adaptability makes it a versatile solution for a wide range of applications, enhancing operational efficiency and product quality.
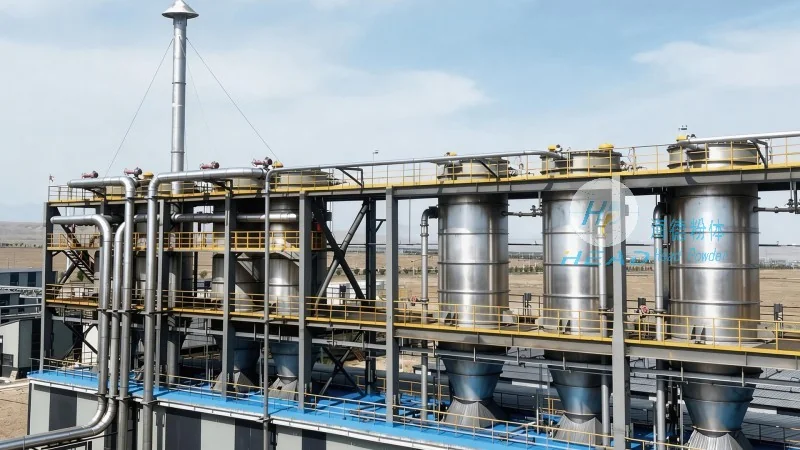
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name HeadPowder, is a leading provider of advanced pneumatic conveying systems. HeadPowder specializes in the design, manufacturing, and integration of inert gas circulating systems tailored to meet the unique requirements of clients in various industries. With a strong commitment to innovation and quality, HeadPowder has built a reputation for delivering reliable and efficient solutions that enhance productivity and safety. The company's team of experienced engineers and technicians works closely with clients to understand their operational challenges and develop customized solutions that address specific needs. HeadPowder's state-of-the-art manufacturing facilities and rigorous quality control processes ensure that every system meets the highest standards of performance, durability, and compliance with industry regulations.
Location and Service Commitment
HeadPowder is headquartered in Shandong, China, providing a strategic base for serving clients both domestically and internationally. The company's location in Shandong allows for easy access to key industrial markets and efficient logistics for delivering systems to clients worldwide. HeadPowder maintains a customer-centric approach, offering comprehensive support services including installation, commissioning, and ongoing maintenance. The company's technical support team is available to assist clients with any operational issues or system optimization, ensuring that the inert gas circulating pneumatic conveying systems operate at peak efficiency. HeadPowder's dedication to customer satisfaction and operational excellence has made it a trusted partner for businesses seeking reliable and effective material handling solutions.




