Understanding the mechanics and benefits of fertilizer granule pneumatic conveying systems is crucial for modern agricultural operations. These systems represent a sophisticated approach to transporting bulk granular materials, offering efficiency and reliability that traditional methods often struggle to match. The technology has evolved significantly over the years, adapting to the increasing demands of the fertilizer industry for faster, cleaner, and more sustainable material handling solutions.
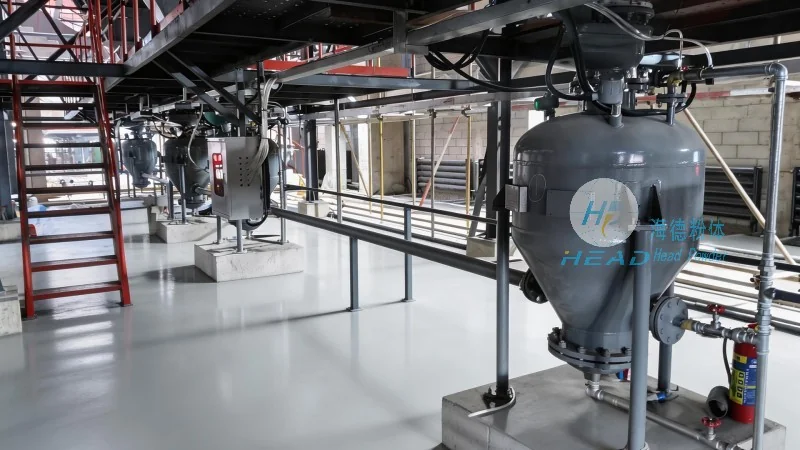
Key Components of the Pneumatic Conveying System
The core of any pneumatic conveying system for fertilizer granules consists of several interrelated components. At the heart of the system is the air supply unit, which generates the necessary pressure or vacuum to move the material. This unit typically includes a blower or compressor, depending on the system design—positive pressure systems use blowers to push material through pipes, while negative pressure systems employ vacuum pumps to draw material in. The feed hopper is another critical component, designed to hold and meter the fertilizer granules before they enter the conveying line. This hopper often features a screw feeder or rotary valve to control the flow rate, ensuring consistent material delivery. The conveying pipes form the main pathway for the material, constructed from durable materials like stainless steel or polyethylene to withstand the abrasive nature of fertilizer granules. The system may also include flexible hoses or elbows to navigate changes in direction or elevation. At the receiving end, a separator or cyclone is used to separate the material from the air stream, collecting the fertilizer granules in a discharge bin. Finally, a filter system is essential to capture any fine particles and ensure compliance with environmental regulations.
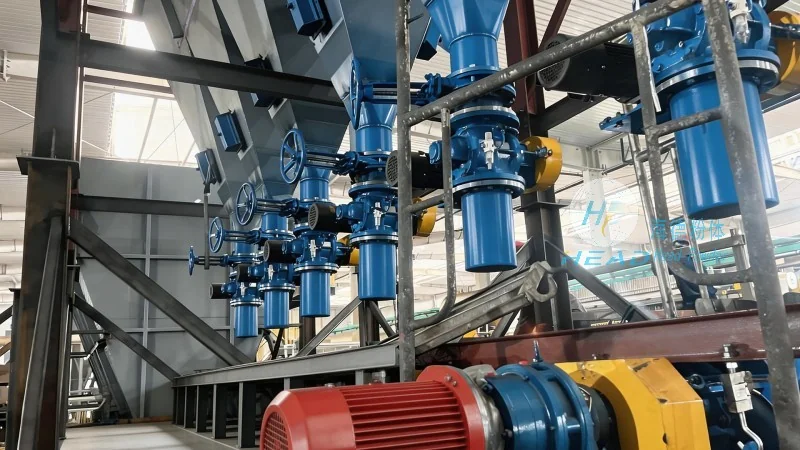
Advantages of Using Pneumatic Conveying for Fertilizer Granules
Implementing a pneumatic conveying system for fertilizer granules offers numerous advantages that directly impact operational efficiency and cost-effectiveness. One of the most significant benefits is the high conveying capacity, which allows for the transport of large volumes of material over long distances without the need for multiple transfer points. This reduces downtime and labor costs associated with manual handling or mechanical conveyors. The system is also highly hygienic and clean, as it eliminates the need for contact between the material and human hands or equipment, minimizing contamination risks and ensuring product quality. Additionally, pneumatic conveying systems are compact and space-saving, as they can be installed in tight spaces and do not require extensive infrastructure like traditional belt conveyors. The technology is also flexible, allowing for easy integration with existing production lines and the ability to adjust flow rates as needed. From an environmental perspective, these systems can be designed to be energy-efficient, with options for variable speed drives and optimized air usage, reducing operational costs and carbon footprint.
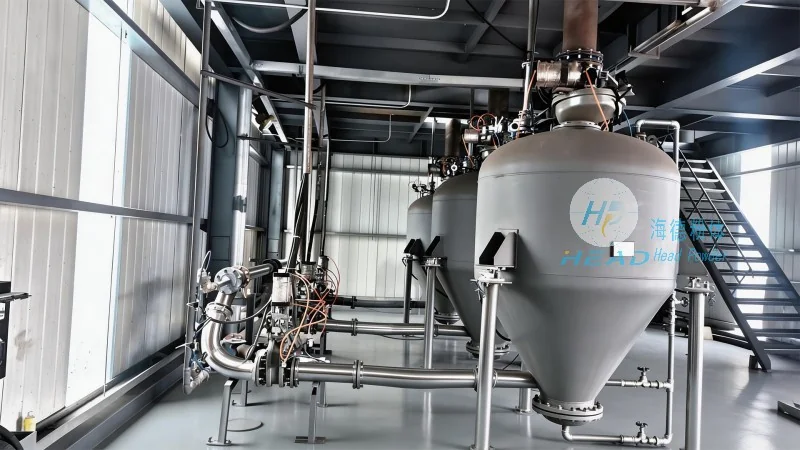
HeadPowder's Expertise in Fertilizer Granule Pneumatic Conveying
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of specialized engineering solutions for the fertilizer industry. With headquarters in Shandong, China, HeadPowder has built a strong reputation for delivering high-quality pneumatic conveying systems tailored to the unique needs of fertilizer manufacturers. The company’s expertise lies in designing and manufacturing custom systems that optimize material flow, minimize downtime, and enhance overall operational performance. HeadPowder’s team of engineers and technicians work closely with clients to understand their specific requirements, from the type of fertilizer granules being handled to the scale of the operation. This collaborative approach ensures that each system is tailored to maximize efficiency and cost savings. The company’s commitment to innovation is evident in its use of advanced materials and technologies, such as high-strength stainless steel for corrosion resistance and energy-efficient blowers for reduced operational costs. HeadPowder’s systems are designed to meet international standards and are backed by comprehensive after-sales support, including maintenance services and technical assistance, ensuring long-term reliability and performance.
Technical Specifications and Application Scenarios
The technical specifications of a fertilizer granule pneumatic conveying system vary depending on the specific application and the scale of the operation. For small-scale fertilizer plants, a positive pressure system with a blower and a few hundred meters of pipe may be sufficient. These systems typically handle capacities ranging from 1 to 5 tons per hour and are ideal for short-distance transport within a facility. For larger operations, such as bulk fertilizer production plants, a negative pressure system with a vacuum pump and longer pipe runs may be required. These systems can handle capacities up to 50 tons per hour or more, making them suitable for transporting material over distances of several kilometers. The choice between positive and negative pressure depends on factors like the material's density, the distance to be covered, and the need for environmental control. HeadPowder’s systems are designed to accommodate a wide range of technical specifications, including different pipe diameters, air velocities, and material flow rates. The company’s engineers can provide detailed calculations and recommendations based on the client's specific requirements, ensuring that the system is optimized for performance and efficiency. Typical application scenarios include transporting fertilizer granules from storage silos to production lines, moving material between processing stages, and delivering finished products to packaging or loading areas. The flexibility of pneumatic conveying systems makes them suitable for a variety of industrial settings, from small-scale farms to large-scale fertilizer manufacturing facilities.
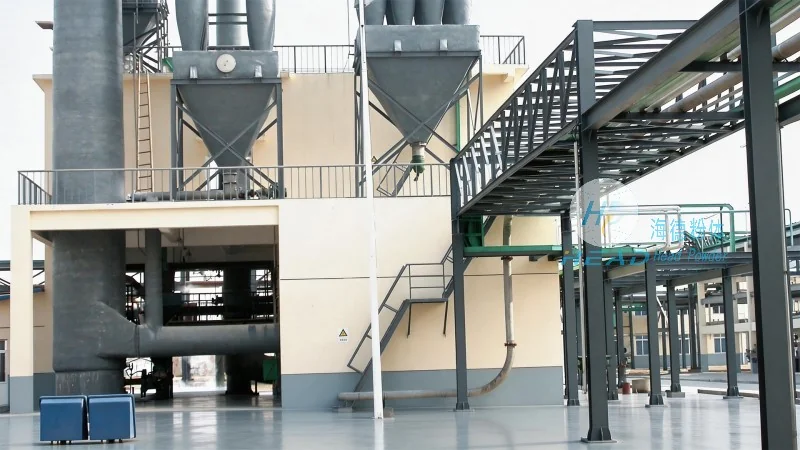
Conclusion
In conclusion, fertilizer granule pneumatic conveying systems represent a highly effective and efficient solution for modern agricultural operations. By leveraging the power of air to transport bulk materials, these systems offer significant advantages over traditional methods, including increased capacity, improved hygiene, and reduced operational costs. The technology has become an essential component of the fertilizer industry, enabling manufacturers to meet the growing demand for high-quality fertilizers while maintaining operational efficiency. Companies like Shandong HeadPowder Engineering Co., Ltd. play a vital role in providing the expertise and engineering solutions needed to implement these systems successfully. With their commitment to innovation and customer satisfaction, HeadPowder continues to be a trusted partner for fertilizer manufacturers seeking to enhance their material handling capabilities. As the industry evolves, the importance of efficient and reliable pneumatic conveying systems will only grow, making them a critical investment for any fertilizer operation.




