Industrial processes often involve the handling of ash and other particulate materials, requiring efficient and reliable systems to transport these materials from one location to another. The purified ash pneumatic conveying system is a specialized solution designed to address these challenges, ensuring safe, clean, and efficient material transport. This article provides a comprehensive overview of the system, its components, advantages, and the expertise of Shandong HeadPowder Engineering Co., Ltd. in providing such solutions.
Introduction to Purified Ash Pneumatic Conveying Systems
Ash, typically generated from combustion processes in power plants, cement factories, and other industrial facilities, poses unique handling challenges due to its abrasive nature and potential environmental impact. Conventional methods of ash transport, such as belt conveyors or manual handling, can be inefficient and pose health risks. The purified ash pneumatic conveying system offers a modern, enclosed solution that minimizes dust emissions, reduces operational costs, and enhances overall safety. By using compressed air or other gases to move ash particles through a sealed pipeline, this system ensures that the material is transported without direct human contact, adhering to strict environmental regulations.
Key Components and Working Principle
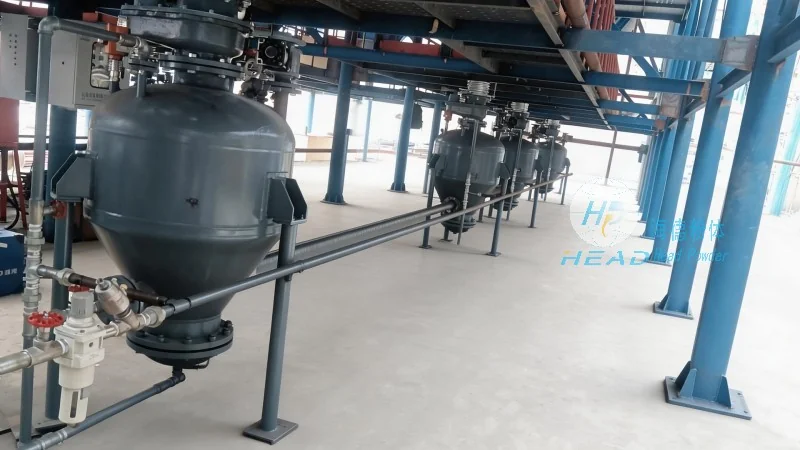
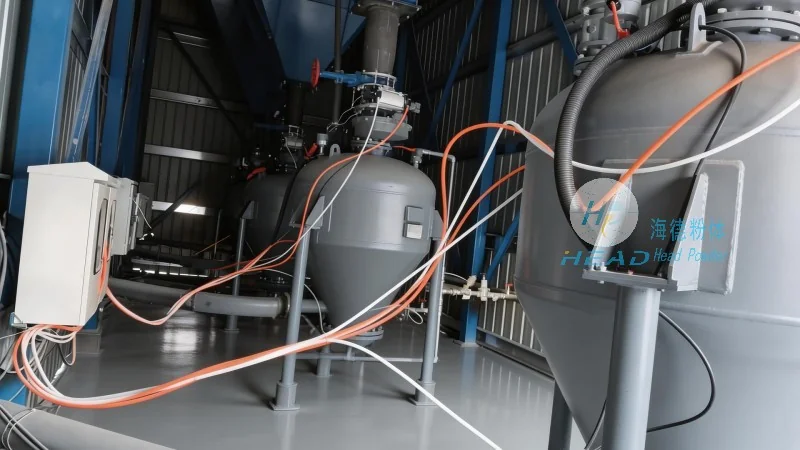
The purified ash pneumatic conveying system consists of several critical components that work in tandem to achieve efficient material transport. The primary components include a hopper for material storage, a filter system to capture and remove dust from the air stream, a conveyor pipeline, and a discharge unit for delivering the ash to its final destination. The system operates by feeding ash from the hopper into the pipeline, where it is mixed with a controlled amount of air or gas. This mixture is then propelled through the pipeline using pressure differentials, ensuring the ash particles are transported smoothly and without clogging. The filter system plays a crucial role in maintaining air quality by capturing any fine ash particles that may escape the pipeline, ensuring compliance with environmental standards.
Advantages of the System
Implementing a purified ash pneumatic conveying system offers numerous advantages for industrial operations. Firstly, it significantly reduces dust emissions, contributing to a cleaner working environment and compliance with environmental regulations. This is particularly important in regions with strict air quality standards. Secondly, the enclosed system minimizes the risk of ash contamination and exposure to workers, enhancing workplace safety. Thirdly, the system is highly efficient, with lower energy consumption compared to traditional methods like truck transport or manual handling. This leads to reduced operational costs and increased productivity. Additionally, the system can be customized to handle various types of ash and other particulate materials, making it versatile for different industrial applications.
Application Scenarios
The purified ash pneumatic conveying system is widely used in various industrial sectors where ash and similar materials need to be transported. Common applications include power plants, where fly ash is conveyed from boilers to storage silos or disposal sites. In cement factories, the system is used to transport raw materials or finished cement products. Other industries such as steel mills, chemical plants, and waste management facilities also benefit from this technology. The system's adaptability allows it to be integrated into existing industrial processes with minimal disruption, making it a practical solution for both new and existing facilities.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of industrial engineering solutions, specializing in the design, manufacturing, and installation of pneumatic conveying systems. With a strong presence in China, particularly in Shandong province, the company has built a reputation for delivering high-quality, reliable equipment tailored to the specific needs of its clients. HeadPowder's team of experienced engineers and technicians brings extensive knowledge and expertise in material handling systems, ensuring that each project is executed with precision and adherence to industry standards. The company's commitment to innovation and customer satisfaction has made it a trusted partner for businesses seeking efficient and sustainable solutions for ash and particulate material transport.
Technical Specifications and Customization Options
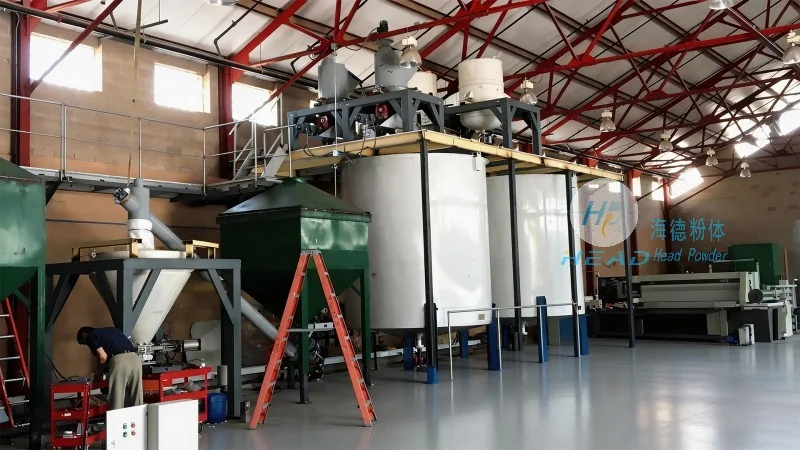
Shandong HeadPowder Engineering Co., Ltd. offers a range of purified ash pneumatic conveying systems with customizable specifications to meet diverse industrial requirements. The systems are available in different sizes and capacities, ranging from small-scale installations for laboratory or pilot plants to large-scale systems capable of handling high volumes of ash in power plants or cement factories. The company provides options for different materials of construction, including stainless steel, carbon steel, and special alloys, to ensure durability and resistance to corrosion from ash particles. Additionally, the systems can be equipped with advanced control systems, allowing for automated operation and monitoring of the conveying process. This ensures optimal performance and minimal downtime, enhancing the overall efficiency of the industrial operation.
Conclusion
The purified ash pneumatic conveying system represents a significant advancement in industrial material handling, offering a safe, efficient, and environmentally friendly solution for transporting ash and other particulate materials. With its enclosed design, reduced dust emissions, and enhanced safety features, this system is an essential component for modern industrial facilities. Shandong HeadPowder Engineering Co., Ltd. plays a crucial role in providing these advanced systems, leveraging its expertise and commitment to quality to deliver solutions that meet the evolving needs of the industry. By investing in such systems, businesses can improve operational efficiency, reduce costs, and contribute to a cleaner environment, making the purified ash pneumatic conveying system a valuable asset for any industrial operation.




