Introduction to the Rice Starch Powder Conveying System: Structure and Working Principle
Release time:2026-09-22 04:01:32
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Zhang manager
HeadPowder, a leading manufacturer in the field of powder handling technology, presents an in-depth overview of its rice starch powder conveying system. This system is engineered to meet the precise demands of industrial applications, ensuring efficient and reliable material transport for rice starch powder. The following sections will delve into the system's structural design and operational principles, highlighting key components and their functional roles.
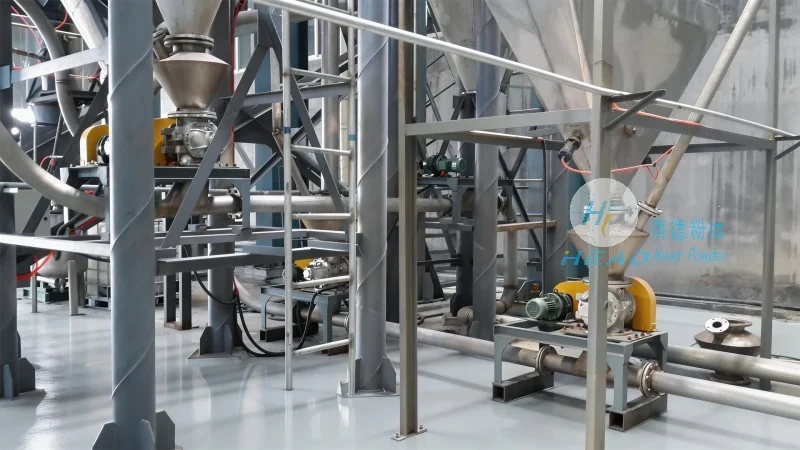
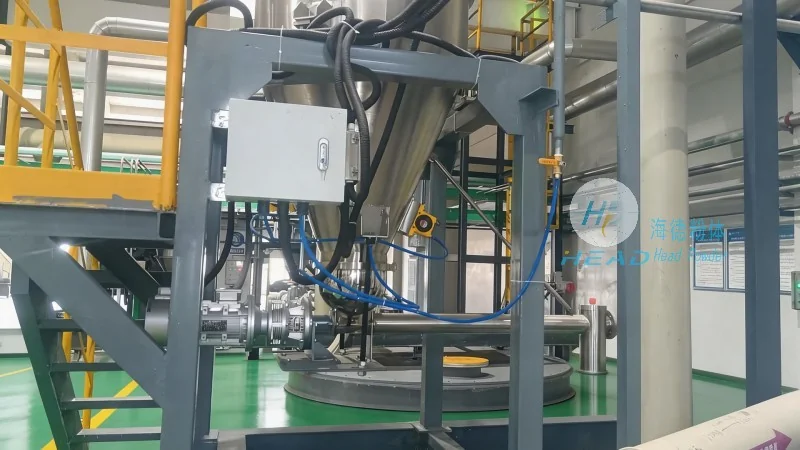
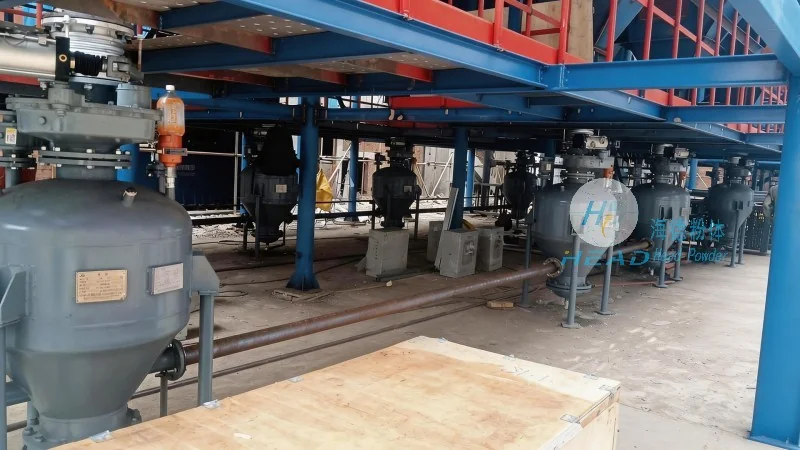
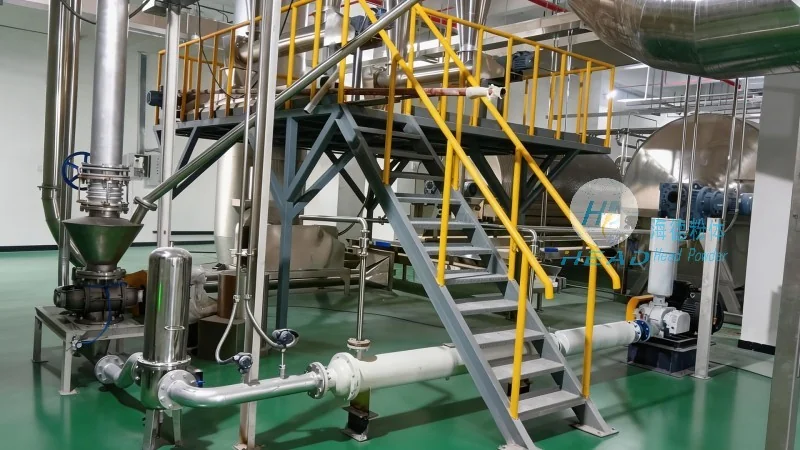
System Structure Overview
HeadPowder's rice starch powder conveying system is a sophisticated industrial solution designed to efficiently handle the unique properties of rice starch powder. The system comprises several critical components that work in concert to ensure reliable material transport. The primary components include a large-capacity storage hopper, a high-performance conveyor mechanism (such as a screw or pneumatic conveyor), and an advanced control unit. The hopper is constructed with a sloped interior and smooth, food-grade surfaces to facilitate natural material flow, preventing caking and ensuring consistent feeding. Its material, typically stainless steel or food-grade plastic, is chosen for its resistance to corrosion and compatibility with the powder. The conveyor mechanism is selected based on the powder's characteristics, including moisture content and flowability. For instance, a screw conveyor is ideal for handling free-flowing rice starch powder, as it uses a rotating helical screw to push the material forward. In contrast, a pneumatic conveyor may be preferred for finer powders that require less mechanical contact, utilizing air pressure to transport the powder. The control unit integrates sensors like level indicators and pressure transducers to monitor the system's status in real-time. These sensors provide critical data on material levels, conveyor speed, and pressure, enabling the control unit to adjust operations dynamically. The system also includes a discharge valve or outlet that regulates the flow of powder to the next processing stage, ensuring seamless integration into the production line.
Working Principle and Operational Mechanism
The operational principle of the rice starch powder conveying system revolves around the seamless transfer of rice starch powder from the storage hopper to the discharge point. The process begins with the material being fed into the hopper, where it accumulates until the conveyor is activated. The conveyor mechanism then initiates its operation, using mechanical or pneumatic forces to move the powder forward. In a screw conveyor configuration, a rotating screw blade pushes the powder along the conveyor tube, while the hopper's sloped design ensures a continuous flow. The speed of the screw and the angle of the hopper are carefully calibrated to maintain an optimal flow rate, preventing material buildup or blockages. The control unit plays a pivotal role in regulating the conveyor speed and feed rate. It adjusts these parameters based on real-time data from the sensors, such as the hopper level and conveyor load. This dynamic control ensures that the discharge rate matches the production requirements, minimizing waste and maximizing efficiency. The system also incorporates safety features, including overload protection and emergency stop mechanisms, to safeguard both the equipment and personnel. The working principle is designed to be robust and adaptable, allowing the system to handle different batches of rice starch powder with consistent performance. It can handle varying moisture levels and particle sizes, making it suitable for diverse industrial applications.




