Principles and Working Scene Characteristics of Intelligent Weighing Pneumatic Conveying
Release time:2026-09-18 14:01:24
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Zhang manager
Intelligent weighing pneumatic conveying systems represent a sophisticated solution in material handling, integrating advanced weighing technology with pneumatic transport mechanisms. This technology is designed to efficiently move bulk materials through a system of pipes using air pressure, while simultaneously providing precise weight measurement at various points in the process. The integration of intelligent control systems further enhances operational efficiency and accuracy, making it suitable for a wide range of industrial applications, from pharmaceutical and food processing to chemical production and beyond.
Principles of Operation
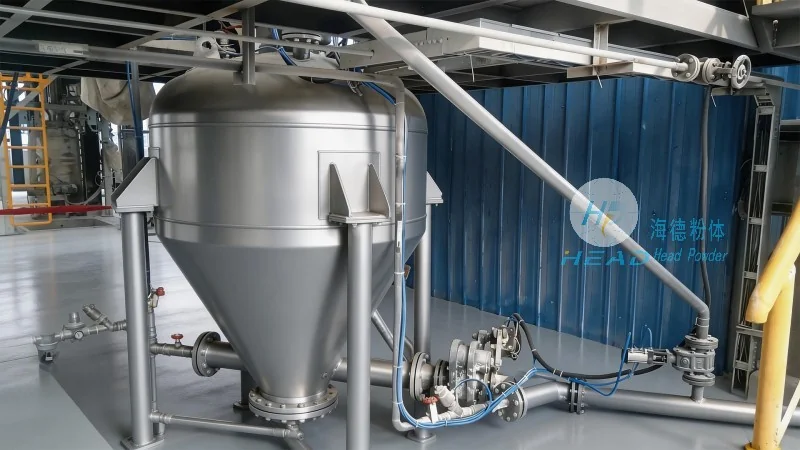
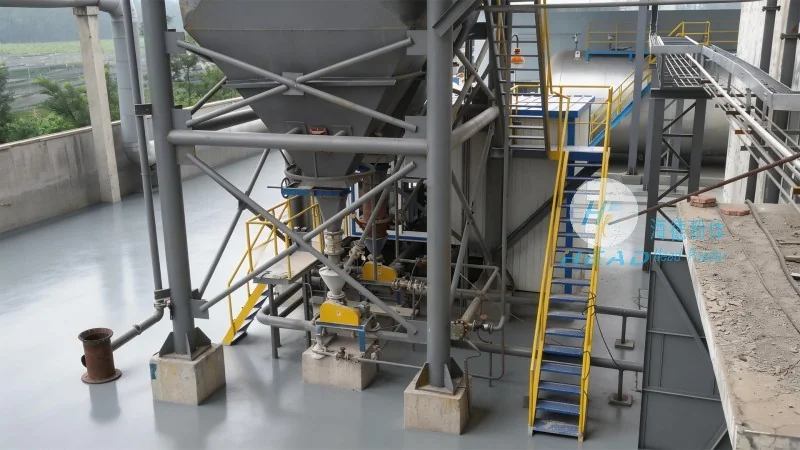
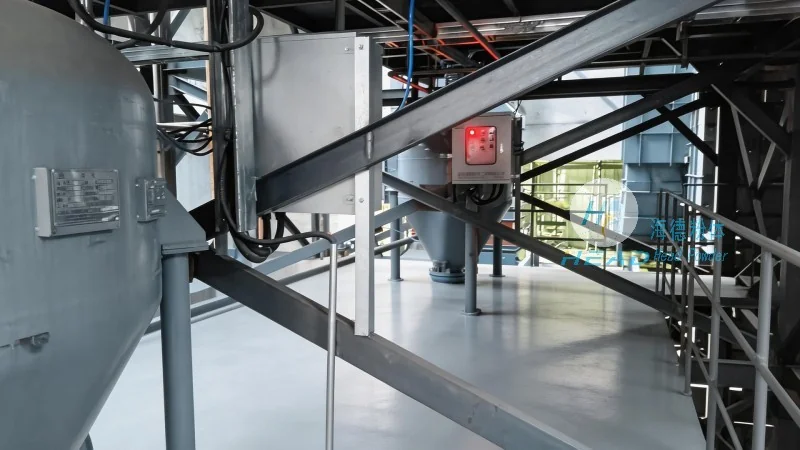
The core principle of intelligent weighing pneumatic conveying involves the use of air as the medium to transport materials from a source to a destination. The system typically consists of a hopper for material storage, a feeder to control the flow of material into the conveying line, a blower or compressor to generate the air pressure, and a receiver to collect the conveyed material. As materials move through the system, load cells or sensors are strategically placed at key points (such as the hopper, feeder, and receiver) to measure the weight of the material in real-time. This data is transmitted to an intelligent control unit, which processes the information and adjusts the air flow and material feed rate accordingly. The system’s ability to monitor and adjust parameters in real-time ensures optimal conveying conditions, preventing issues such as material blockages or uneven flow. Additionally, the intelligent control unit can integrate with other equipment, such as mixers or packaging machines, to create a seamless material handling process. The result is a highly efficient and accurate system that minimizes waste, reduces energy consumption, and maximizes productivity. By optimizing air pressure and material feed rates, the system operates with lower energy costs compared to traditional pneumatic conveying systems, making it a cost-effective solution for long-term use.
Key Working Scene Characteristics
Intelligent weighing pneumatic conveying systems are particularly well-suited for applications where precise material handling and monitoring are critical. Common working scenes include pharmaceutical manufacturing, where the system ensures the exact dosage of active ingredients is conveyed to the next stage of production, maintaining strict quality control standards. In food processing, the system helps maintain hygiene by containing powders within a sealed system, reducing the risk of contamination and ensuring product safety. Chemical production also benefits from this technology, as it allows for precise measurement and transport of hazardous or sensitive materials, minimizing the risk of spills or accidents. The flexibility of the system also makes it suitable for handling a variety of materials, including fine powders, granules, and bulk solids, adapting to different particle sizes and flow characteristics. This adaptability, combined with the system’s ability to provide real-time weight data, makes it an ideal solution for industries where consistency and accuracy are paramount. Furthermore, the system’s ability to integrate with automated processes reduces the need for manual intervention, improving safety and reducing labor costs. Overall, intelligent weighing pneumatic conveying systems offer a reliable and efficient solution for modern industrial material handling needs.




