For industries dealing with nickel sulfate, efficient material handling is crucial. The nickel sulfate material pneumatic conveying equipment from Shandong HeadPowder Engineering Co., Ltd. offers a reliable solution that combines advanced technology with practical design. This equipment is engineered to handle the unique properties of nickel sulfate, ensuring safe and efficient transport while maintaining product integrity.
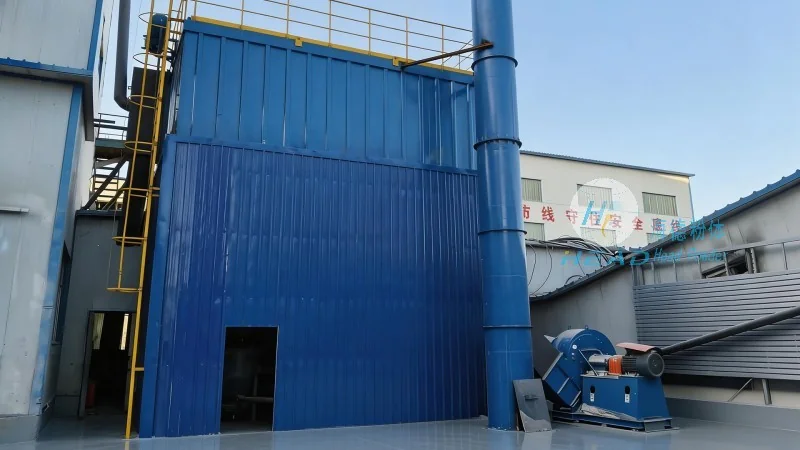
Company Overview
HeadPowder, the professional manufacturer behind this equipment, is a leading company in the field of material handling solutions. With years of experience and a commitment to quality, HeadPowder provides customized pneumatic conveying systems tailored to the specific needs of various industries. The company’s headquarters is located in Shandong, China, where it leverages local expertise and resources to develop cutting-edge equipment for global markets.
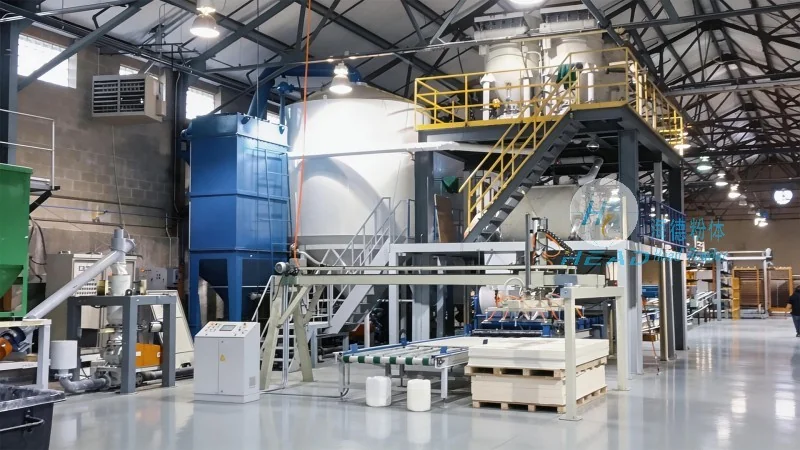
Working Principle of Nickel Sulfate Pneumatic Conveying Equipment
The core of the nickel sulfate material pneumatic conveying system is its pneumatic conveying mechanism, which operates by using air as the medium to transport bulk materials. The process begins with the material being fed into the hopper. From there, the material is drawn into the conveying line by a vacuum or pressure source, depending on the system configuration. The equipment typically includes components such as a feeder, a conveying line, a separator, and a receiver. The feeder ensures a consistent flow of nickel sulfate into the system, while the conveying line transports the material through the air stream. The separator then separates the material from the air, and the receiver collects the processed nickel sulfate. This entire process is controlled by a sophisticated control system that optimizes the flow rate and pressure, ensuring efficient and reliable operation.
Key Features of the Nickel Sulfate Pneumatic Conveying Equipment
One of the standout features of this equipment is its ability to handle the hygroscopic and corrosive nature of nickel sulfate. The system is designed with materials that are resistant to corrosion, such as stainless steel, to prevent degradation over time. Additionally, the equipment incorporates dust control measures to minimize environmental impact and ensure workplace safety. The modular design allows for easy installation and maintenance, reducing downtime and operational costs. Another key feature is the adjustable conveying capacity, which can be customized to meet the varying demands of different production processes. The equipment also features a low maintenance design, with components that are easy to replace and service, further enhancing its long-term reliability.
Advantages in Material Handling
Using the nickel sulfate material pneumatic conveying equipment offers several advantages over traditional methods. First, it eliminates the need for manual handling, reducing the risk of accidents and improving workplace safety. Second, the system is highly efficient, with minimal material loss and low energy consumption. This translates to cost savings for the end-user. Third, the equipment is capable of handling materials in a closed system, preventing contamination and maintaining product purity. This is particularly important for nickel sulfate, which is often used in pharmaceutical and chemical applications where purity is critical. Finally, the system’s flexibility allows it to be integrated into existing production lines with minimal modifications, making it a practical solution for existing facilities.




