Working Principle and Characteristics of Powder Handling for Desulfurization and Denitrification Age
Release time:2026-09-17 10:01:21
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Zhang manager
Comprehending the working principle and characteristics of powder handling systems is vital for optimizing the operation of desulfurization and denitrification processes in industrial environments. These systems are engineered to efficiently transport powders such as desulfurization and denitrification agents, which are essential for mitigating air pollutants like sulfur dioxide (SO₂) and nitrogen oxides (NOₓ).
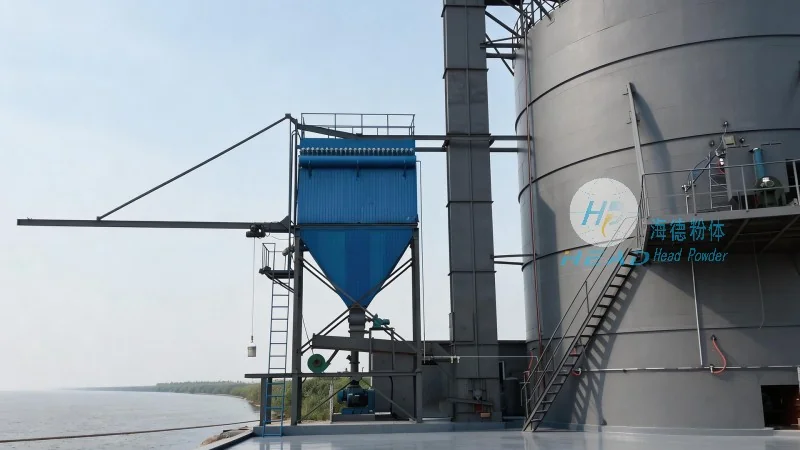
Working Principle of Powder Handling for Desulfurization and Denitrification Agents
The fundamental working principle of powder handling systems for these agents commonly involves pneumatic or mechanical conveying methods. In pneumatic systems, a fan or blower generates airflow that propels powder particles through a network of pipes. The powder is fed from a hopper or silo into the system, where it is entrained by the air stream and transported to the desired location, such as a reactor or storage tank. Key components include the air compressor, dust filter, and control valves, which regulate the flow rate and pressure to ensure stable and efficient transport. Mechanical systems, alternatively, use screw conveyors or belt conveyors to move the powder through a closed or open system, relying on mechanical force rather than air pressure.
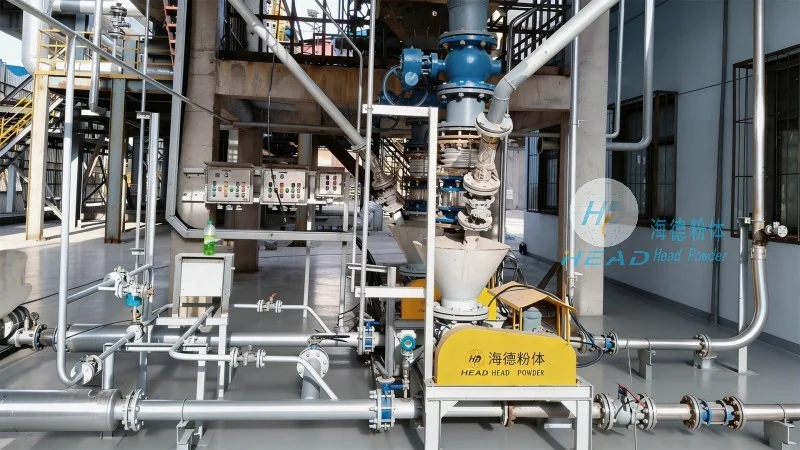
Key Characteristics of Powder Handling Systems for Desulfurization and Denitrification Agents
Several key characteristics define the performance of these powder handling systems. Firstly, efficiency is paramount, as the systems must deliver high throughput rates while minimizing energy consumption. This is achieved through optimized airflow or mechanical design, ensuring that the powder is transported with minimal loss or degradation. Secondly, environmental considerations are critical, as the systems must prevent dust emissions and maintain air quality compliance. Advanced filtration and sealing technologies are employed to contain particles and prevent contamination of the surrounding environment. Thirdly, adaptability is essential, as different desulfurization and denitrification agents may have varying particle sizes, densities, and flow properties. The systems are designed to accommodate a wide range of materials, with adjustable parameters to match specific operational requirements. Additionally, automation and control features enhance operational reliability, allowing for real-time monitoring and adjustment of the conveying process to maintain consistent performance.
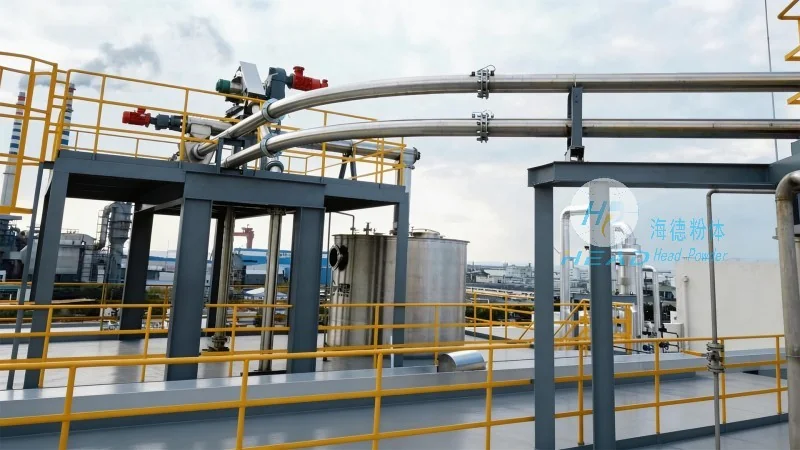
Company Introduction: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading provider of specialized powder handling solutions tailored for the environmental protection industry. With a focus on innovation and customer-centric design, the company has established itself as a trusted partner for businesses seeking to enhance the efficiency and sustainability of their desulfurization and denitrification operations. Headpowder's headquarters is located in Shandong, China, where the company leverages local expertise and advanced manufacturing capabilities to develop and deliver high-quality systems. The company's commitment to quality and reliability ensures that its products meet stringent industry standards and contribute to the reduction of air pollution in industrial applications. By combining technical expertise with practical application knowledge, headpowder offers customized solutions that address the unique challenges faced by clients in the field of air pollution control.




