HeadPowder, a leading manufacturer based in Shandong, China, specializes in providing advanced solutions for dust-free and airtight powder conveying systems. These systems are designed to handle bulk powders efficiently while maintaining strict environmental and safety standards. Understanding the working principle and key features of such systems is crucial for industries that rely on precise and reliable powder transport.
Working Principle of Dust-Free Powder Conveying Systems
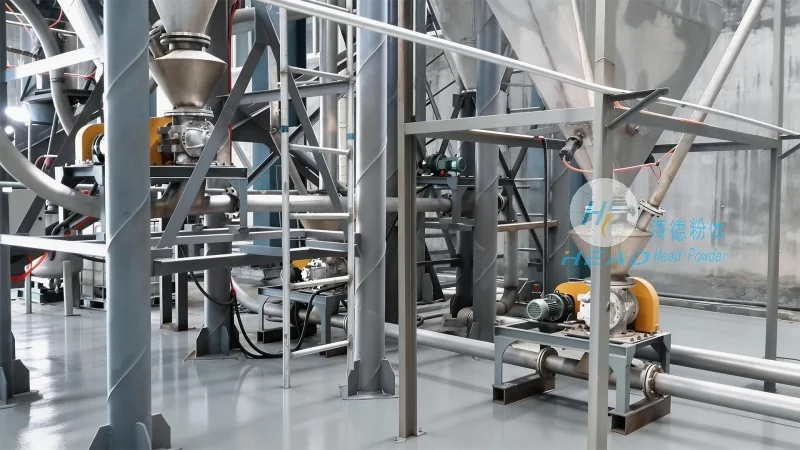
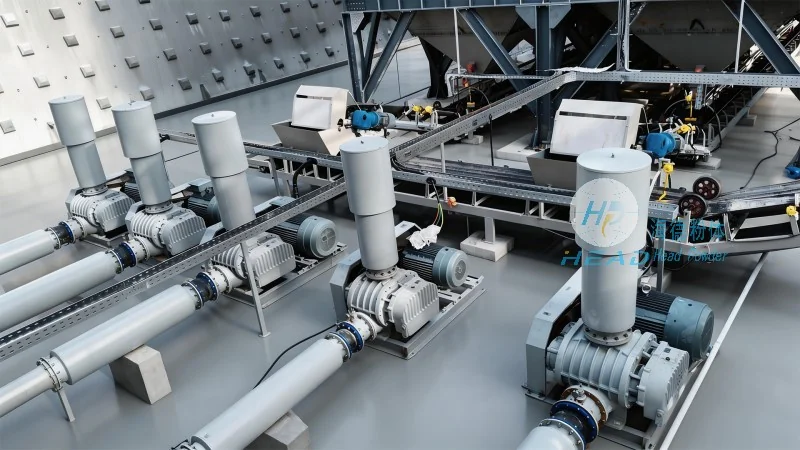
The core working principle of dust-free and airtight powder conveying systems revolves around the creation of a sealed, controlled environment to prevent powder particles from escaping into the ambient air. This is achieved through a combination of mechanical and pneumatic technologies that work together to transport powders from a source to a destination without exposing them to open air. The system typically comprises a feed hopper or storage tank, a conveying line (either rigid or flexible, often made of stainless steel or food-grade materials), and a receiving vessel. The process begins when the powder is discharged from the source container into the conveying line. In pneumatic systems, compressed air is introduced to create a flow that carries the powder particles through the line. The air-powder mixture is then separated at the receiving end, usually via a cyclone separator or filter, where the powder is collected and the air is either recirculated or safely vented. Mechanical systems, such as screw conveyors or positive displacement pumps, rely on physical force to push the powder through the sealed line. These systems are particularly effective for handling cohesive or abrasive powders that may not be easily transported by air. The airtight design ensures that the entire transport process is contained, minimizing dust generation and exposure to personnel. This principle is fundamental to maintaining product purity, workplace safety, and compliance with environmental regulations.
Key Features of Dust-Free and Airtight Powder Conveying Systems
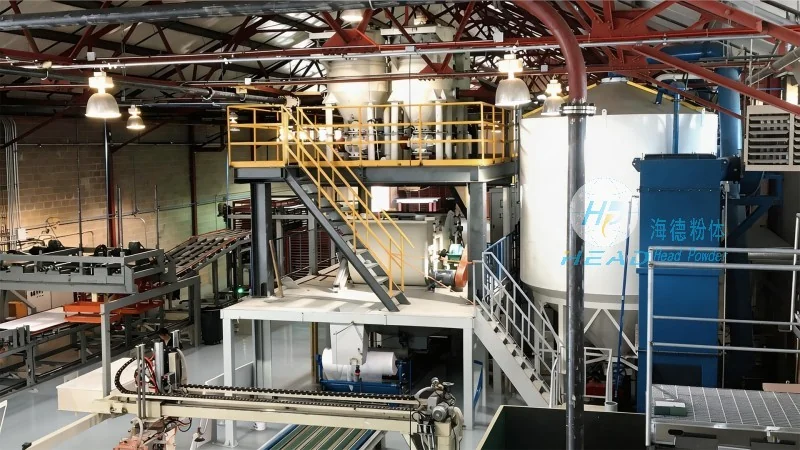
Several critical features define the performance and advantages of dust-free and airtight powder conveying systems, making them indispensable for industries where precision, safety, and environmental compliance are non-negotiable. First, the airtight and sealed design prevents cross-contamination between different powders, which is essential in sectors like pharmaceuticals, food, and specialty chemicals where product purity and batch integrity are paramount. This feature ensures that each batch of powder remains free from contaminants from other materials, maintaining the quality and consistency required for regulatory approval. Second, the enclosed system significantly reduces the risk of dust explosions by eliminating the presence of airborne dust particles that could ignite under the right conditions. The systems incorporate explosion-proof components, such as spark-resistant motors and pressure relief valves, and often include inert gas purging to further mitigate explosion risks. Third, these systems are engineered for high efficiency, with low energy consumption and rapid transport speeds that allow for large volumes of powder to be moved quickly and reliably. The modular design enables easy integration into existing production lines, with options for customization based on the specific flow rates, powder characteristics, and operational requirements. Fourth, the use of high-quality, corrosion-resistant materials, such as stainless steel and food-grade plastics, enhances the durability and hygiene of the equipment. This ensures long-term performance, minimal maintenance, and compliance with hygiene standards in industries like food and pharmaceuticals. Additionally, the systems are designed for easy cleaning and maintenance, with removable components that can be sanitized to prevent microbial growth and contamination.
Applications and Benefits in Industrial Settings
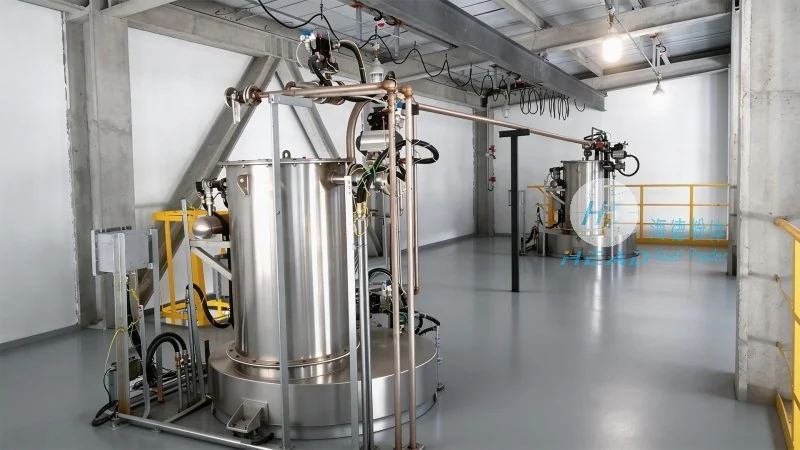
Dust-free and airtight powder conveying systems find extensive applications across a wide range of industries, including pharmaceutical manufacturing, food processing, chemical production, and mining. In the pharmaceutical industry, these systems are critical for transporting active pharmaceutical ingredients (APIs) and excipients while maintaining sterile conditions and preventing cross-contamination. The enclosed design ensures that the powders remain free from environmental contaminants, which is essential for meeting stringent regulatory requirements. In the food industry, the systems are used to handle powders like flour, sugar, and spices, where dust control is vital to prevent product degradation and ensure consumer safety. The airtight design also helps maintain product freshness by preventing moisture absorption and contamination. In the chemical industry, these systems help manage hazardous powders, such as powders used in the production of fertilizers or industrial chemicals, reducing the risk of accidents and environmental pollution. The primary benefits of these systems include improved workplace safety, reduced environmental impact, and enhanced product quality. By eliminating dust emissions, companies can avoid costly dust control measures, such as air filtration systems and dust collection equipment, and instead focus on core production activities. The long-term cost savings from reduced maintenance, lower energy consumption, and increased operational efficiency make these systems a valuable investment for any business that handles bulk powders. Furthermore, the reliability of these systems ensures consistent production output, minimizing downtime and improving overall productivity.




