

Working Principle and Features of Dry Ash Pneumatic Conveying Equipment
Dry ash pneumatic conveying equipment operates by utilizing air as the primary medium to transport dry ash materials. The system typically comprises several critical components: a material hopper for ash storage, a blower or fan to generate the necessary airflow, a conveying pipeline to guide the ash and air mixture, and a separator or filter to separate the ash from the air at the receiving end. The process initiates when dry ash is fed into the material hopper. The blower then creates a pressure differential, either by drawing air (negative pressure system) or pushing air (positive pressure system), which propels the ash particles through the pipeline. As the ash travels through the pipeline, it is suspended in the air stream, maintaining a consistent flow. Upon reaching the destination, the air and ash mixture enters the separator, where the heavier ash particles are deposited, and the lighter air is either discharged or recirculated back to the blower. This closed-loop or open-loop system ensures efficient and controlled transportation of dry ash, minimizing dust emissions and maximizing material throughput. The design of the system allows for flexibility in layout, enabling it to adapt to various industrial settings and transportation distances, from short-distance transfers within a facility to long-distance transport between sites. The system's ability to handle abrasive materials without significant wear and tear ensures long-term operational efficiency, reducing maintenance and replacement costs over time.
Key Features of Dry Ash Pneumatic Conveying Systems
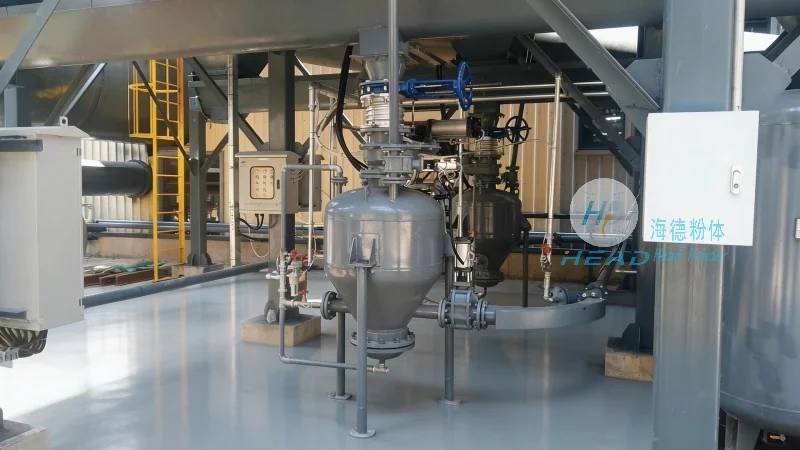
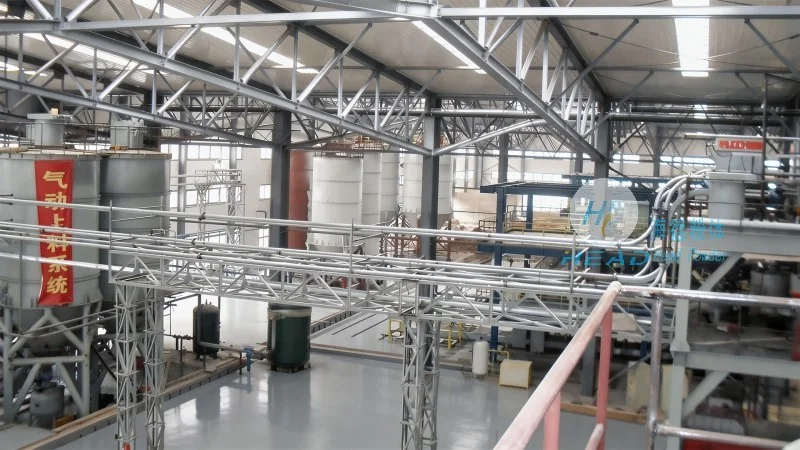
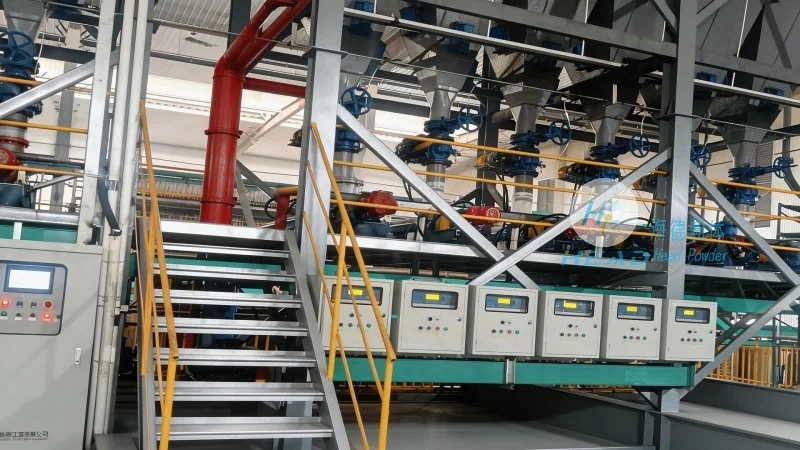
Shandong HeadPowder Engineering Co., Ltd. develops dry ash pneumatic conveying systems that are characterized by several distinct features. One of the primary features is the high efficiency in material transport, achieved through optimized airflow and pipeline design. The systems are engineered to handle large volumes of dry ash with minimal energy consumption, making them cost-effective for industrial operations. Another key feature is the durability and robust construction, which is essential for withstanding the abrasive nature of ash particles. The equipment uses high-quality materials, such as stainless steel and wear-resistant components, to ensure long service life and reduce maintenance needs. Advanced control systems are integrated into the design, allowing for precise regulation of airflow, material feed rate, and system pressure. This control capability enhances operational stability and allows for real-time monitoring and adjustments. Additionally, the systems incorporate effective dust control measures, including efficient separators and filtration units, to minimize environmental impact and comply with environmental regulations. The design also prioritizes ease of maintenance, with accessible components and modular construction that simplify routine checks and repairs. These features collectively make the dry ash pneumatic conveying systems from Shandong HeadPowder Engineering Co., Ltd. a reliable and efficient solution for ash handling in various industrial applications.
Application and Benefits in Industrial Settings
Dry ash pneumatic conveying equipment is extensively used in power generation facilities, where large quantities of fly ash are produced as a byproduct of coal combustion. The equipment efficiently transports this ash from the boiler to storage silos or disposal sites, eliminating the need for manual handling and reducing labor costs. In cement factories, the system handles raw material ash and other byproducts, contributing to the overall production process. The primary benefits of using dry ash pneumatic conveying systems include improved operational efficiency, reduced labor requirements, and enhanced safety in the workplace. By automating the ash transport process, the systems minimize the risk of dust exposure and accidents associated with manual handling. Furthermore, the efficient separation of ash from air reduces environmental pollution, making the process more sustainable and compliant with environmental standards. The long-term benefits include lower maintenance costs due to the durable construction and reduced wear and tear, as well as increased productivity from consistent and reliable operation. Overall, the dry ash pneumatic conveying systems from Shandong HeadPowder Engineering Co., Ltd. provide a comprehensive solution that addresses the challenges of ash handling in industrial settings, combining performance, reliability, and environmental responsibility.