Stone pneumatic conveying systems are advanced industrial solutions designed to transport bulk materials, particularly stones and aggregates, through a pipeline using compressed air. These systems offer an efficient and flexible method for material handling, eliminating the need for traditional mechanical conveyors and reducing operational costs and maintenance requirements. The technology has become increasingly popular in various industries due to its ability to handle abrasive materials while maintaining high throughput and minimal product degradation.
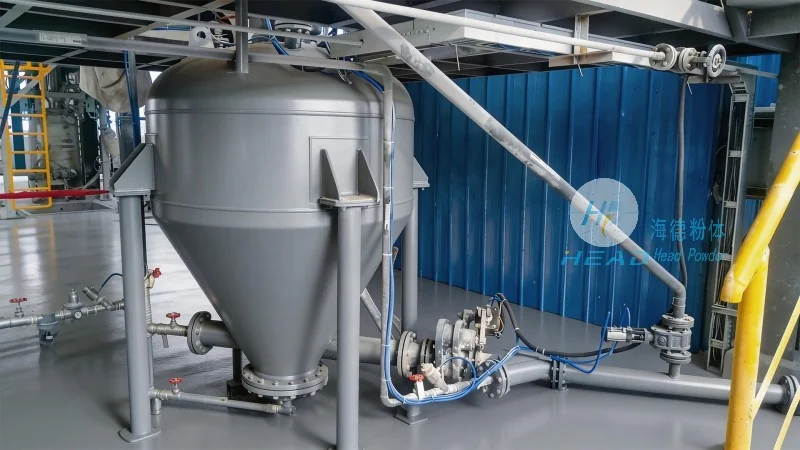
Working Principle of Stone Pneumatic Conveying Systems
The core mechanism of a stone pneumatic conveying system involves the use of compressed air to create a flow that propels the material through a sealed pipeline. The process typically begins with the material being fed into a hopper or feeder, where it is then drawn into a venturi or a pressure vessel. Compressed air, often supplied by a dedicated air compressor, is introduced into the system, creating a low-pressure zone that pulls the material into the pipeline. As the air and material mixture travels through the pipeline, the air velocity is maintained at a level sufficient to keep the material suspended and transported to the destination point. The system can operate in either positive pressure or negative pressure modes, depending on the specific design and application requirements. Positive pressure systems use compressed air to push the material, while negative pressure systems use suction to draw the material. The choice between these modes depends on factors such as the distance of material transport, the type of material, and the layout of the conveying line.
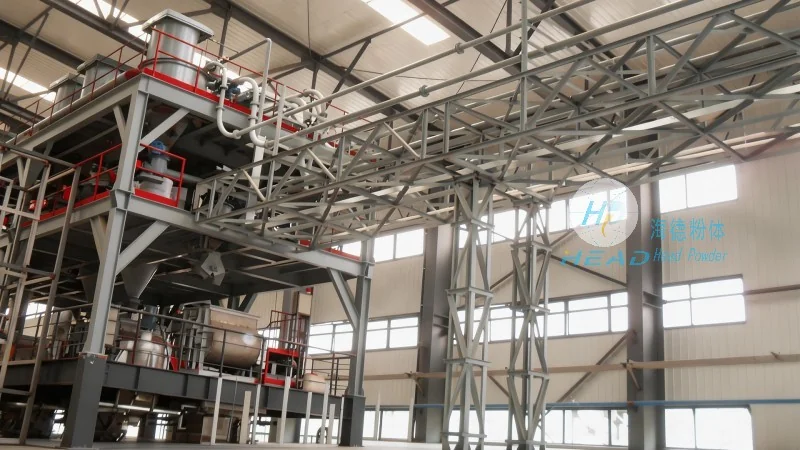
Key Features and Advantages of Stone Pneumatic Conveying Systems
Stone pneumatic conveying systems offer several distinct advantages that make them a preferred choice for material handling in construction, mining, and other industries. One of the primary features is their ability to handle abrasive and heavy materials without causing wear and tear on the system components. The sealed pipeline design prevents dust and debris from escaping into the environment, ensuring compliance with environmental regulations and maintaining a clean working environment. Additionally, these systems provide high flexibility in terms of layout, as the pipeline can be installed in various configurations, including vertical, horizontal, or a combination of both, to accommodate different site conditions and material flow paths. The systems also offer excellent control over material flow, allowing for precise regulation of the conveying rate and pressure, which is crucial for maintaining consistent production processes. Another notable feature is the reduced maintenance requirements compared to traditional mechanical conveyors, as there are fewer moving parts and less exposure to abrasive materials, leading to lower operational costs and longer system lifespan.
Application and Operational Considerations
Stone pneumatic conveying systems are widely used in applications where the transport of bulk materials over medium to long distances is required. Common applications include the transportation of aggregates from quarries to processing plants, the movement of crushed stones in construction sites, and the handling of recycled materials in waste management facilities. The systems are particularly advantageous in environments where space is limited or where traditional conveyors would be impractical due to the need to navigate obstacles or uneven terrain. Operational considerations for these systems include the selection of appropriate air compressor capacity, the design of the pipeline to minimize pressure drop and material deposition, and the use of appropriate filters and separators to maintain air quality and prevent system blockages. Proper maintenance, including regular cleaning of the pipeline and replacement of worn components, is essential to ensure the system operates efficiently and reliably over its service life.
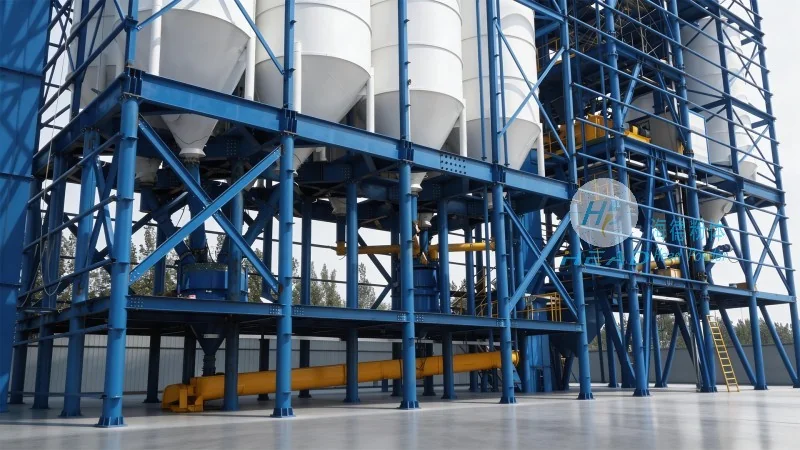
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer and supplier of pneumatic conveying systems and related industrial equipment. With a focus on innovation and quality, the company has established itself as a trusted partner in the material handling industry, providing customized solutions tailored to the specific needs of clients. Headpowder's products are designed to meet the highest standards of performance, durability, and efficiency, ensuring reliable operation in demanding industrial environments. The company's commitment to customer satisfaction and technical excellence has earned it a reputation for delivering solutions that enhance productivity and reduce operational costs for its clients. Headpowder serves clients across various industries, including construction, mining, and manufacturing, and is dedicated to providing comprehensive support, from system design and installation to maintenance and after-sales service.




