Understanding the fly ash particle material conveying system is crucial for industries dealing with fly ash, a byproduct of coal combustion. This system is engineered to efficiently transport fly ash particles, which are often used in construction materials, cement production, and other industrial applications. The design of such a system involves several key principles that ensure optimal performance, safety, and reliability.
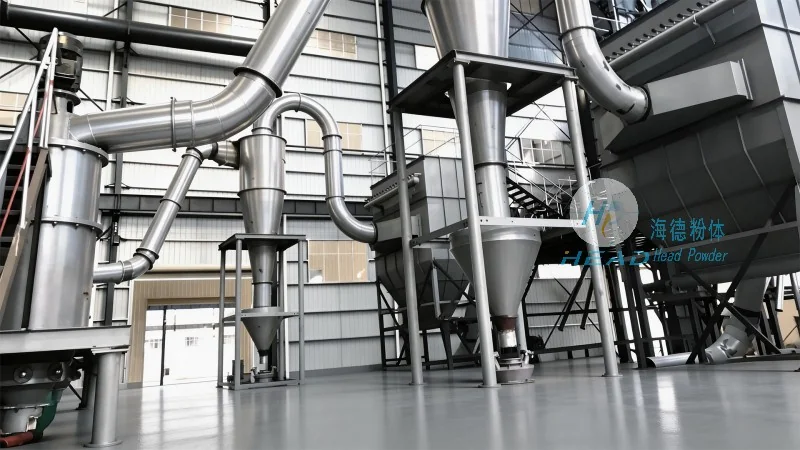
Key Design Principles of Fly Ash Particle Material Conveying Systems
The design of a fly ash particle material conveying system is based on several fundamental principles that address the unique characteristics of fly ash particles. These principles include material handling efficiency, system durability, and environmental compliance. The system typically incorporates components like hoppers, feeders, conveyors, and control systems, each designed to work in harmony to achieve seamless material transport. The selection of materials for the system components is critical, as fly ash particles can be abrasive and corrosive, requiring durable materials like stainless steel or special alloys to prevent wear and tear.
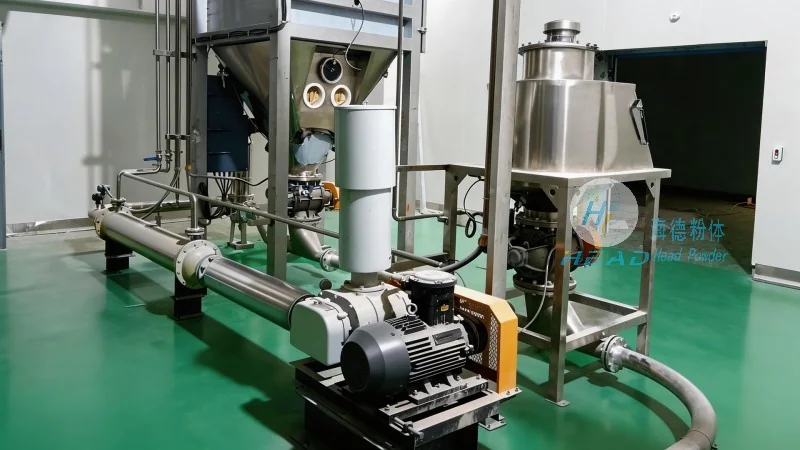
Components and Their Functions in the Conveying System
A typical fly ash particle material conveying system consists of several interconnected components, each playing a vital role in the overall operation. The hopper is the initial storage unit where raw fly ash is collected. It is designed with a sloped bottom to facilitate the flow of particles into the feeder. The feeder, often a rotary or vibratory type, regulates the flow rate of fly ash from the hopper to the conveyor. The conveyor, which can be a belt, screw, or pneumatic type, transports the fly ash particles from the feeder to the discharge point. Control systems, including sensors and automation equipment, monitor the system's performance and adjust parameters as needed to maintain consistent operation. These components work together to ensure that the fly ash is conveyed safely and efficiently, minimizing downtime and maximizing throughput.
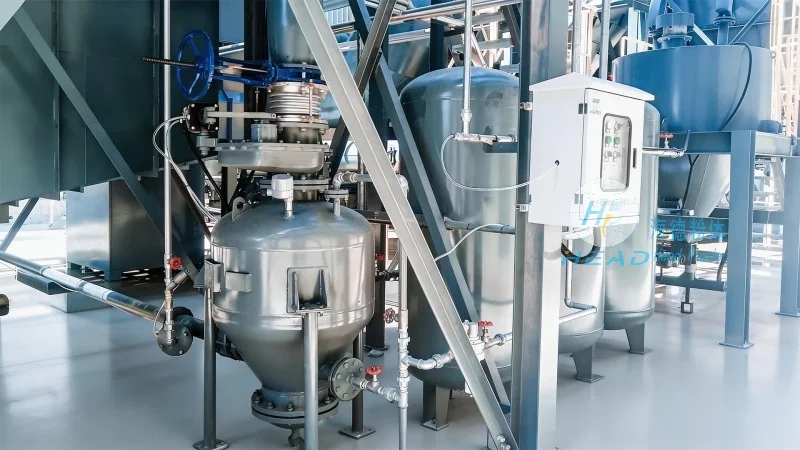
HeadPowder's Expertise in Fly Ash Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of specialized engineering solutions for fly ash handling and conveying. With years of experience in the industry, HeadPowder has developed advanced systems that meet the stringent requirements of modern industrial applications. The company's team of engineers and technicians specializes in designing and manufacturing custom conveying systems tailored to the specific needs of clients, ensuring optimal performance and reliability. HeadPowder's commitment to quality and innovation has made it a trusted partner for many industries, including power plants, cement manufacturers, and construction material producers. The company's headquarters is located in Shandong, China, where it operates a state-of-the-art research and development facility, enabling continuous improvement and the development of cutting-edge technologies.




