Ammonia fertilizer material handling systems are critical components in the agricultural and chemical industries, designed to safely and efficiently transport ammonia-based fertilizers from storage to application points. These systems are engineered to handle the unique properties of ammonia, such as its corrosive nature and high vapor pressure, ensuring operational safety and product integrity. Understanding the design principles behind these systems is essential for optimizing performance, minimizing risks, and meeting industry standards.
Key Components of Ammonia Fertilizer Material Handling Systems
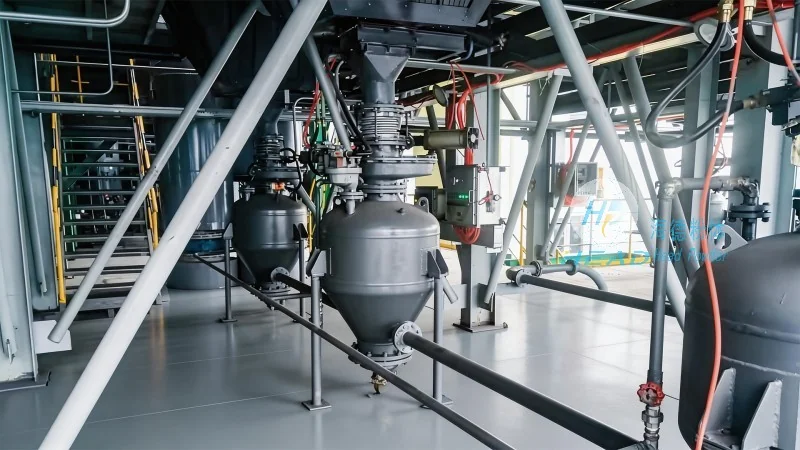
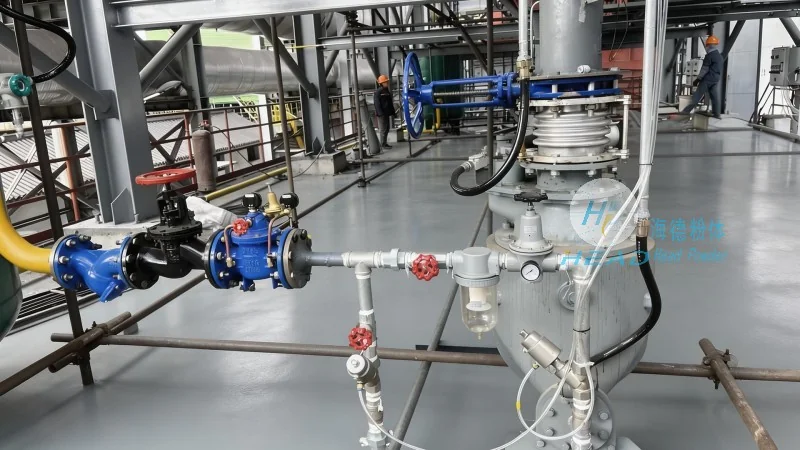
At the core of an ammonia fertilizer material handling system are several key components that work in tandem to ensure smooth operation. The primary components include storage tanks, pumps, pipelines, valves, and safety devices. Storage tanks are typically made of corrosion-resistant materials like stainless steel or lined carbon steel to withstand the chemical properties of ammonia. Pumps, often centrifugal or positive displacement types, are used to move the liquid ammonia through the system. Pipelines are designed with appropriate diameters and materials to handle the flow rates and pressures required. Valves control the flow direction and pressure, while safety devices such as pressure relief valves and leak detectors are integrated to prevent accidents and ensure compliance with safety regulations.
Design Principles for Safety and Efficiency
The design of ammonia fertilizer material handling systems prioritizes both safety and efficiency. Safety is paramount due to the hazardous nature of ammonia, which can cause severe burns and environmental damage if mishandled. Design principles include the use of explosion-proof equipment, proper ventilation systems, and emergency shutdown procedures. Efficiency is achieved through optimized flow rates, minimal pressure drops, and energy-efficient pump selection. Engineers also consider factors like material compatibility, temperature control, and maintenance accessibility to ensure long-term reliability. The system design must adhere to international standards such as ASME, API, and local regulations to guarantee compliance and operational safety.
HeadPowder Engineering's Expertise in Ammonia Fertilizer Handling
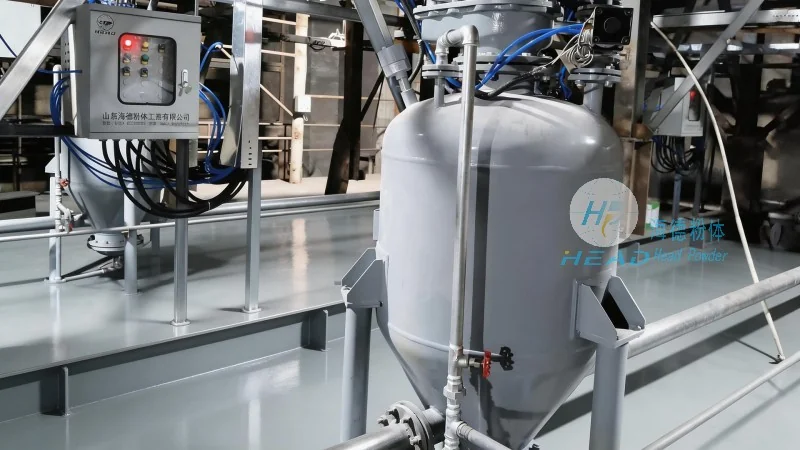
Shandong HeadPowder Engineering Co., Ltd., a leading provider in the field, specializes in designing and manufacturing ammonia fertilizer material handling systems tailored to client needs. With a focus on safety, efficiency, and durability, HeadPowder's solutions are built to meet the demanding requirements of the agricultural and chemical sectors. The company's team of experienced engineers utilizes advanced design software and rigorous testing protocols to ensure that each system is optimized for performance and reliability. HeadPowder's commitment to quality and customer satisfaction has made it a trusted partner for businesses seeking reliable ammonia fertilizer handling solutions. The company's facilities in Shandong, China, are equipped with state-of-the-art technology and skilled workforce, enabling the production of high-quality systems that adhere to international standards.
Conclusion
Ammonia fertilizer material handling systems are complex and critical infrastructure in the fertilizer industry, requiring careful design and engineering to ensure safety and efficiency. The design principles outlined above, combined with the expertise of companies like Shandong HeadPowder Engineering Co., Ltd., contribute to the development of reliable systems that support agricultural productivity while minimizing risks. As the demand for ammonia-based fertilizers continues to grow, the importance of robust material handling systems becomes increasingly evident, making them a vital component of modern agricultural operations.




