When it comes to industrial material handling, especially in the context of ash management from power plants or similar facilities, the purified ash material handling system stands out as a critical component. This system is engineered to efficiently transport ash materials while ensuring environmental safety and operational efficiency. At Shandong HeadPowder Engineering Co., Ltd., we specialize in the design, development, and implementation of such systems, leveraging years of expertise in material handling technologies.
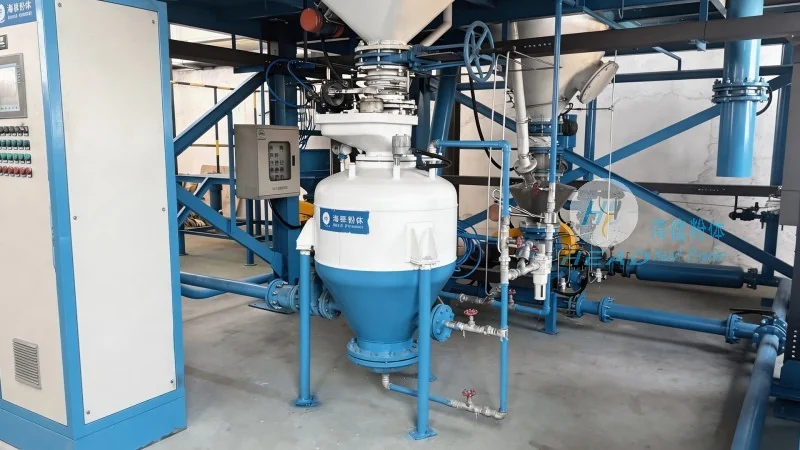
Key Components and Functionalities of the System
The purified ash material handling system typically comprises several key components that work in tandem to achieve optimal performance. These include ash collection hoppers, conveyor belts or screw conveyors, dust collection and filtration systems, and control panels for automated operation. The primary function is to collect ash from its source, transport it to a designated storage or processing area, and minimize the release of airborne particles to protect both the environment and personnel. The system is designed with robust materials to withstand the abrasive nature of ash and the harsh conditions of industrial environments.
Design Principles Behind the System
The design principles of a purified ash material handling system are centered on efficiency, safety, and sustainability. One of the core principles is the use of enclosed and sealed transport mechanisms to prevent dust emissions. This is achieved through the integration of dust collection systems that capture and filter particles before they are released into the atmosphere. Another key principle is the optimization of material flow to minimize energy consumption and operational costs. Engineers at HeadPowder carefully calculate the conveyor speed, load capacity, and system layout to ensure that the system operates at peak efficiency without unnecessary energy waste. Additionally, the system is designed for easy maintenance and scalability, allowing for adjustments as operational needs change over time.
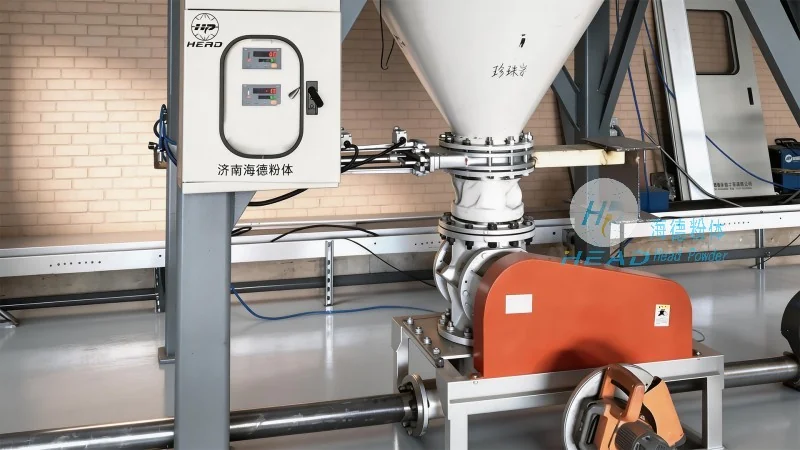
Material Handling Capabilities and Environmental Compliance
HeadPowder's purified ash material handling systems are built to handle various types of ash, including fly ash, bottom ash, and boiler ash, with different particle sizes and moisture content. The system's flexibility allows it to adapt to different ash characteristics, ensuring consistent performance. Environmental compliance is a top priority, and the system is engineered to meet or exceed local and international environmental standards. The dust filtration and collection systems are designed to capture a high percentage of particulate matter, reducing the environmental impact of ash handling operations. This not only protects the surrounding ecosystem but also helps companies maintain a positive public image and comply with regulatory requirements.
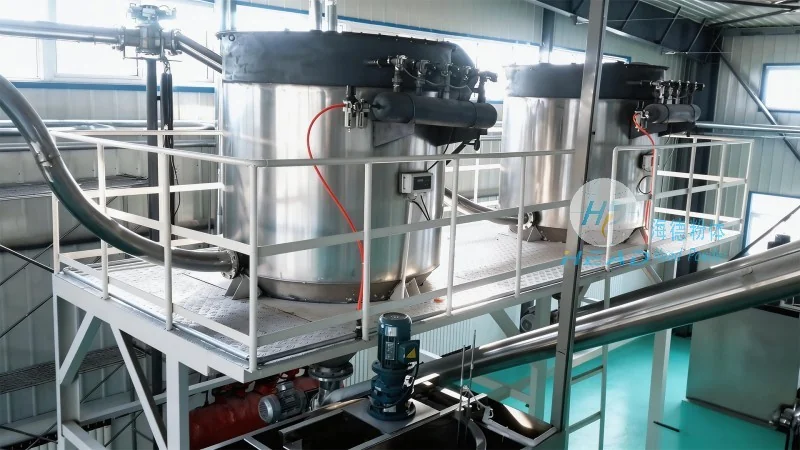
Customization and Integration with Existing Infrastructure
At Shandong HeadPowder Engineering Co., Ltd., we understand that each industrial facility has unique requirements. Therefore, our purified ash material handling systems are highly customizable to fit specific site conditions and operational needs. We work closely with clients to assess their current infrastructure, ash generation rates, and storage capabilities to design a system that integrates seamlessly with existing equipment. This approach minimizes disruption during installation and ensures a smooth transition to the new material handling solution. Our team of engineers and technicians provides comprehensive support throughout the entire process, from initial design and engineering to installation and post-installation maintenance.
Benefits of Implementing a Purified Ash Material Handling System
Adopting a purified ash material handling system offers numerous benefits for industrial facilities. Firstly, it enhances operational efficiency by streamlining the ash transport process, reducing downtime and increasing overall productivity. Secondly, it improves safety by minimizing exposure to airborne dust and other hazardous particles, protecting the health of workers. Thirdly, it contributes to environmental sustainability by reducing emissions and complying with environmental regulations. Additionally, the system's robust design and quality components lead to lower maintenance costs and longer service life, providing a better return on investment over time. For companies looking to modernize their ash handling operations, a purified ash material handling system from HeadPowder is a reliable and effective solution.




