Borax, also known as sodium tetraborate, is a widely used chemical compound in various industrial applications, including glass manufacturing, detergents, and agricultural uses. The efficient handling and transportation of borax are crucial for industrial operations to maintain productivity and safety. A borax material handling system is a specialized setup designed to manage the flow of borax from storage to processing or packaging units. This system integrates various components such as conveyors, storage silos, and feeding mechanisms to ensure smooth and controlled movement of the material.
Understanding the Core Components of a Borax Material Handling System
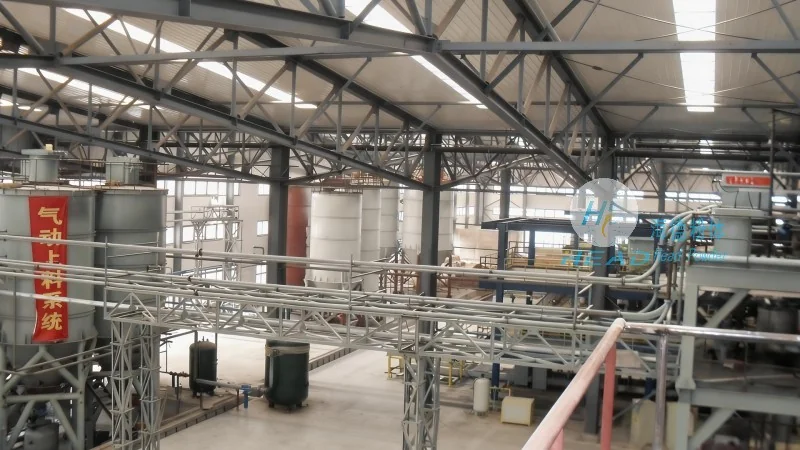
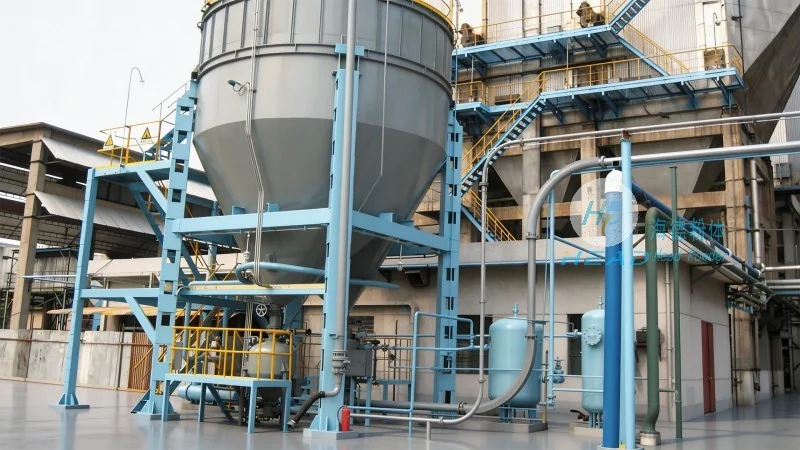
The design of a borax material handling system is built around several key components that work in tandem to achieve optimal performance. The primary components include bulk storage silos, which are used to store large quantities of borax, often in a dry or slurry form. These silos are typically made of durable materials like steel or reinforced concrete to withstand the chemical properties of borax and prevent contamination. The storage silos are equipped with agitators or mixers to maintain the consistency of the material, especially when handling borax in a slurry state. This ensures that the material remains free-flowing and does not settle or clog the system.
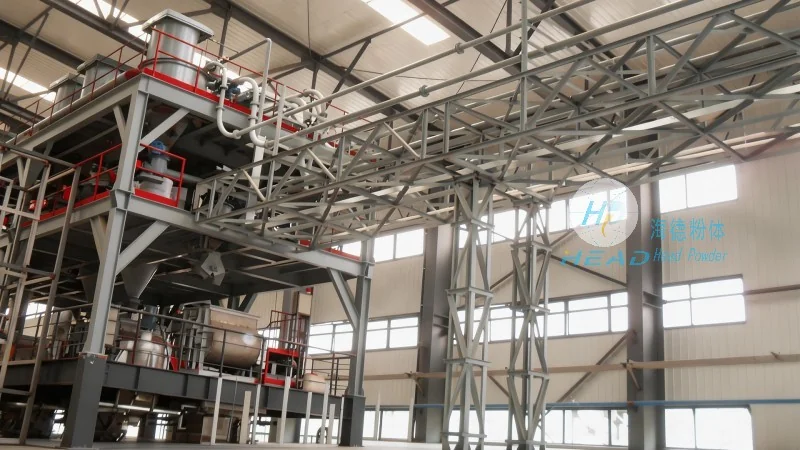
From the storage silos, the borax is transferred to the processing area through a network of conveyors. The most common types of conveyors used in borax handling include belt conveyors, screw conveyors, and pneumatic conveyors. Belt conveyors are ideal for transporting bulk quantities of dry borax over long distances, providing a reliable and cost-effective solution. Screw conveyors, on the other hand, are suitable for vertical or inclined transport, making them useful for moving borax between different levels of a facility. Pneumatic conveyors use air pressure to transport borax in a dry or slurry form, offering flexibility in layout and the ability to handle fine powders without the need for mechanical contact.
Design Principles for Efficient Borax Material Handling
The design principles of a borax material handling system focus on several critical factors to ensure efficiency, safety, and durability. One of the key principles is the minimization of material degradation and contamination. Borax is a sensitive chemical that can degrade or react with other substances if not handled properly. Therefore, the system is designed with materials that are chemically inert and resistant to corrosion, such as stainless steel or specialized coatings. The components are also sealed to prevent dust and moisture from entering, which can affect the quality of the borax and lead to operational issues.
Another important design principle is the prevention of blockages and clogging. Borax, especially when in a fine powder form, can be prone to bridging or agglomeration in storage silos and conveyors. To address this, the system incorporates features like vibration devices, air cannons, and rotary valves. These devices help to break up any clumps or bridging material, ensuring a consistent flow of borax through the system. The design also considers the flow characteristics of borax, using appropriate angles and slopes in the silos and conveyors to promote smooth movement and prevent stagnation.
Control Systems and Automation in Borax Material Handling
Modern borax material handling systems often incorporate advanced control systems and automation to enhance operational efficiency and safety. These systems use sensors and monitoring equipment to track the level of borax in the storage silos, the flow rate through the conveyors, and the pressure in the pneumatic lines. The data collected by these sensors is processed by a central control unit, which can adjust the operation of the system in real-time. For example, if the level of borax in a silo drops below a certain threshold, the control system can automatically initiate the transfer of material from another silo or from an external source. This automation reduces the need for manual intervention and minimizes the risk of human error.
Automation also plays a role in safety measures. The system may include alarms and interlocks to prevent overfilling of silos or excessive pressure in the conveyors. These safety features are crucial in handling borax, as any malfunction could lead to spills, dust explosions, or other hazardous situations. The control systems are typically designed to comply with industry standards and regulations, ensuring that the operation of the borax material handling system is safe and compliant.
HeadPowder's Expertise in Borax Material Handling Solutions
Shandong HeadPowder Engineering Co., Ltd., a leading provider of material handling solutions, specializes in designing and manufacturing borax material handling systems tailored to the specific needs of industrial clients. With years of experience in the field, HeadPowder understands the unique challenges of handling borax and has developed innovative solutions to address them. The company's team of engineers and technicians work closely with clients to assess their operational requirements, material characteristics, and safety standards, ensuring that the final system is both efficient and reliable.
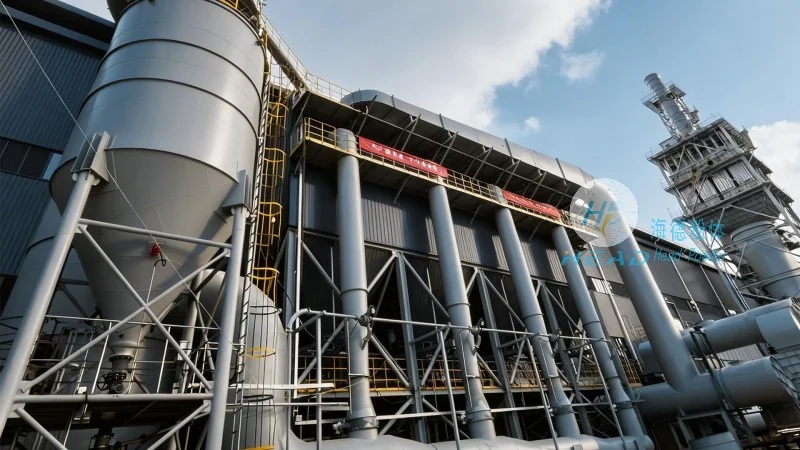
HeadPowder's borax material handling systems are designed with a focus on durability and low maintenance. The components are built to withstand the harsh conditions of industrial environments, including high temperatures, chemical exposure, and heavy usage. The company uses high-quality materials and advanced manufacturing techniques to ensure that the systems have a long service life and minimal downtime. Additionally, HeadPowder provides comprehensive support services, including installation, commissioning, and maintenance, to ensure that the borax material handling system operates at peak performance throughout its lifecycle.
Conclusion: The Importance of a Well-Designed Borax Material Handling System
In conclusion, a borax material handling system is a critical component of industrial operations that handle borax. The design of such a system must consider the unique properties of borax, including its chemical stability, flow characteristics, and potential for degradation. By integrating appropriate components, control systems, and safety features, a well-designed borax material handling system can significantly improve operational efficiency, reduce costs, and enhance safety. Companies like Shandong HeadPowder Engineering Co., Ltd. play a vital role in providing these specialized solutions, helping industrial clients to optimize their borax handling processes and achieve their business objectives.




