Ammonium sulfate is a widely used chemical compound in various industrial applications, and its efficient handling through powder conveying systems is crucial for maintaining production efficiency and safety. This article explores the fundamental aspects of ammonium sulfate powder conveying, focusing on the design principles that underpin effective material transport.
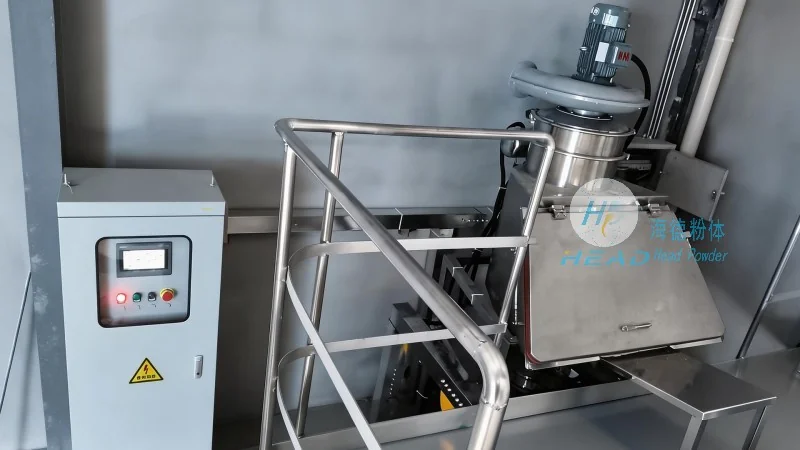
HeadPowder: A Leader in Powder Handling Solutions
Shandong HeadPowder Engineering Co., Ltd., based in Shandong, China, specializes in providing advanced powder conveying systems tailored to the unique needs of chemical processing industries. With a deep understanding of material properties and industrial requirements, HeadPowder offers customized solutions that enhance the performance and reliability of ammonium sulfate handling operations.
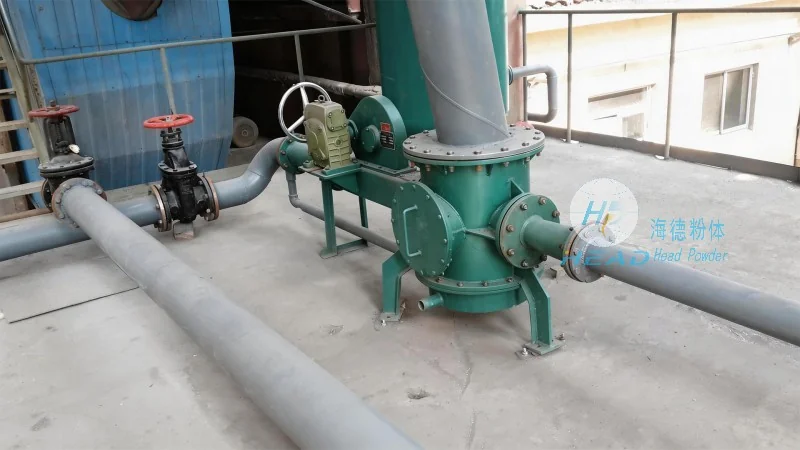
Key Design Principles for Ammonium Sulfate Powder Conveying Systems
The design of an ammonium sulfate powder conveying system involves several critical factors that ensure optimal performance. These include the selection of appropriate equipment such as screw conveyors, pneumatic conveyors, or bucket elevators, which are chosen based on the material's flow characteristics, density, and moisture content. For ammonium sulfate, which is a fine, free-flowing powder, screw conveyors are often preferred due to their ability to handle dry powders without causing excessive friction or degradation. The system layout also plays a vital role, as it must consider factors like space constraints, material flow direction, and integration with other processing equipment. Proper sealing and dust control measures are essential to prevent contamination and ensure compliance with environmental regulations. Additionally, the control system must be robust, allowing for real-time monitoring of pressure, flow rate, and temperature to maintain consistent operation and prevent blockages or overloading.
Addressing Challenges in Ammonium Sulfate Handling
Handling ammonium sulfate presents unique challenges due to its hygroscopic nature and potential for caking. To mitigate these issues, conveying systems often incorporate features like temperature control, anti-caking agents, or vibration mechanisms to maintain material flowability. The design must also consider the material's reactivity with other substances or equipment components, ensuring that all parts of the system are compatible and resistant to corrosion or chemical attack. Regular maintenance and cleaning protocols are essential to prevent the buildup of residue, which can affect system efficiency and product quality. HeadPowder's expertise in material science and engineering allows them to address these challenges effectively, providing systems that are both durable and reliable.
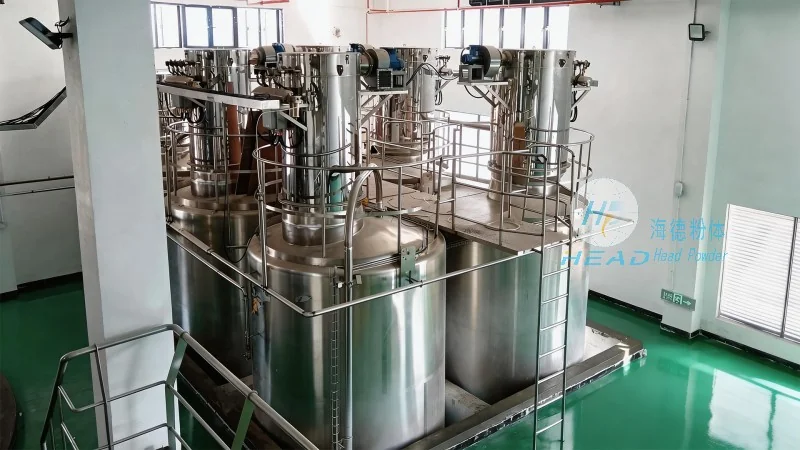
Conclusion: Optimizing Ammonium Sulfate Conveying with HeadPowder
Efficient ammonium sulfate powder conveying is a critical component of modern chemical processing operations, and the design principles outlined above are essential for achieving optimal performance. By leveraging advanced technology and a deep understanding of material behavior, companies like Shandong HeadPowder Engineering Co., Ltd. can provide tailored solutions that enhance productivity, reduce downtime, and ensure compliance with industry standards. Whether for bulk storage, processing, or distribution, the right conveying system can significantly impact the overall success of an operation. With a focus on quality, innovation, and customer satisfaction, HeadPowder continues to be a trusted partner in the development of reliable powder handling systems for industries worldwide.




