For industries dealing with diatomite mineral powders, the selection and understanding of pneumatic conveying systems are critical for efficient material handling. This article explores the diatomite mineral powder pneumatic conveying system equipment, detailing its components, operational principles, and the design considerations that ensure optimal performance. By examining the technology behind these systems, readers will gain insights into how such equipment enhances productivity and maintains material integrity in processing applications.
Introduction to Diatomite Mineral Powder Pneumatic Conveying Systems
Diatomite, a natural sedimentary rock composed primarily of fossilized diatoms, is widely used in various industries due to its unique properties, including high porosity, low density, and excellent filtering capabilities. In processing diatomite, the handling of its fine powder form requires specialized equipment to prevent dust accumulation, ensure consistent flow, and maintain product quality. Pneumatic conveying systems offer a solution by transporting powders through a pressurized or vacuum environment using air or other gases. This method is particularly advantageous for diatomite, as it minimizes contamination, reduces labor costs associated with manual handling, and enables seamless integration into automated production lines.
Key Components of the Pneumatic Conveying System
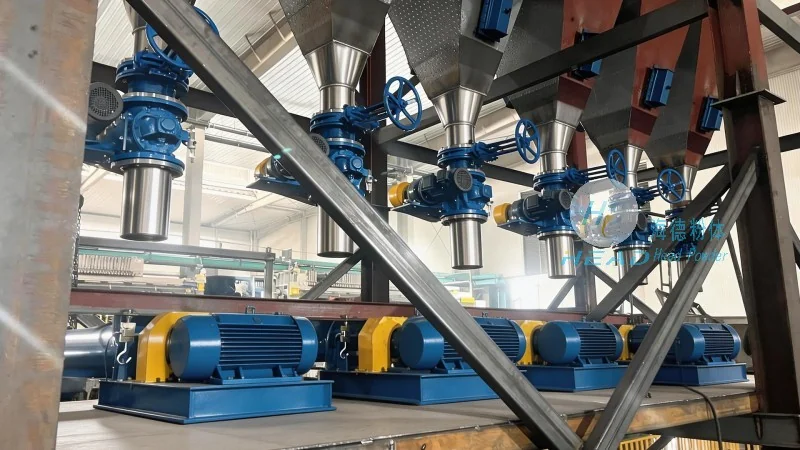
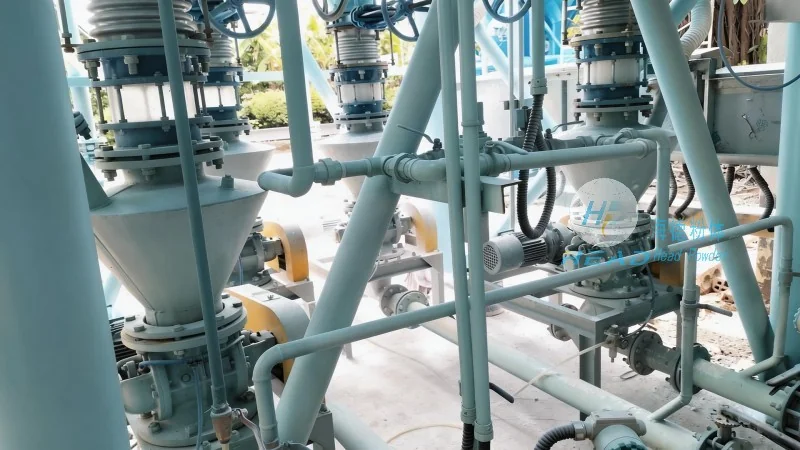
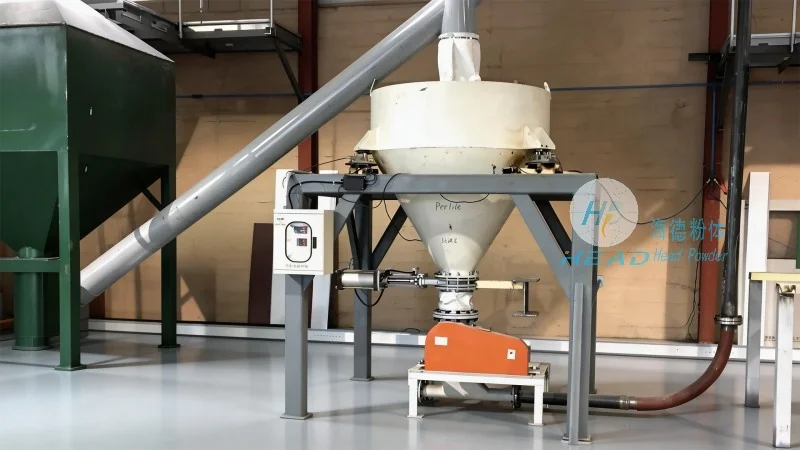
The diatomite mineral powder pneumatic conveying system typically consists of several interconnected components, each playing a vital role in the overall operation. The primary elements include the hopper or feed bin, which stores the diatomite powder and regulates its discharge into the system. A rotary valve or feeder is often used to control the flow rate of the material, ensuring a steady supply to the conveying line. The conveying line itself, made of materials resistant to abrasion and corrosion (such as stainless steel or special plastics), transports the powder under pressure or vacuum. At the receiving end, a silo or storage tank collects the material, while a dust collector or filter system removes any entrained particles from the air, ensuring compliance with environmental regulations and maintaining air quality. Additionally, control panels and sensors are integrated to monitor pressure, flow rates, and system performance, allowing for real-time adjustments and troubleshooting.
Design Principles for Efficient Pneumatic Conveying
The design of a diatomite mineral powder pneumatic conveying system is based on several key principles to ensure efficiency, reliability, and cost-effectiveness. The first principle is the selection of the appropriate conveying method—either pressure or vacuum. Pressure systems use a blower or compressor to push air and powder through the line, while vacuum systems use a vacuum pump to draw material from the source. For diatomite, pressure systems are often preferred due to their ability to handle higher material loads and longer distances without significant pressure drop. The design also considers the particle size and density of the diatomite, as these factors influence the required air velocity and pressure to maintain a stable flow. Engineers must calculate the necessary air volume and pressure to overcome friction losses in the conveying line and ensure the powder remains suspended in the air stream. This involves determining the appropriate velocity (typically between 20-30 m/s for fine powders) and pressure (ranging from 0.5 to 2 bar) to prevent particle settling or blockages.
Advantages of Using Pneumatic Conveying for Diatomite
Implementing a pneumatic conveying system for diatomite mineral powders offers numerous advantages over traditional methods like bucket elevators or belt conveyors. One of the most significant benefits is the reduction of dust exposure, which not only improves workplace safety but also maintains the purity of the material. Unlike mechanical systems that can generate dust through friction or impact, pneumatic conveying keeps the powder enclosed within the system, minimizing environmental impact and product contamination. Another advantage is the ability to handle fine, abrasive powders without causing wear and tear on equipment components. Diatomite is known for its abrasive nature, and pneumatic systems use smooth, corrosion-resistant materials that resist erosion, extending the lifespan of the equipment. Furthermore, pneumatic conveying systems are highly flexible, allowing for changes in material flow rates and line configurations without major modifications. This adaptability is crucial for industries that may need to process different grades of diatomite or adjust production volumes based on market demand.
Application Examples in Diatomite Processing
Diatomite mineral powder pneumatic conveying systems are widely used in various processing stages, from raw material handling to finished product packaging. In mining operations, the system can transport mined diatomite from storage bins to crushing and grinding equipment, ensuring a continuous supply of raw material. During the grinding process, the system efficiently conveys the fine powder to classification and screening units, where it is separated into different particle sizes for further processing. In the filtration industry, diatomite is often used as a filter aid, and pneumatic conveying systems deliver the powder to filter presses or other filtration equipment, maintaining consistent filter cake formation and improving filtration efficiency. Additionally, in the production of diatomite-based products like activated carbon or catalysts, the system ensures that the powder is delivered to mixing and extrusion units without agglomeration, preserving the material's properties. These applications highlight the versatility and importance of pneumatic conveying systems in optimizing diatomite processing workflows.
Maintenance and Operational Considerations
To ensure the long-term performance and reliability of a diatomite mineral powder pneumatic conveying system, proper maintenance and operational practices are essential. Regular inspections of the conveying line, rotary valves, and air filters are necessary to detect and address any wear or blockages. The system should be cleaned periodically to remove accumulated powder, which can reduce airflow and increase pressure drop. Additionally, monitoring the air pressure and flow rates helps identify potential issues before they lead to system failures. For abrasive diatomite powders, using wear-resistant materials for components like the hopper and conveying line is crucial to extend equipment life. Proper training for operators on system operation and troubleshooting is also vital to prevent downtime and ensure safe operation. By following these maintenance guidelines, industries can maximize the efficiency and lifespan of their pneumatic conveying systems, reducing operational costs and maintaining product quality.
Conclusion
In conclusion, the diatomite mineral powder pneumatic conveying system equipment is a sophisticated solution for handling fine, abrasive powders in industrial applications. By understanding its design principles, key components, and operational advantages, industries can select and implement systems that enhance productivity, maintain material integrity, and ensure workplace safety. As a leading provider in this field, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing customized pneumatic conveying systems tailored to the specific needs of diatomite processing facilities. With a focus on efficiency, reliability, and environmental compliance, these systems play a critical role in modern diatomite processing operations, supporting the growth and sustainability of industries that rely on this valuable mineral.




