Wheat flour pneumatic conveying systems are essential in modern flour milling and processing operations, offering efficient and reliable methods for transporting bulk wheat flour and other fine powders. This article explores the fundamental principles behind these systems, highlighting their design, operation, and key advantages in industrial applications.
Company Introduction
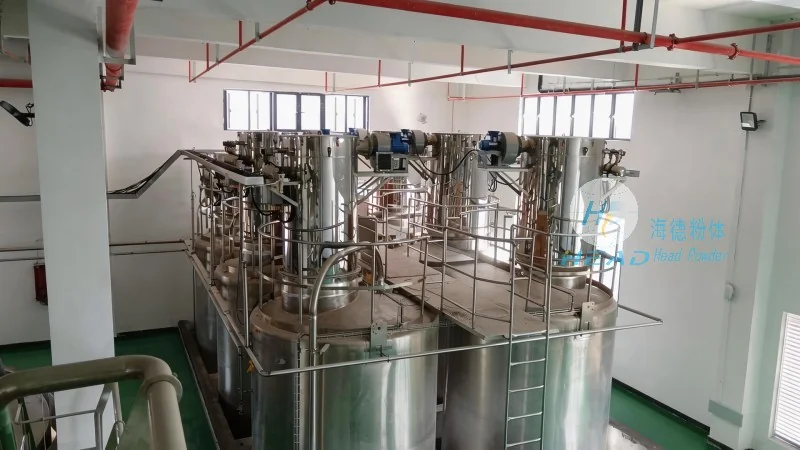
HeadPowder, a leading manufacturer in the field, specializes in the design, development, and implementation of advanced pneumatic conveying solutions. As a subsidiary of Shandong HeadPowder Engineering Co., Ltd., based in Shandong, China, the company leverages over a decade of industry experience to deliver high-performance systems tailored to the specific needs of flour mills and food processing facilities worldwide.
The Core Principle of Pneumatic Conveying
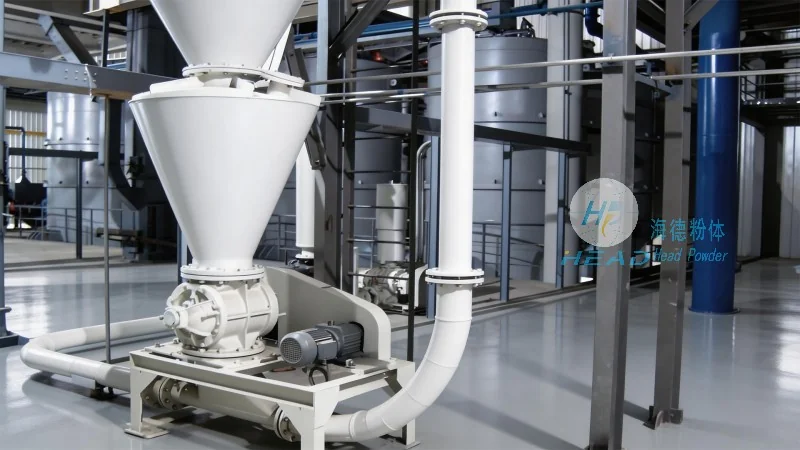
Pneumatic conveying systems operate on the principle of using air or gas to transport solid materials through a pipeline. In the case of wheat flour, the system typically employs a positive pressure or negative pressure (vacuum) method to move the fine powder from a source, such as a silo or storage bin, to a destination like a processing line or packaging area. The process involves creating a pressure differential that propels the flour particles along the pipeline, often with the assistance of airlocks, cyclones, or other separation devices to ensure efficient and clean transport.
Key Technical Features
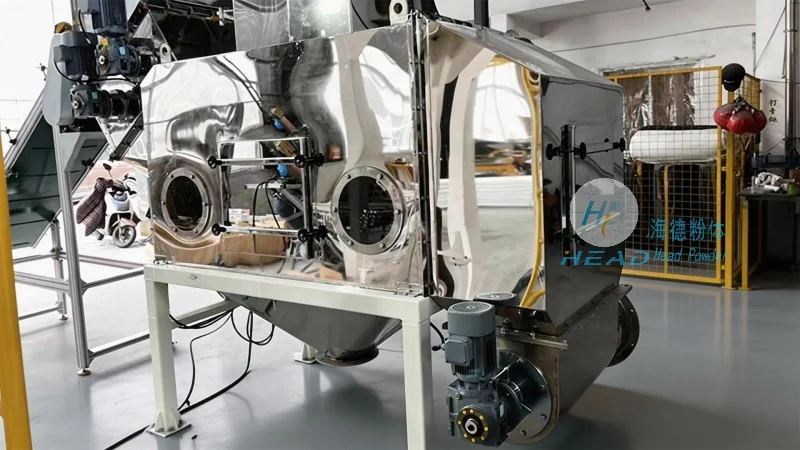
Modern wheat flour pneumatic conveying systems from HeadPowder are equipped with several advanced features that enhance performance and reliability. These include variable speed air blowers to control airflow and pressure, which allows for precise regulation of flour flow rates. Additionally, the systems incorporate high-efficiency filters and dust collection units to maintain air quality and comply with environmental regulations. The use of corrosion-resistant materials, such as stainless steel, ensures durability and longevity, even in harsh industrial environments where flour and moisture may be present.
Applications and Benefits
The applications of wheat flour pneumatic conveying systems are widespread across the food processing industry. They are commonly used in flour mills to transfer raw wheat flour from storage silos to milling equipment, in bakery operations to move flour to mixing and baking lines, and in food manufacturing facilities to distribute flour for various product formulations. The primary benefits of these systems include improved safety by eliminating manual handling of bulk flour, increased efficiency through automated and continuous operation, and reduced product contamination due to enclosed and sealed transport pathways.
Quality Assurance and Reliability
HeadPowder places a strong emphasis on quality and reliability in all its pneumatic conveying systems. Each system is rigorously tested and validated to meet industry standards and customer specifications. The company’s commitment to using high-quality components and employing skilled engineering teams ensures that the systems operate with minimal downtime and maximum efficiency. Furthermore, HeadPowder provides comprehensive after-sales support, including maintenance services and technical assistance, to ensure that clients can maximize the lifespan and performance of their wheat flour pneumatic conveying systems.




