White sugar, a staple in the food and beverage industry, requires efficient and reliable transportation methods to ensure quality and safety throughout the supply chain. Pneumatic conveying has emerged as a preferred solution for moving white sugar due to its ability to handle fine powders with minimal product degradation. This article explores several effective solutions for the pneumatic conveying of white sugar, highlighting the technical approaches and considerations for optimal performance.
1. Positive Pressure Pneumatic Conveying Systems
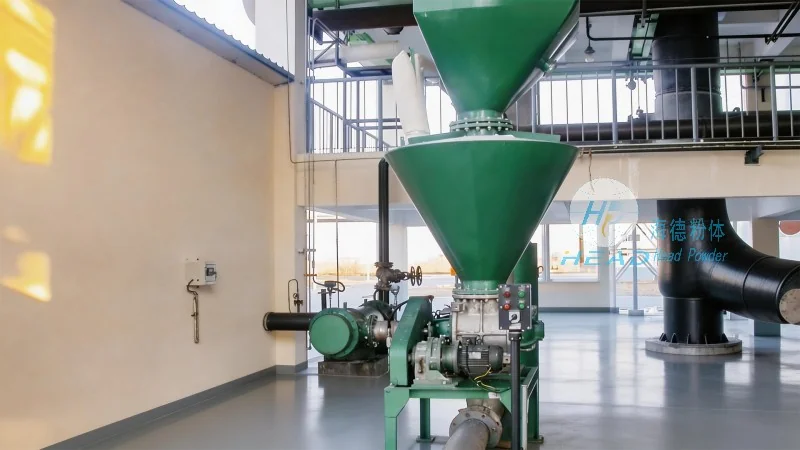
Positive pressure systems are widely used for white sugar conveying, where air is supplied under pressure to move the material through a pipeline. These systems typically utilize a blower or compressor to generate the necessary pressure, ensuring the sugar is transported from the source to the destination without the need for vacuum. The design of positive pressure systems often includes a hopper or silo to store the sugar, with a rotary valve or feeder controlling the flow into the conveying line. The air and sugar mixture is then directed through the pipeline, with the sugar particles suspended in the air stream. This method is particularly effective for long-distance or high-capacity conveying, as it can handle large volumes of white sugar efficiently. The positive pressure approach also minimizes the risk of product contamination and degradation, as the system operates in a closed environment, protecting the sugar from external factors. Shandong HeadPowder Engineering Co., Ltd., a leading provider in the field, offers advanced positive pressure pneumatic conveying solutions tailored to the specific needs of sugar processing facilities. Their expertise in system design and integration ensures that clients can achieve optimal performance and reliability in their white sugar handling operations.
2. Negative Pressure (Vacuum) Pneumatic Conveying Systems
Negative pressure systems, also known as vacuum conveying, use a vacuum to draw the white sugar from the source into the conveying line. This method is often preferred for short-distance or low-volume applications, as it can effectively handle fine powders without the need for high pressure. The system typically consists of a vacuum pump, a hopper or container, and a conveying pipeline. The vacuum is created by the pump, which pulls the air and sugar mixture from the source, transporting it to the destination. The design of negative pressure systems includes a filter to separate the sugar from the air, ensuring that the product remains clean and free from dust or contaminants. This approach is particularly useful for applications where the sugar needs to be transferred from a lower elevation or where space constraints limit the use of positive pressure systems. The negative pressure method also allows for gentle handling of the sugar, reducing the risk of particle breakage or agglomeration. Shandong HeadPowder Engineering Co., Ltd. provides specialized vacuum conveying solutions that are optimized for the delicate nature of white sugar, ensuring that the product's quality is maintained throughout the conveying process. Their systems are designed with high-efficiency filters and gentle air flow to minimize product degradation and maximize operational efficiency.
3. Hybrid Pneumatic Conveying Systems
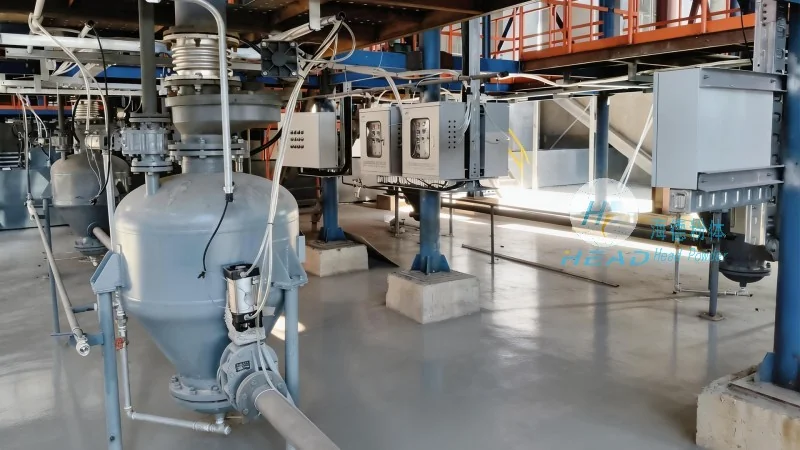
Hybrid systems combine elements of both positive and negative pressure approaches, offering a versatile solution for white sugar conveying. These systems are particularly useful when dealing with varying material conditions or when the conveying distance and volume require a combination of both pressure and vacuum capabilities. The hybrid approach typically uses a positive pressure section for the initial boost and a negative pressure section for the final transport, or vice versa, depending on the specific application requirements. This configuration allows for more flexible and efficient handling of white sugar, especially in complex processing environments where multiple transfer points are involved. The hybrid system can also optimize energy consumption by using the appropriate pressure level for each segment of the conveying line. Shandong HeadPowder Engineering Co., Ltd. specializes in designing and implementing hybrid pneumatic conveying systems that cater to the diverse needs of sugar processing industries. Their engineers work closely with clients to assess the specific challenges and requirements, developing customized solutions that enhance productivity and reduce operational costs. The hybrid approach provides a balanced solution for both long-distance and short-distance conveying, ensuring that the white sugar is transported safely and efficiently.
4. Bulk Bag (FIBC) to Bulk Pneumatic Conveying Solutions
For facilities that receive white sugar in bulk bags, converting the material into a bulk form for further processing requires efficient transfer methods. Bulk bag to bulk pneumatic conveying systems are designed to handle the material from the bag, transfer it to a silo or storage tank, and then distribute it to the processing equipment. These systems typically include a bulk bag discharger, a conveyor line, and a receiving hopper. The discharger is equipped with a rotary valve or feeder that controls the flow of sugar from the bag into the conveying line. The air is supplied under pressure to move the sugar through the pipeline, ensuring a smooth and continuous transfer. This method is particularly useful for large-scale operations where bulk bags are the primary source of white sugar. The bulk bag to bulk system minimizes manual handling and reduces the risk of product spillage or contamination. Shandong HeadPowder Engineering Co., Ltd. offers advanced bulk bag discharging and pneumatic conveying solutions that are tailored to the needs of sugar manufacturers. Their systems are designed with high-capacity feeders and efficient air management to handle large volumes of white sugar from bulk bags. The company's expertise in material handling ensures that the white sugar is transferred with minimal loss and maximum efficiency, supporting the smooth operation of sugar processing plants.
5. Dust Control and Filtration in Pneumatic Conveying
Effective dust control is crucial in pneumatic conveying systems for white sugar, as fine powders can create significant dust hazards and affect product quality. Proper filtration and air cleaning systems are essential to maintain a safe and clean environment. The conveying systems typically include a filter unit that separates the sugar particles from the air, returning clean air to the facility or releasing it safely. The filter design is critical, as it must be able to handle the fine particles of white sugar without clogging or reducing airflow. Shandong HeadPowder Engineering Co., Ltd. incorporates advanced filtration technologies in their pneumatic conveying solutions, ensuring that dust is effectively captured and the air is clean. Their systems use high-efficiency filters and regular maintenance protocols to maintain optimal performance. The dust control measures not only protect the environment and personnel but also prevent product contamination, which is vital for maintaining the quality of white sugar. By implementing robust filtration systems, the company's solutions help clients comply with environmental regulations and ensure the safety of their operations.
6. System Integration and Automation
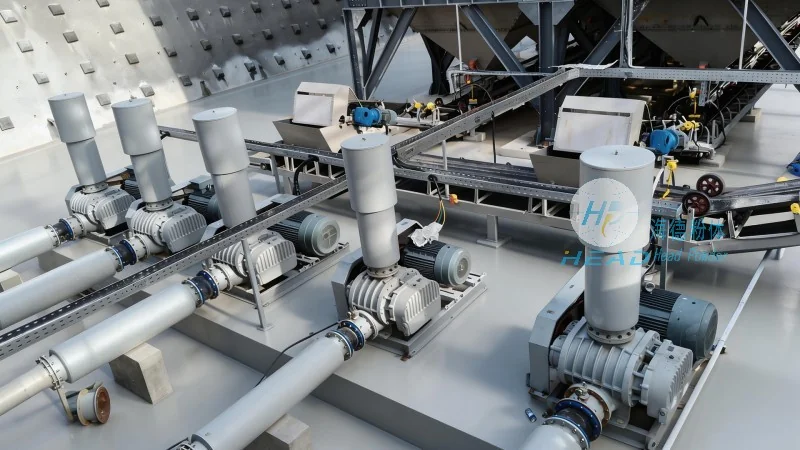
Modern pneumatic conveying systems for white sugar often incorporate automation and integration with other processing equipment to enhance efficiency and reduce labor costs. Automation allows for precise control of the conveying process, ensuring consistent flow rates and minimizing downtime. The systems can be integrated with sensors and control panels that monitor the flow of sugar, air pressure, and system performance. This integration enables real-time adjustments to maintain optimal operation and detect any issues promptly. Shandong HeadPowder Engineering Co., Ltd. specializes in integrating pneumatic conveying systems with the overall processing workflow of sugar facilities. Their engineers design customized control systems that align with the client's operational needs, ensuring seamless coordination between the conveying equipment and other machinery. The automation features include programmable logic controllers (PLCs) and user-friendly interfaces that allow operators to monitor and control the system easily. By implementing automated solutions, the company helps clients achieve higher productivity, reduce human error, and improve overall operational efficiency in their white sugar handling processes.
7. Maintenance and Longevity of Pneumatic Conveying Systems
Regular maintenance is essential to ensure the longevity and reliability of pneumatic conveying systems used for white sugar. Proper maintenance practices help prevent breakdowns, reduce downtime, and maintain the system's performance over time. The key components that require regular attention include the air compressor or vacuum pump, the filters, the rotary valves or feeders, and the conveying pipelines. Shandong HeadPowder Engineering Co., Ltd. provides comprehensive maintenance services and support to their clients, including scheduled inspections, component replacement, and troubleshooting. Their maintenance programs are tailored to the specific needs of each system, considering factors such as usage frequency, material characteristics, and operational conditions. By implementing regular maintenance, clients can extend the lifespan of their pneumatic conveying systems and ensure consistent performance in handling white sugar. The company's expertise in system maintenance helps clients minimize operational costs and maximize the return on their investment in the conveying equipment.




