For industries dealing with bulk materials like coal and sand, efficient material handling is crucial for operational efficiency and cost management. Pneumatic conveying lines offer a reliable solution to transport these materials over short to medium distances, ensuring minimal product degradation and reduced labor costs. This article delves into the operation process and working principles of a coal sand material pneumatic conveying line, highlighting key components, operational dynamics, and the technical advantages it provides.
Key Components of a Coal Sand Pneumatic Conveying Line
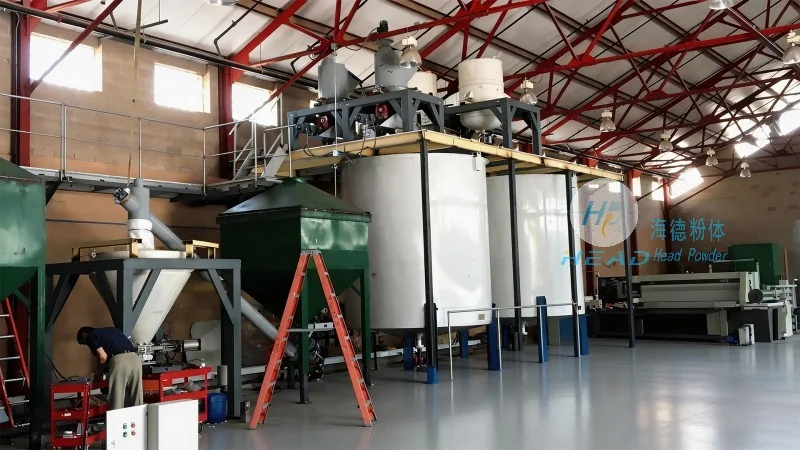
The core of any pneumatic conveying system is its component layout, which is tailored to handle the specific characteristics of coal and sand materials. A typical system includes several critical parts: a material hopper for storage and feeding, a rotary airlock valve to control the flow of material into the line, a main air duct that transports the material-air mixture, a dust separator or cyclone to separate the material from the air, and a discharge hopper for material collection. Each component plays a vital role in ensuring smooth and continuous operation. The material hopper is designed to accommodate bulk storage, allowing for consistent feeding without interruptions. The rotary airlock valve acts as a gate, preventing backflow and maintaining a steady flow rate. The main air duct, often made of stainless steel or other corrosion-resistant materials, is sized to handle the air velocity and material load. The dust separator efficiently separates the solid particles from the air stream, minimizing dust emissions and protecting downstream equipment. Finally, the discharge hopper collects the material after it has been separated from the air, ready for further processing or storage.
Working Principle of the Pneumatic Conveying Process
The operation of a coal sand pneumatic conveying line is based on the principle of air movement to transport solid materials. The process typically involves the following steps: First, the coal or sand material is fed into the material hopper from a storage silo or bin. The rotary airlock valve then opens to allow a controlled amount of material to enter the main air duct. Simultaneously, a high-pressure air blower or fan generates a strong air flow within the duct. As the material enters the duct, it is entrained by the air stream, forming a dense mixture of solid particles and air. This mixture travels through the air duct under the pressure of the air flow, reaching the dust separator. In the separator, the air stream is directed through a cyclone or other separation device, which uses centrifugal force to separate the solid particles from the air. The separated material is collected in the discharge hopper, while the clean air is either recirculated back into the system or released into the environment after filtration. The efficiency of this separation process is critical to maintaining system performance and minimizing dust pollution. The entire process is automated, with sensors and control systems monitoring parameters such as pressure, flow rate, and material level to ensure optimal operation. This continuous cycle allows for a steady and reliable supply of coal or sand to downstream processes, such as crushing, screening, or packaging.
Operation Process of the Coal Sand Pneumatic Conveying Line
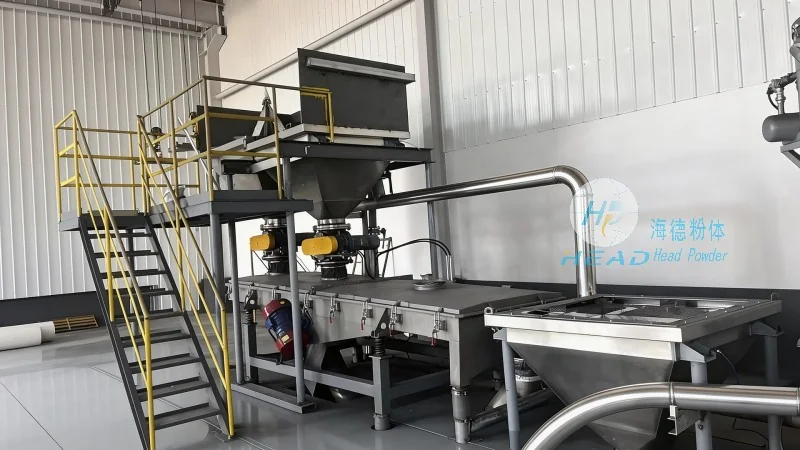
The operation process of a coal sand material pneumatic conveying line is a well-orchestrated sequence of events that ensures consistent material transport. The process begins with the loading of the material hopper. The hopper is typically filled from a bulk storage system, and its level is monitored by a sensor to prevent overfilling. Once the hopper is filled to the desired level, the rotary airlock valve opens, allowing material to flow into the main air duct. The air blower then starts, generating the necessary air pressure to entrain the material. The air velocity in the duct is carefully controlled to ensure that the material is fully suspended and transported without settling or blockages. As the material-air mixture travels through the duct, it passes through any necessary intermediate sections, such as bends or expansion joints, which are designed to minimize pressure loss and maintain flow stability. At the discharge end, the mixture enters the dust separator. The separator uses a combination of centrifugal force and gravity to separate the solid particles from the air. The separated material is collected in the discharge hopper, which is connected to the downstream processing equipment. The clean air, now free of solid particles, is either recirculated back into the system to improve energy efficiency or released after filtration. The entire operation is monitored by a control panel that displays real-time data on pressure, flow rate, and material level. Operators can adjust parameters such as air pressure and flow rate to optimize performance based on the material characteristics and system load. This dynamic control ensures that the system operates efficiently under varying conditions, such as changes in material density or flow rate. The process is designed to be continuous, with minimal downtime for maintenance or cleaning, as the system can be operated with minimal intervention once properly set up.
Technical Advantages of Using a Pneumatic Conveying Line for Coal and Sand
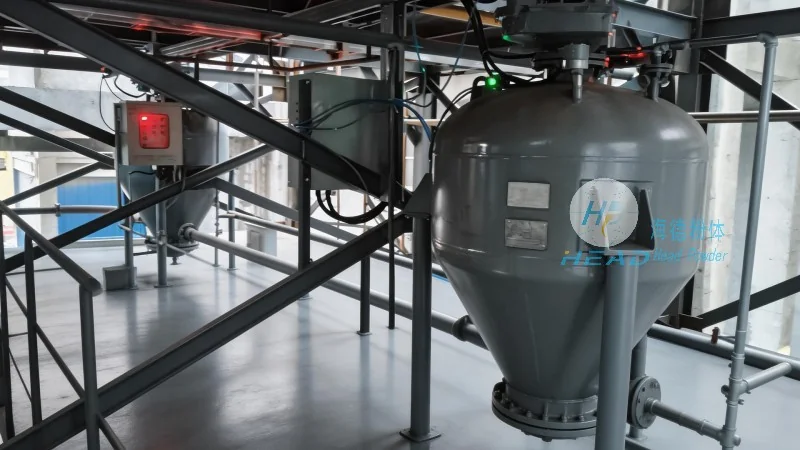
Implementing a pneumatic conveying line for coal and sand materials offers several technical advantages over traditional methods like belt conveyors or bucket elevators. One of the primary benefits is the ability to transport materials in a closed system, which significantly reduces dust emissions and improves workplace safety. This is particularly important for coal and sand, which can generate fine particles that are hazardous to health if inhaled. The closed system also prevents material contamination from external sources, ensuring that the product remains clean and free from impurities. Another advantage is the flexibility in system layout. Pneumatic conveying lines can be installed in various configurations, including vertical, horizontal, or a combination of both, to accommodate different site layouts and material handling requirements. This flexibility allows for efficient use of space and integration with existing infrastructure. Additionally, the system is relatively low maintenance compared to other bulk material handling equipment. The components, such as the rotary airlock valve and dust separator, are designed for durability and long service life, reducing the need for frequent repairs or replacements. The energy efficiency of the system is also a key advantage. By using a high-pressure air blower, the system can transport materials over longer distances with less energy consumption compared to other methods. The recirculation of air in the system further enhances energy efficiency, as it reduces the need to draw in fresh air from the environment. Finally, the system provides consistent and reliable material flow, which is critical for maintaining production efficiency in industries that rely on a steady supply of raw materials. The automated control system ensures that the flow rate and pressure are maintained at optimal levels, minimizing downtime and maximizing throughput.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer and supplier of pneumatic conveying systems and related engineering solutions. With a strong focus on innovation and quality, the company has established itself as a trusted partner for industries dealing with bulk materials. Headpowder specializes in designing and manufacturing customized pneumatic conveying lines tailored to the specific needs of clients, including those handling coal, sand, and other similar materials. The company's team of experienced engineers and technicians works closely with clients to understand their operational requirements and develop solutions that meet their unique challenges. Headpowder's products are known for their durability, efficiency, and reliability, ensuring that clients receive a high-quality system that delivers long-term performance. The company is committed to providing excellent customer service, from initial consultation and design to installation and after-sales support. Headpowder's headquarters is located in Shandong, China, where the company has a state-of-the-art manufacturing facility and a team of skilled professionals dedicated to delivering superior products and services. By choosing headpowder, clients can be confident that they are investing in a reliable and efficient solution for their material handling needs.




