HeadPowder, a leading manufacturer in the field, specializes in the design and production of corn starch pneumatic conveying systems. These systems are engineered to efficiently transport corn starch and related powders through an air-driven mechanism, ensuring high performance and reliability in industrial applications. The core principle of pneumatic conveying involves using compressed air to move bulk materials, which is particularly advantageous for handling fine powders like corn starch that are prone to dust and clogging in traditional mechanical systems.
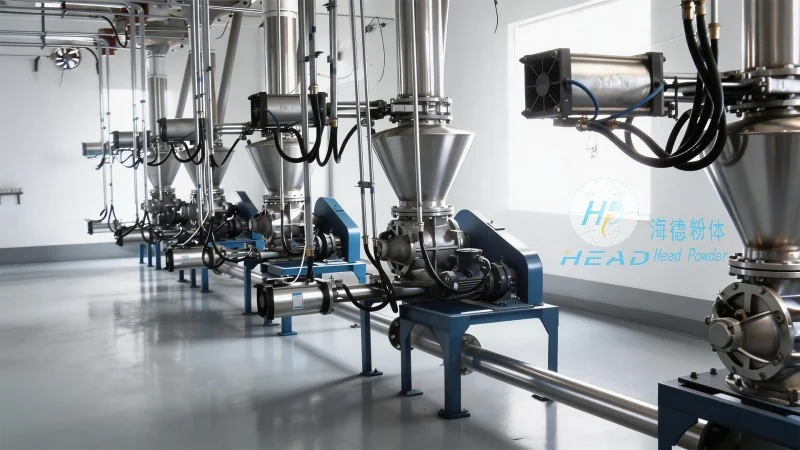
Working Principle of the Pneumatic Conveying System
The operation of a corn starch pneumatic conveying system is based on the fundamental physics of fluid dynamics and material transport. At its heart, the system comprises several key components: a feeding hopper, a conveying line (often equipped with airlocks or rotary valves), a dust collector, and a discharge outlet. The process begins when corn starch is fed into the hopper. Compressed air is then introduced into the system, creating a pressure differential that propels the starch particles through the conveying line. The air acts as a carrier, suspending the powder and moving it from the source to the destination. This method eliminates the need for mechanical components that might cause friction or contamination, making it ideal for food-grade applications where hygiene is paramount.
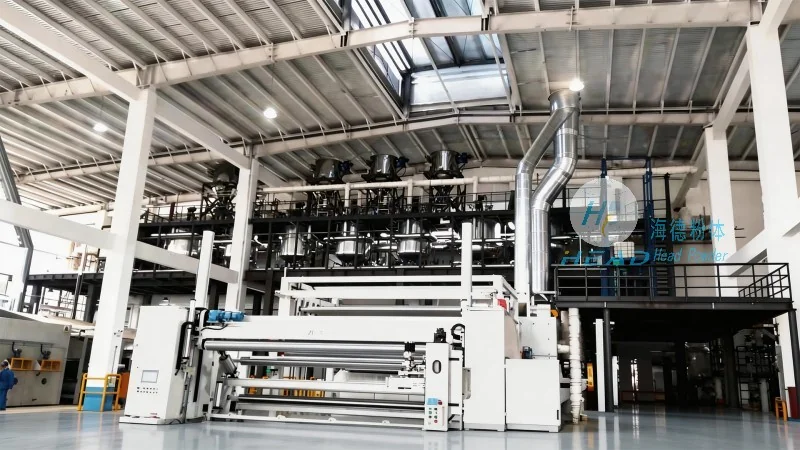
Key Working Scene Characteristics
The working scene characteristics of corn starch pneumatic conveying equipment are tailored to meet the specific demands of industrial environments. One of the primary advantages is the ability to handle fine, cohesive powders without the risk of blockages or degradation. The system's design minimizes product contact with metal surfaces, reducing the likelihood of contamination and ensuring product purity. Additionally, the equipment is highly scalable, allowing it to be adapted for both small-scale laboratory operations and large-scale industrial production lines. This flexibility makes it suitable for various applications, including starch processing plants, food manufacturing facilities, and chemical processing units where consistent and efficient material transport is critical.
Advantages in Practical Applications
In real-world scenarios, corn starch pneumatic conveying systems offer several distinct advantages over traditional methods. For instance, they provide a dust-free and enclosed transport process, which enhances workplace safety and complies with environmental regulations. The system's ability to maintain product integrity is another key benefit, as the enclosed environment prevents moisture absorption and oxidation, which can affect the quality of corn starch. Furthermore, the energy efficiency of pneumatic conveying systems is notable; by optimizing air pressure and flow rates, operators can reduce energy consumption while maintaining high throughput. This makes the equipment not only cost-effective but also environmentally friendly, aligning with modern industrial sustainability goals.
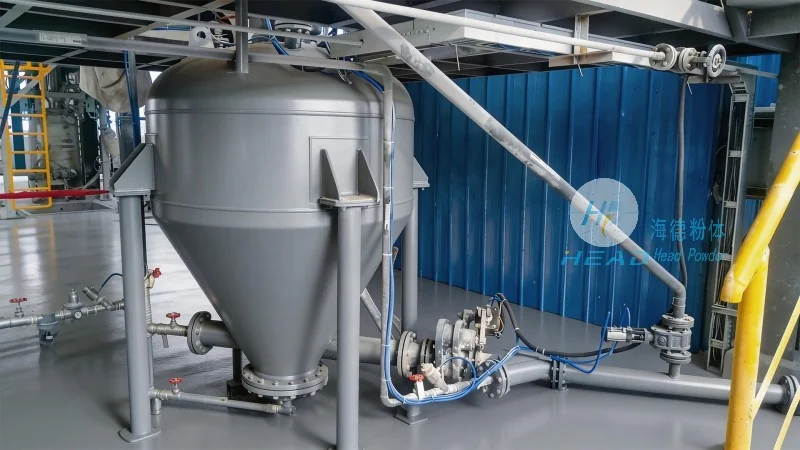
Company Profile and Technical Support
Shandong HeadPowder Engineering Co., Ltd., the parent company of HeadPowder, is headquartered in Shandong, China. With years of experience in the engineering and manufacturing of material handling systems, the company has established itself as a trusted partner for industries requiring reliable and efficient corn starch conveying solutions. HeadPowder's team of engineers and technicians specializes in customizing systems to meet specific client needs, ensuring that each installation is optimized for performance, safety, and longevity. The company provides comprehensive technical support, including installation guidance, maintenance services, and troubleshooting assistance, to ensure that clients can maximize the operational efficiency of their equipment. By leveraging advanced technology and adhering to strict quality standards, HeadPowder delivers solutions that meet the highest industry benchmarks.




