HeadPowder, a leading provider of industrial conveying solutions, specializes in the design and manufacturing of advanced corn cob pneumatic conveying equipment. This article explores the fundamental principles behind this technology and highlights key working scene characteristics that make it an efficient choice for various industrial applications.
Understanding the Pneumatic Conveying Principle
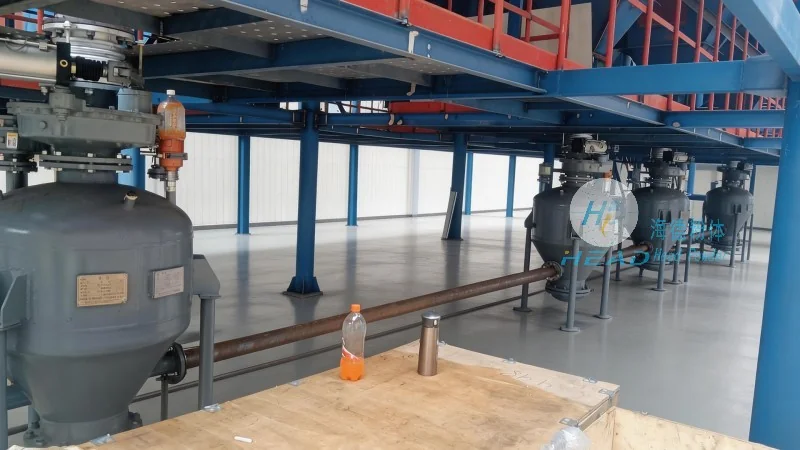
The core of corn cob pneumatic conveying equipment lies in the use of air as the medium to transport bulk materials. Unlike traditional mechanical conveyors, which rely on belts, chains, or screws, pneumatic systems utilize pressure differentials to move materials through a pipeline. In the case of corn cob, a dry, fibrous agricultural byproduct, the equipment is engineered to handle its unique physical properties, such as low bulk density and abrasive characteristics. The system typically consists of a hopper, a rotary valve or feeder, a conveying pipeline, and a receiver or discharge unit. Air is introduced into the system, often through a blower or fan, creating a flow that lifts and transports the corn cob particles. The design ensures minimal material degradation and efficient transfer, making it suitable for high-volume operations.
Key Working Scene Characteristics
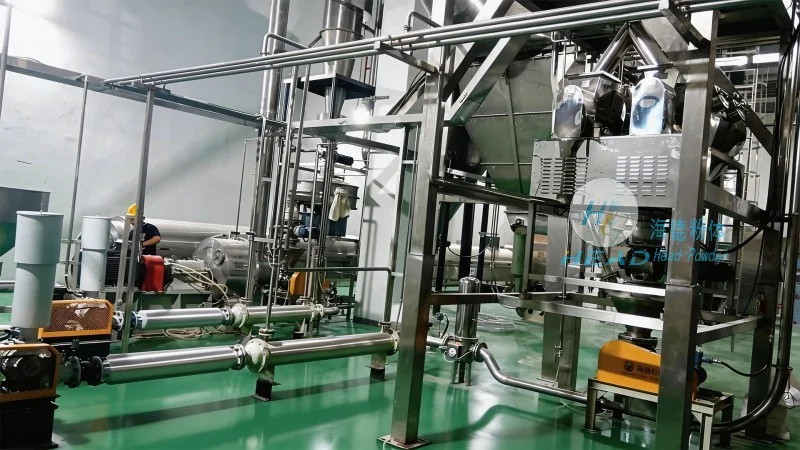
HeadPowder's corn cob pneumatic conveying equipment is tailored to meet the demands of diverse industrial environments. One of the primary advantages is its ability to handle long-distance transport with minimal maintenance. The equipment operates in a closed system, reducing dust emissions and improving workplace safety, which is crucial in facilities processing corn cob for animal feed or biomass energy production. Another notable characteristic is its adaptability to varying material conditions. Whether dealing with raw corn cob or processed fractions, the system can be adjusted to optimize flow rates and pressure levels, ensuring consistent performance. The working scenes often include feed mills, biofuel plants, and agricultural processing facilities, where the equipment integrates seamlessly with existing production lines. Additionally, the equipment's compact design allows for installation in spaces with limited room, making it a practical solution for both new and retrofit projects.
Application Scenarios and Efficiency
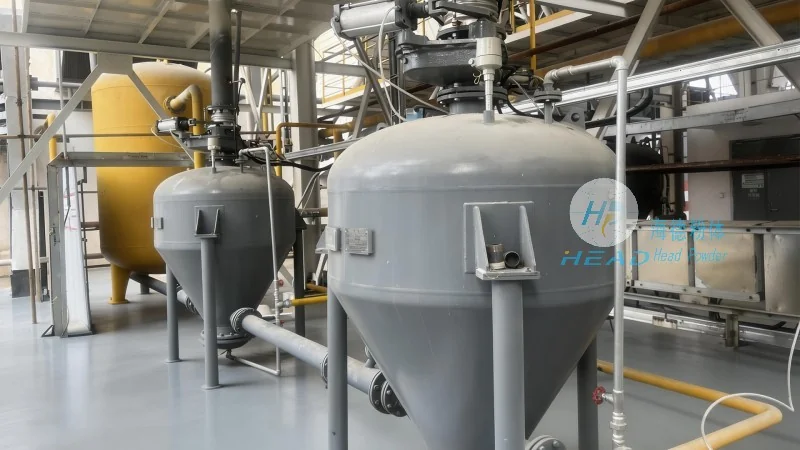
In real-world applications, corn cob pneumatic conveying systems from HeadPowder have demonstrated significant efficiency gains. For instance, in a feed mill, the equipment can transport corn cob from storage silos to processing units without the need for manual handling, reducing labor costs and operational downtime. Similarly, in a biofuel plant, the system efficiently moves biomass feedstock to the combustion or gasification stage, contributing to higher energy output. The working scene characteristics also include the ability to handle mixed materials, such as corn cob mixed with other byproducts, without clogging or loss of material. This versatility makes the equipment a valuable asset in industries where material consistency and throughput are critical. Furthermore, the system's energy efficiency is a key factor, as it minimizes power consumption compared to traditional conveyors, leading to lower operational costs over time.
Conclusion and Company Overview
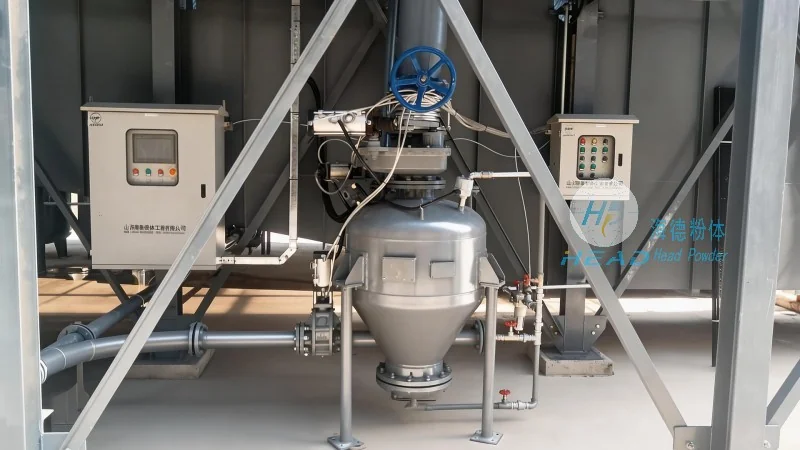
HeadPowder Engineering Co., Ltd., based in Shandong, China, has established itself as a trusted manufacturer of corn cob pneumatic conveying equipment. With a focus on innovation and customer-centric solutions, the company ensures that its products meet the specific needs of each working scene. By combining advanced engineering with practical application knowledge, HeadPowder delivers reliable, efficient, and cost-effective conveying systems that enhance productivity in agricultural and industrial settings. The principles and characteristics outlined above underscore the importance of selecting the right pneumatic conveying equipment for corn cob processing, and HeadPowder's expertise makes it a top choice for businesses seeking to optimize their operations.




