Working Principle and Features of Copper Mine Sand Powder Pneumatic Conveying Systems
Release time:2026-09-18 02:01:28
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Zhang manager
Copper mine sand powder pneumatic conveying systems represent a critical technology in the mineral processing industry, designed to efficiently transport fine particulate materials like copper mine sand from one location to another. These systems utilize air or gas as the primary conveying medium, offering a flexible and effective solution for handling bulk materials in mining operations. The following sections will explore the fundamental working principle and key features of such systems, with a focus on their application in copper mine sand processing.
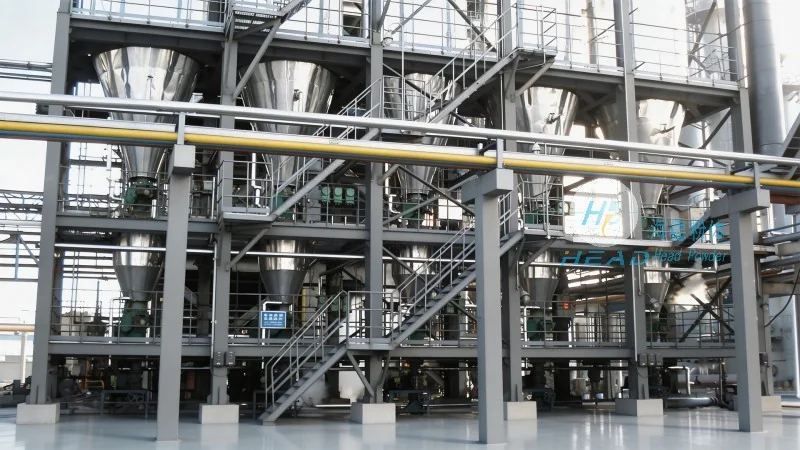
Working Principle of the Pneumatic Conveying System
The core working principle of a copper mine sand powder pneumatic conveying system revolves around the use of compressed air or other gases to generate the necessary force to move the material. The process typically begins with the material being fed into a hopper or feeder, where it is then introduced into a pipeline. As the air is introduced into the pipeline, it creates a low-pressure zone that draws the powder particles along with it. The combination of air velocity and particle size determines the conveying velocity and efficiency. The system may include components such as a blower or compressor to generate the required air pressure, a filter to remove any fine particles from the exhaust air, and a separator to separate the material from the air at the destination point. This continuous cycle allows for the seamless transport of copper mine sand powder over varying distances, often with minimal human intervention.
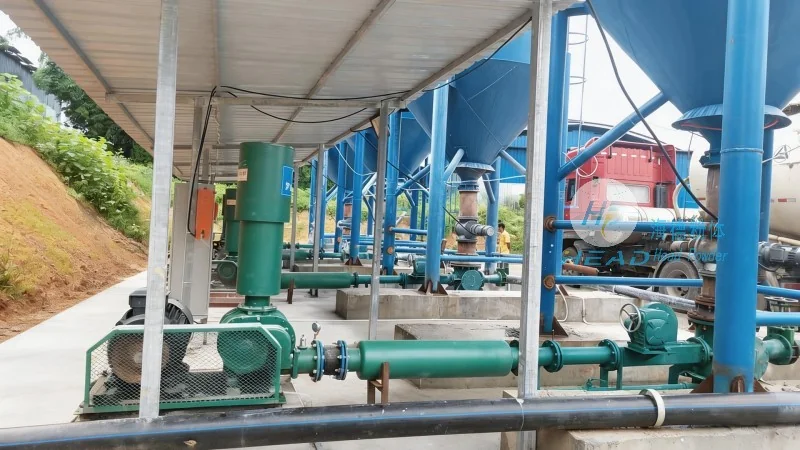
Key Features of the Copper Mine Sand Powder Pneumatic Conveying System
Several distinct features make copper mine sand powder pneumatic conveying systems particularly advantageous in mining applications. Firstly, they offer high efficiency in material transport, capable of moving large volumes of fine particulate material with minimal energy consumption compared to traditional methods like belt conveyors or trucks. The system's flexibility allows for the conveyance of materials over complex routes, including vertical and horizontal segments, without the need for extensive infrastructure modifications. Additionally, these systems are generally more hygienic and dust-free, reducing the risk of contamination and improving workplace safety. The enclosed design of the pipeline also minimizes environmental impact by preventing dust emissions into the air. Another notable feature is the ease of integration with other processing equipment, as the system can be easily connected to storage silos, processing units, or packaging machinery. Maintenance requirements are relatively low, with most components designed for durability and ease of repair, contributing to long-term operational reliability. The system's ability to handle abrasive materials like copper mine sand without significant wear on components further enhances its practicality in demanding mining environments.
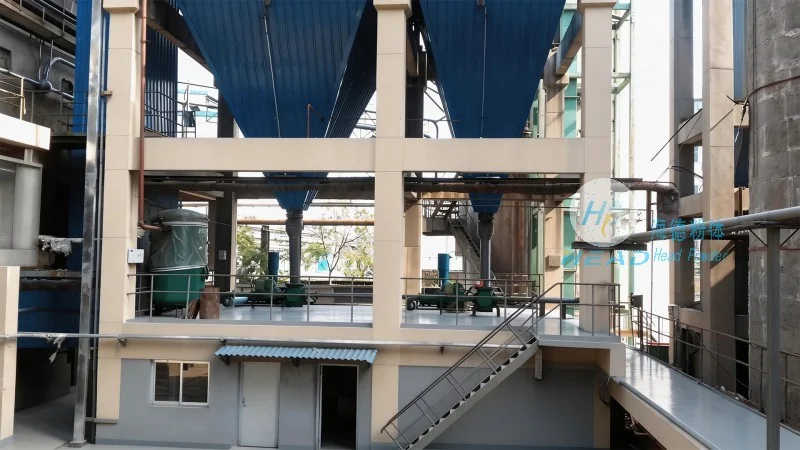
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer specializing in the design, development, and supply of advanced pneumatic conveying systems for various industrial applications, including mining and mineral processing. With a strong focus on innovation and customer-centric solutions, the company has established itself as a trusted partner in the industry. HeadPowder's headquarters and primary operations are located in Shandong, China, where the company leverages local expertise and resources to deliver high-quality products tailored to the specific needs of copper mine operations. The company's commitment to quality, safety, and environmental responsibility is reflected in its adherence to international standards and continuous improvement initiatives. By combining cutting-edge technology with extensive industry experience, HeadPowder provides reliable and efficient pneumatic conveying solutions that enhance operational efficiency and reduce costs for its clients in the copper mining sector.




