Working Principle and Features of Cement Granular Material Conveying Systems
Release time:2026-09-17 19:01:25
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Zhang manager
Cement production and construction industries rely heavily on efficient material handling solutions to ensure smooth operations and high productivity. The cement granular material conveying system, a critical component in these sectors, plays a pivotal role in transporting bulk materials like cement, fly ash, and other powders. This article delves into the working principle and key features of such systems, highlighting how they enhance operational efficiency and reliability.
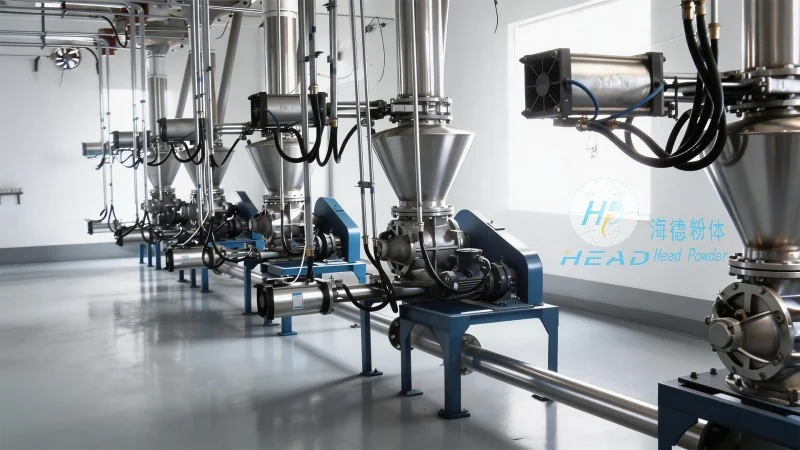
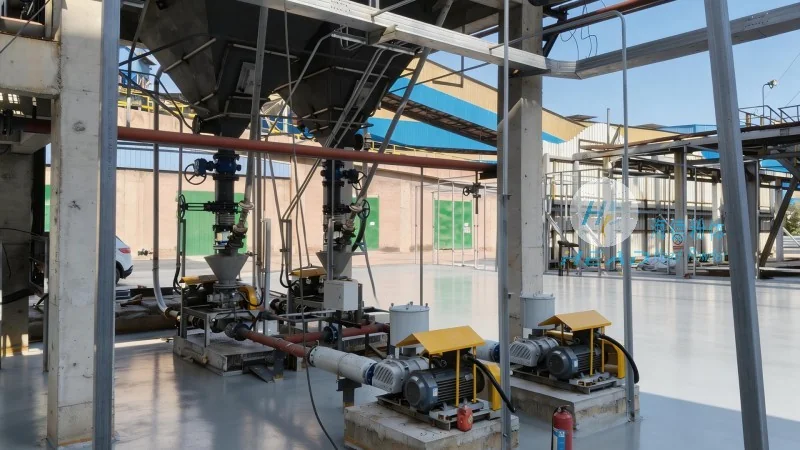
Working Principle of Cement Granular Material Conveying Systems
The working principle of a cement granular material conveying system is centered around the use of specialized equipment designed to move bulk materials over long distances or vertical heights. Typically, these systems employ mechanisms like screw conveyors, pneumatic conveying systems, or belt conveyors, each tailored to specific material characteristics and operational requirements. For instance, screw conveyors utilize rotating screws to push materials forward, while pneumatic systems use air pressure to transport particles through pipelines. The system's design ensures minimal material degradation and consistent flow rates, which are crucial for maintaining product quality and reducing downtime. Additionally, modern systems incorporate sensors and control systems to monitor and adjust the conveying process in real-time, further optimizing performance and preventing potential issues.
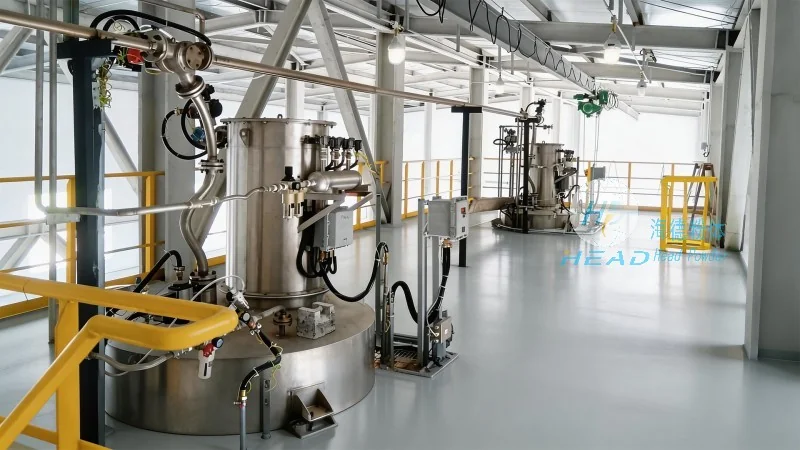
Key Features of Cement Granular Material Conveying Systems
Key features of cement granular material conveying systems include high efficiency, low maintenance costs, and adaptability to various material types. These systems are engineered to handle abrasive and fine materials without causing wear or blockages, thanks to robust construction and advanced materials. For example, the use of stainless steel or special coatings in conveyor components enhances durability and resistance to corrosion. Furthermore, the systems offer flexibility in terms of layout, allowing integration into existing production lines or new facility setups. This adaptability is particularly valuable in dynamic industrial environments where processes may evolve over time. Another notable feature is their energy efficiency, which reduces operational costs and aligns with sustainability goals in the industry. By minimizing energy consumption, these systems contribute to lower carbon footprints and cost savings for businesses.
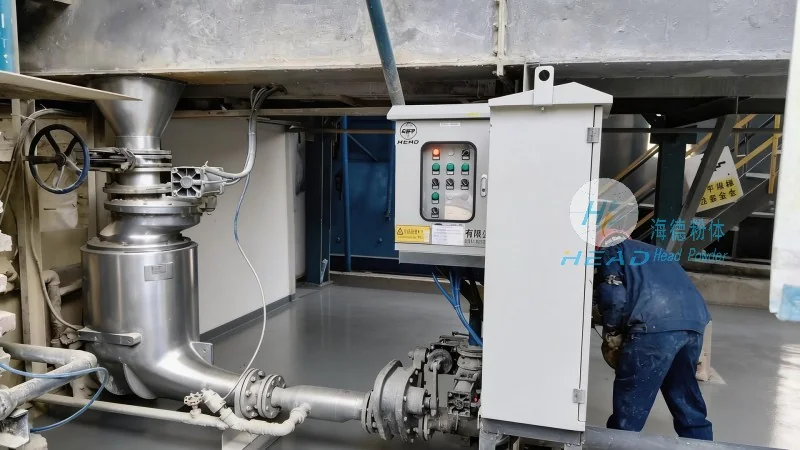
Shandong HeadPowder Engineering Co., Ltd., a leading provider in the field, specializes in designing and manufacturing advanced cement granular material conveying systems. With a focus on innovation and customer-centric solutions, the company ensures that its products meet the highest standards of performance and reliability. HeadPowder's systems are widely used in cement plants, power stations, and construction sites across China, demonstrating their effectiveness in real-world applications. The company's commitment to quality and customer satisfaction has established it as a trusted partner for businesses seeking reliable material handling solutions.




