

Working Principle and Features of Organic Salt Powder Conveyors
Organic salt powder conveyors are essential equipment in the chemical and industrial sectors, designed to efficiently transport organic salt powders from one location to another. These systems are engineered to handle various types of organic salts, including but not limited to sodium chloride, potassium chloride, and other similar compounds, ensuring reliable and safe material handling. The following sections will explore the working principle and key features of such conveyors, providing a comprehensive understanding of their functionality and benefits.
Company Introduction
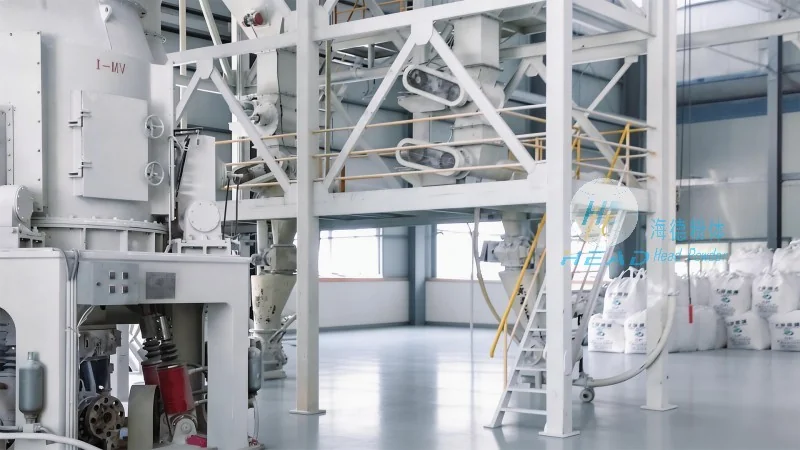
HeadPowder, as the manufacturer, is a leading provider of specialized powder handling equipment. With its headquarters in Shandong, China, the company has established itself as a trusted name in the industry, delivering high-quality solutions tailored to the unique needs of clients. The company's commitment to innovation and quality ensures that each organic salt powder conveyor is built to meet stringent operational requirements and safety standards.
Working Principle of Organic Salt Powder Conveyors
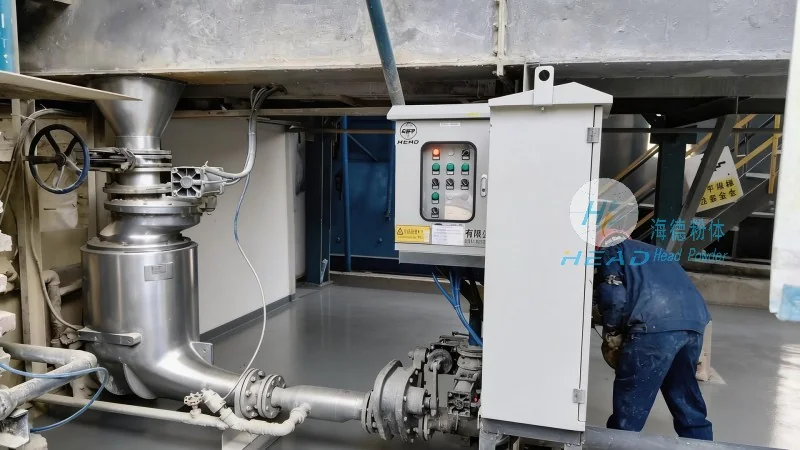
The working principle of organic salt powder conveyors revolves around the use of mechanical components to move powders through a system. Typically, these conveyors employ a combination of screw mechanisms, belt systems, or pneumatic methods to transport the material. The screw conveyor, for instance, consists of a rotating helical screw inside a trough, which pulls the powder forward as it rotates. This mechanism is particularly effective for organic salts due to its ability to handle dry, free-flowing powders without the need for additional additives or lubricants. The conveyor's design ensures minimal product degradation and maintains the integrity of the organic salt, which is crucial for applications where purity and consistency are paramount.
Key Features of Organic Salt Powder Conveyors
Organic salt powder conveyors are equipped with several features that enhance their performance and usability. One of the primary features is the adjustable speed control, allowing operators to regulate the conveyor's speed based on the specific requirements of the material being transported. This flexibility ensures optimal flow rates and prevents issues such as clogging or excessive pressure buildup. Another important feature is the material's ability to handle varying particle sizes and moisture content. The conveyor's design incorporates robust construction materials, such as stainless steel or corrosion-resistant alloys, which are ideal for organic salts that may be prone to moisture absorption or chemical reactions. Additionally, the system includes safety features like overload protection and emergency stop mechanisms, ensuring safe operation in industrial environments.
Advantages of Using Organic Salt Powder Conveyors
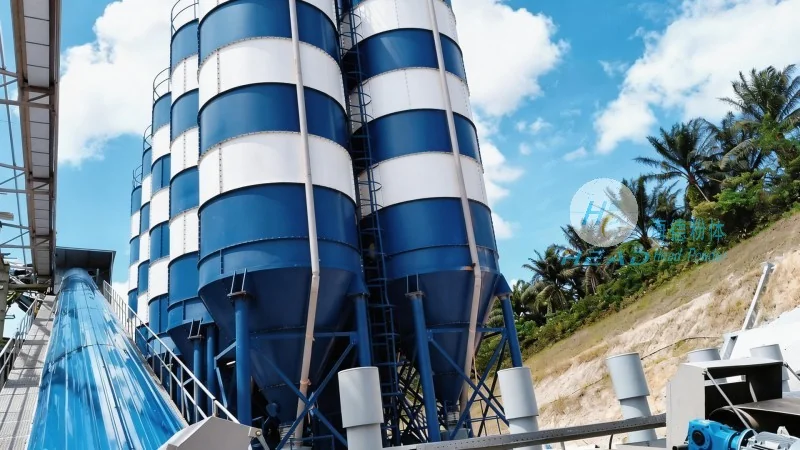
Implementing organic salt powder conveyors offers several advantages for industrial operations. Firstly, these systems improve operational efficiency by automating the material handling process, reducing the need for manual labor and minimizing the risk of human error. The consistent and reliable transport of organic salts ensures that production lines run smoothly, leading to increased productivity and reduced downtime. Secondly, the conveyors contribute to cost savings by minimizing material waste and reducing the need for additional processing steps. The efficient transfer of powders also helps in maintaining product quality, as the system prevents contamination and degradation that can occur during manual handling. Furthermore, the compact design of many organic salt powder conveyors allows for easy integration into existing production facilities, making them a practical solution for businesses looking to upgrade their material handling capabilities.
Applications in Industrial Settings
Organic salt powder conveyors find wide applications in various industrial sectors. In the chemical industry, they are used to transport raw materials such as sodium chloride and potassium chloride to production lines, where they are further processed into other chemical products. The food industry also utilizes these conveyors for handling organic salts used as preservatives or flavor enhancers in food processing. Additionally, in the pharmaceutical industry, the conveyors are employed to transport organic salts used in the formulation of medications, ensuring that the materials are handled hygienically and safely. The versatility of these systems makes them suitable for a range of applications, from small-scale operations to large-scale industrial plants.