HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced vacuum suction type powder handling equipment. This equipment is engineered to efficiently transport bulk powders and granules in various industrial applications, offering a reliable solution for material handling challenges. The following sections will delve into the working principle and key features of this technology.
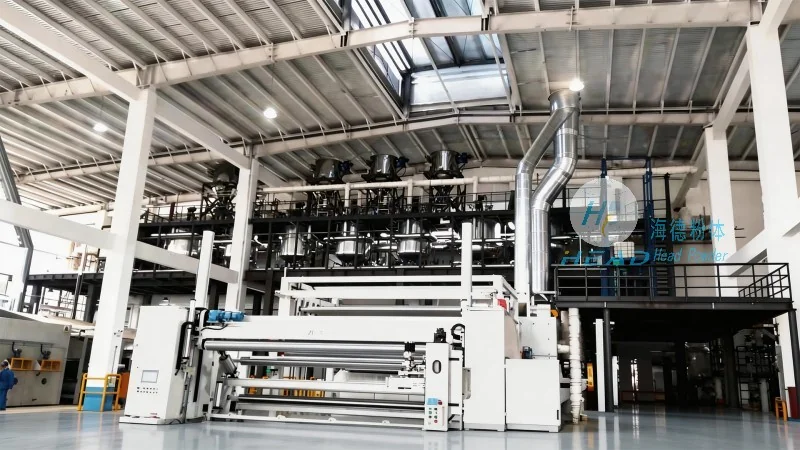
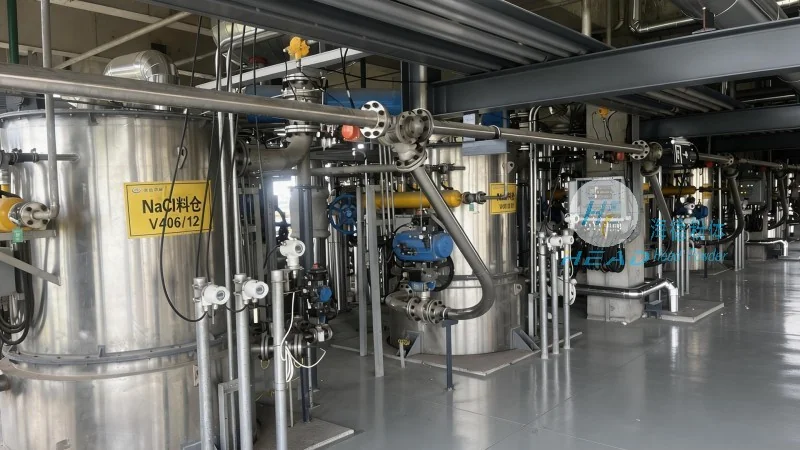
Working Principle of Vacuum Suction Type Powder Handling Equipment
The vacuum suction system operates on the principle of creating a pressure differential between the material source and the collection point. By generating a negative pressure (vacuum) at the intake, the equipment draws powders into the system. The process typically involves a series of components, including a vacuum pump, a hopper for material loading, and a pipeline network. The vacuum pump maintains the low-pressure environment, while the hopper allows for easy loading of the powder. As the material is drawn into the pipeline, it is transported to the destination, where the pressure is restored to atmospheric levels, allowing the powder to be discharged. This method eliminates the need for mechanical conveying elements like belts or screws, reducing wear and maintenance costs. The system is particularly effective for handling fine powders and sensitive materials that are prone to degradation or contamination from mechanical contact.
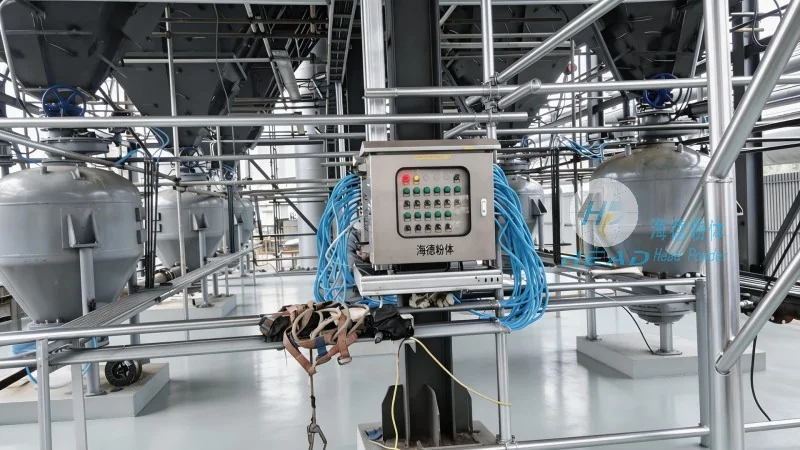
Key Features of Vacuum Suction Type Powder Handling Equipment
HeadPowder's vacuum suction type powder handling equipment is characterized by several distinct features that enhance its performance and usability. One of the primary advantages is the ability to handle a wide range of powder types, from fine powders to larger granules, without the risk of clogging or blockage. The system's flexibility allows for variable flow rates, enabling precise control over the material transport. Additionally, the vacuum design minimizes the risk of dust emissions, contributing to a cleaner and safer working environment. The equipment is also designed for easy integration into existing production lines, with modular components that can be customized to meet specific application requirements. Another notable feature is the low energy consumption, as the vacuum pump operates efficiently and requires minimal power compared to traditional conveying methods. The system's durability and robust construction ensure long-term reliability, with minimal downtime for maintenance. Furthermore, the equipment is equipped with safety features, such as pressure relief valves and overcurrent protection, to ensure safe operation in industrial settings.
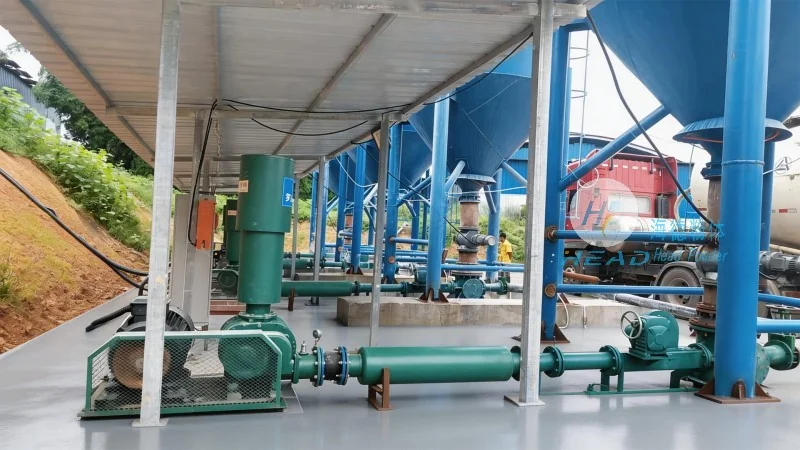
Applications and Benefits
Vacuum suction type powder handling equipment from HeadPowder is widely used in various industries, including pharmaceuticals, food processing, chemical manufacturing, and mining. The system's ability to handle sensitive materials makes it ideal for applications where product purity and quality are critical. In the pharmaceutical industry, for example, the equipment is used to transport active pharmaceutical ingredients (APIs) and excipients, ensuring that the materials remain uncontaminated and free from mechanical damage. In the food industry, the system is employed to handle powders like flour, sugar, and spices, maintaining the product's quality and preventing cross-contamination. The chemical industry benefits from the equipment's ability to handle corrosive or hazardous powders, as the system is designed with materials that resist chemical attack. The mining industry uses the equipment to transport bulk materials like ore and coal, improving efficiency and reducing labor costs. The overall benefits of this technology include increased productivity, reduced operational costs, and improved product quality. The vacuum suction system also contributes to a safer working environment by minimizing dust exposure and reducing the risk of accidents associated with mechanical conveying systems.




